Каталог ZCC-CT сверла монолитные - страница 100
Навигация
 Каталог ZCC-CT сверла со сменными пластинами
 Общий каталог ZCC-CT 2019
 Каталог ZCC-CT расточные системы
 Каталог ZCC-CT фрезы монолитные
 Каталог ZCC-CT фрезы со сменными пластинами
 Каталог ZCC-CT оснастка
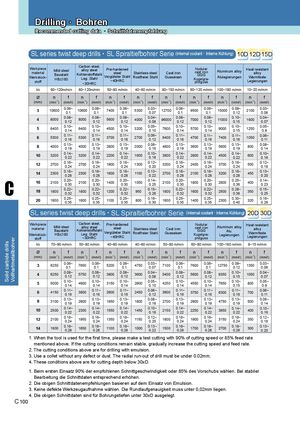
| SL ser | ies t | wist d | eep | drills∙ | SL | Spiral | tiefbo | hrer | Serie | (Interna | l coolan | t ∙ Intern | e Kühlun | ) 10 g | 12 D | D 15D |
| Workpiece material Werkstück- stoff | Mild HB≤ Bau | steel 180 stahl | Carbo alloy ~30 Kohlens Leg. | n steel, steel HRC toffstahl Stahl | Pre-ha st ~40 Vergüte | rdened eel HRC ter Stahl | Stainle Rostfrei | ss steel er Stahl | Cast Guss | iron eisen | Nod cast G Kuge phit | ular iron GG lgra- guss | Aluminu Alulegie | m alloy rungen | Heat re all Warm Legier | sistant oy feste ungen |
| Vc | 60~12 | 0m/min | 60~12 | 0m/min | 50~80 | m/min | 40~60 | m/min | 80~150 | m/min | 60~120 | m/min | 100~18 | 0 m/min | 10~20 | m/min |
| Ø | n | f | n | f | n | f | n | f | n | f | n | f | n | f | n | f |
| (mm) | (min -1) | (mm/r) | (min -1) | (mm/r) | (min -1) | (mm/r) | (min -1) | (mm/r) | (min -1) | (mm/r) | (min -1) | (mm/r) | (min -1) | (mm/r) | (min -1) | (mm/r) |
| 3 | 10600 | 0.06~ 0.1 | 10600 | 0.06~ 0.1 | 7400 | 0.06~ 0.1 | 5300 | 0.03~ 0.07 | 12700 | 0.06~ 0.1 | 9500 | 0.06~ 0.1 | 15000 | 0.09~ 0.12 | 2100 | 0.03~ 0.06 |
| 4 | 8000 | 0.08~ 0.12 | 8000 | 0.08~ 0.12 | 5600 | 0.08~ 0.12 | 4000 | 0.04~ 0.08 | 96000 | 0.08~ 0.12 | 7000 | 0.08~ 0.12 | 11000 | 0.10~ 0.15 | 1600 | 0.04~ 0.07 |
| 5 | 6400 | 0.10~ 0.14 | 6400 | 0.10~ 0.14 | 4500 | 0.10~ 0.14 | 3200 | 0.05~ 0.10 | 7600 | 0.10~ 0.14 | 5700 | 0.10~ 0.14 | 9000 | 0.10~ 0.15 | 1250 | 0.05~ 0.9 |
| 6 | 5300 | 0.11~ 0.16 | 5300 | 0.11~ 0.16 | 3700 | 0.11~ 0.16 | 2700 | 0.06~ 0.12 | 6400 | 0.11~ 0.16 | 4700 | 0.11~ 0.16 | 7400 | 0.11~ 0.16 | 1050 | 0.06~ 0.11 |
| 8 | 4000 | 0.13~ 0.19 | 4000 | 0.13~ 0.19 | 2800 | 0.13~ 0.19 | 2000 | 0.08~ 0.16 | 4800 | 0.13~ 0.19 | 3600 | 0.13~ 0.19 | 5600 | 0.13~ 0.19 | 800 | 0.08~ 0.14 |
| 10 | 3200 | 0.14~ 0.22 | 3200 | 0.14~ 0.22 | 2200 | 0.14~ 0.22 | 1600 | 0.10~ 0.18 | 3800 | 0.14~ 0.22 | 2800 | 0.14~ 0.22 | 4500 | 0.14~ 0.22 | 600 | 0.10~ 0.16 |
| 12 | 2700 | 0.16~ 0.24 | 2700 | 0.16~ 0.24 | 1900 | 0.16~ 0.24 | 1300 | 0.12~ 0.20 | 3200 | 0.16~ 0.24 | 2400 | 0.16~ 0.24 | 3700 | 0.16~ 0.24 | 500 | 0.12~ 0.18 |
| 14 | 2300 | 0.18~ 0.28 | 2300 | 0.18~ 0.28 | 1600 | 0.18~ 0.28 | 1100 | 0.13~ 0.22 | 2700 | 0.18~ 0.28 | 2100 | 0.18~ 0.28 | 3200 | 0.18~ 0.28 | 450 | 0.13~ 0.20 |
| 16 | 2100 | 0.20~ 0.30 | 2100 | 0.20~ 0.30 | 1400 | 0.20~ 0.30 | 1050 | 0.14~ 0.25 | 2100 | 0.20~ 0.30 | 1800 | 0.20~ 0.30 | 2800 | 0.25~ 0.36 | 400 | 0.14~ 0.23 |
| 18 | 1800 | 0.22~ 0.32 | 1800 | 0.22~ 0.32 | 1200 | 0.22~ 0.32 | 950 | 0.15~ 0.28 | 1800 | 0.22~ 0.32 | 1600 | 0.22~ 0.32 | 2500 | 0.28~ 0.38 | 350 | 0.15~ 0.25 |
| 20 | 1600 | 0.25~ 0.35 | 1600 | 0.25~ 0.35 | 1100 | 0.25~ 0.35 | 800 | 0.16~ 0.30 | 1600 | 0.25~ 0.35 | 1400 | 0.25~ 0.35 | 2300 | 0.30~ 0.40 | 320 | 0.16~ 0.28 |
SL series twist deep drills SL Spiraltiefbohrer Serie ∙ Interne Kühlung(Internal coolant ∙ ) 20D 30D
| Workpiece material Werkstück- stoff | Mild HB≤ Bau | steel 180 stahl | Carbon alloy ~30 Kohlens Leg. | steel, steel HRC toffstahl Stahl | Pre-ha ste ~40 Vergütet | rdened el HRC er Stahl | Stainle Rostfrei | ss steel er Stahl | Cast Guss | iron eisen | Nod cast G Kuge phit | ular iron GG lgra- guss | Aluminu Al Legier | m alloy u. ungen | Heat re all Warm Legier | sistant oy feste ungen |
| Vc | 70~90 | m/min | 50~80 | m/min | 40~60 | m/min | 40~60 | m/min | 50~80 | m/min | 60~80 | m/min | 100~18 | 0 m/min | 8~15 | m/min |
| Ø | n | f | n | f | n | f | n | f | n | f | n | f | n | f | n | f |
| (mm) | (min -1) | (mm/r) | (min -1) | (mm/r) | (min -1) | (mm/r) | (min -1) | (mm/r) | (min -1) | (mm/r) | (min -1) | (mm/r) | (min -1) | (mm/r) | (min -1) | (mm/r) |
| 3 | 8250 | 0.06~ 0.1 | 7650 | 0.06~ 0.1 | 5200 | 0.06~ 0.1 | 4750 | 0.03~ 0.07 | 7100 | 0.06~ 0.1 | 7600 | 0.06~ 0.1 | 12750 | 0.09~ 0.12 | 1350 | 0.03~ 0.06 |
| 4 | 6250 | 0.08~ 0.12 | 5750 | 0.08~ 0.12 | 3900 | 0.08~ 0.12 | 3600 | 0.04~ 0.08 | 5400 | 0.08~ 0.12 | 5600 | 0.08~ 0.12 | 9350 | 0.10~ 0.15 | 1050 | 0.04~ 0.07 |
| 5 | 5000 | 0.10~ 0.14 | 4600 | 0.10~ 0.14 | 3150 | 0.10~ 0.14 | 2900 | 0.05~ 0.10 | 4250 | 0.10~ 0.14 | 4550 | 0.10~ 0.14 | 7650 | 0.10~ 0.15 | 800 | 0.05~ 0.9 |
| 6 | 4150 | 0.11~ 0.16 | 3800 | 0.11~ 0.16 | 2600 | 0.11~ 0.16 | 2450 | 0.06~ 0.12 | 3600 | 0.11~ 0.16 | 3750 | 0.11~ 0.16 | 6300 | 0.11~ 0.16 | 700 | 0.06~ 0.11 |
| 8 | 3100 | 0.13~ 0.19 | 2900 | 0.13~ 0.19 | 1950 | 0.13~ 0.19 | 1800 | 0.08~ 0.16 | 2700 | 0.13~ 0.19 | 2900 | 0.13~ 0.19 | 4750 | 0.13~ 0.19 | 500 | 0.08~ 0.14 |
| 10 | 2500 | 0.14~ 0.22 | 2300 | 0.14~ 0.22 | 1550 | 0.14~ 0.22 | 1450 | 0.10~ 0.18 | 2150 | 0.14~ 0.22 | 2250 | 0.14~ 0.22 | 3850 | 0.14~ 0.22 | 400 | 0.10~ 0.16 |
| 12 | 2100 | 0.16~ 0.24 | 1950 | 0.16~ 0.24 | 1350 | 0.16~ 0.24 | 1150 | 0.12~ 0.20 | 1800 | 0.16~ 0.24 | 1900 | 0.16~ 0.24 | 3150 | 0.16~ 0.24 | 350 | 0.12~ 0.18 |
| 14 | 1800 | 0.18~ 0.28 | 1650 | 0.18~ 0.28 | 1100 | 0.18~ 0.28 | 1000 | 0.13~ 0.22 | 1500 | 0.18~ 0.28 | 1700 | 0.18~ 0.28 | 2700 | 0.18~ 0.28 | 300 | 0.13~ 0.20 |
1. When the tool is used for the first time, please make a test cutting with 90% of cutting speed or 85% feed rate
mentioned above. If the cutting conditions remain stable, gradually increase the cutting speed and feed rate. 2. The cutting conditions above are for drilling with emulsion. 3. Use a collet without any defect or dust. The radial run-out of drill must be under 0.02mm. 4. These conditions above are for cutting depth below 30xD.
1. Beim ersten Einsatz 90% der empfohlenen Schnittgeschwindigkeit oder 85% des Vorschubs wählen. Bei stabiler
Bearbeitung die Schnittdaten entsprechend erhöhen. 2. Die obigen Schnittdatenempfehlungen basieren auf dem Einsatz von Emulsion. 3. Keine defekte Werkzeugaufnahme wählen. Die Rundlaufgenauigkeit muss unter 0,02mm liegen. 4. Die obigen Schnittdaten sind für Bohrungstiefen unter 30xD ausgelegt.