Каталог ZCC-CT фрезы монолитные - страница 142
Навигация
 Каталог ZCC-CT оснастка
 Каталог ZCC-CT фрезы со сменными пластинами
 Каталог ZCC-CT сверла со сменными пластинами
 Каталог ZCC-CT токарная обработка
 Каталог ZCC-CT сверла монолитные
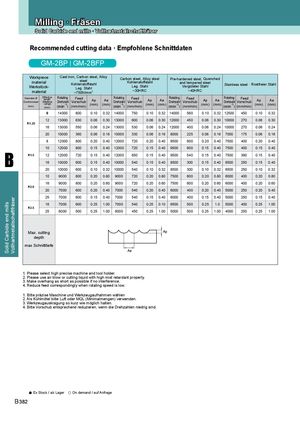
Recommended cutting data · Empfohlene Schnittdaten
GM-2BP | GM-2BFP
| Work mat Werks mat | piece erial Effective tück- erial | Cast ir Rotating | on,Carbon steel ~750N/m Kohlenstof Leg. St | steel, m 2 fstahl ahl | Alloy | Car Rotating | bon steel, ~30HR Kohlensto Leg. St | Alloy ste C ffstahl ahl | el | Pre-ha a Rotating | rdened ste nd temper ~40HR Vergüteter | el,Quen ed steel C Stahl | ched | Stainle Rotating | ss steel · R | ostfreie | r Stahl |
| Diameter Ø Durchmesser | length Effektive Lä | Drehzahl | Feed Vorschub | Ap | Ae | Drehzahl | Feed Vorschub | Ap | Ae | Drehzahl | Feed Vorschub | Ap | Ae | Drehzahl | Feed Vorschub | Ap | Ae |
| (mm) | (mm) nge | (min-1) | (mm/min) | (mm) | (mm) | (min-1) | (mm/min) | (mm) | (mm) | (min-1) | (mm/min) | (mm) | (mm) | (min-1) | (mm/min) | (mm) | (mm) |
| 8 | 14000 | 800 | 0.10 | 0.32 | 14000 | 750 | 0.10 | 0.32 | 14000 | 560 | 0.10 | 0.32 | 12500 | 450 | 0.10 | 0.32 | |
| 12 | 12 | 13000 | 630 | 0.06 | 0.30 | 13000 | 600 | 0.06 | 0.30 | 12000 | 450 | 0.06 | 0.30 | 10000 | 270 | 0.06 | 0.30 |
| R.5 | 16 | 13000 | 550 | 0.06 | 0.24 | 13000 | 530 | 0.06 | 0.24 | 12000 | 400 | 0.06 | 0.24 | 10000 | 270 | 0.06 | 0.24 |
| 20 | 10000 | 360 | 0.06 | 0.16 | 10000 | 330 | 0.06 | 0.16 | 8000 | 225 | 0.06 | 0.16 | 7000 | 175 | 0.06 | 0.16 | |
| 8 | 12000 | 800 | 0.20 | 0.40 | 12000 | 720 | 0.20 | 0.40 | 9500 | 600 | 0.20 | 0.40 | 7500 | 400 | 0.20 | 0.40 | |
| 10 | 12000 | 800 | 0.15 | 0.40 | 12000 | 720 | 0.15 | 0.40 | 9500 | 600 | 0.15 | 0.40 | 7500 | 400 | 0.15 | 0.40 | |
| R1.5 | 12 | 12000 | 720 | 0.15 | 0.40 | 12000 | 650 | 0.15 | 0.40 | 9500 | 540 | 0.15 | 0.40 | 7500 | 360 | 0.15 | 0.40 |
| 16 | 10000 | 600 | 0.15 | 0.40 | 10000 | 540 | 0.15 | 0.40 | 8500 | 300 | 0.15 | 0.40 | 6500 | 250 | 0.15 | 0.40 | |
| 20 | 10000 | 600 | 0.10 | 0.32 | 10000 | 540 | 0.10 | 0.32 | 8500 | 300 | 0.10 | 0.32 | 6500 | 250 | 0.10 | 0.32 | |
| 10 | 9000 | 800 | 0.20 | 0.80 | 9000 | 720 | 0.20 | 0.80 | 7500 | 600 | 0.20 | 0.80 | 6000 | 400 | 0.20 | 0.80 | |
| R20 | 16 | 9000 | 800 | 0.20 | 0.60 | 9000 | 720 | 0.20 | 0.60 | 7500 | 600 | 0.20 | 0.60 | 6000 | 400 | 0.20 | 0.60 |
| . | 20 | 7000 | 600 | 0.20 | 0.40 | 7000 | 540 | 0.20 | 0.40 | 6000 | 400 | 0.20 | 0.40 | 5000 | 250 | 0.20 | 0.40 |
| 25 | 7000 | 600 | 0.15 | 0.40 | 7000 | 540 | 0.15 | 0.40 | 6000 | 400 | 0.15 | 0.40 | 5000 | 250 | 0.15 | 0.40 | |
| R25 | 16 | 7000 | 600 | 0.25 | 1.00 | 7000 | 540 | 0.25 | 0.10 | 6500 | 500 | 0.25 | 1.0 | 5000 | 400 | 0.25 | 1.00 |
| . | 25 | 6000 | 500 | 0.25 | 1.00 | 6000 | 450 | 0.25 | 1.00 | 5000 | 500 | 0.25 | 1.00 | 4000 | 250 | 0.25 | 1.00 |
| Max. c de | utting pth | Ap | |||||||||||||||
| max Sch | nitttiefe | Ae |
1. Please select high precise machine and tool holder. 2. Please use air blow or cutting liquid with high mist retardant property. 3. Make overhang as short as possible if no interference. 4. Reduce feed correspondingly when rotating speed is low. 1. Bitte präzise Maschine und Werkzeugaufnahmen wählen 2. Als Kühlmittel bitte Luft oder MQL (Minimalmengen) verwenden. 3. Werkzeugauskragung so kurz wie möglich halten. 4. Bitte Vorschub entsprechend reduzieren, wenn die Drehzahlen niedrig sind.