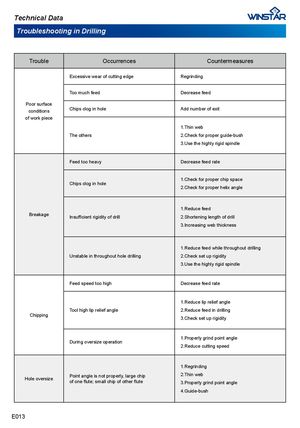
| Trouble | Occurrences | Countermeasures |
| Excessive wear of cutting edge | Regrinding |
| Too much feed | Decrease feed |
| Poor surface conditions of work iece | Chips clog in hole | Add number of exit |
| p | The others | 1.Thin web 2.Check for proper guide-bush 3.Use the highly rigid spindle |
| Feed too heavy | Decrease feed rate |
| Chips clog in hole | 1.Check for proper chip space 2.Check for proper helix angle |
| Breakage | Insufficient rigidity of drill | 1.Reduce feed 2.Shortening length of drill 3.Increasing web thickness |
| Unstable in throughout hole drilling | 1.Reduce feed while throughout drilling 2.Check set up rigidity 3.Use the highly rigid spindle |
| Feed speed too high | Decrease feed rate |
| Chipping | Tool high lip relief angle | 1.Reduce lip relief angle 2.Reduce feed in drilling 3.Check set up rigidity |
| During oversize operation | 1.Properly grind point angle 2.Reduce cutting speed |
| Hole oversize | Point angle is not properly, large chip of one flute; small chip of other flute | 1.Regrinding 2.Thin web 3.Properly grind point angle 4.Guide-bush |
 Каталог Carbidex сменные пластины 2020
 Каталог Winstar твердосплавные пластины и вставки
 Брошюра Winstar пластины 2021
 Каталог Winstar монолитный инструмент 2020
 Каталог Winstar инструмент со сменными пластинами 2020