Общий каталог Widia 2017 - страница 713
Навигация
 Каталог Widia токарный инструмент 2017
 Каталог Widia трохоидальное фрезерование
 Каталог Widia техническое руководство по разверткам
 Каталог Widia фрезы со сменными пластинами 2016
 Каталог Widia достижения 2020
- Table of Contents
- Turning
- Turning • ISO Inserts
- Turning • Tools for External Turning and Internal Boring
- Turning • Tools for External Turning and Internal Boring
- Turning • Tools for Small Hole Boring
- com E1Turning • Grooving and Cut-Off
- Turning • Threading
- Indexable Milling
- Indexable Milling • Face Mills
- Indexable Milling • Chamfer Mills
- Indexable Milling • 90° Shoulder Mills
- Indexable Milling • Helical Mills
- Indexable Milling • Slotting Mills
- Indexable Milling • Copy Mills
- Solid End Milling
- Solid End Milling • High-Performance Solid Carbide End Mills
- Solid End Milling • General Purpose Solid Carbide End Mills
- Solid End Milling • High-Performance High-Speed Steel (HSS-E/PM)
- Solid End Milling • Burs
- Holemaking
- Holemaking • High-Performance Solid Carbide Drills
- Holemaking • Modular Drills
- Holemaking • Indexable Drills
- Holemaking • Modular Drills
- Holemaking • Indexable Drills
- Holemaking • Hole Finishing
- Tapping
- Tapping Portfolio
- Index by Order Number
- Index by Catalogue Number
- Global Contacts
- Informational Icons Guide
- Material Overview • DIN
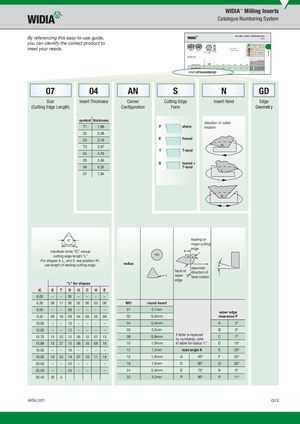
WIDIA™ Milling Inserts
By referencing this easy-to-use guide,
you can identify the correct product to
meet your needs.
07 04
Size Insert Thickness
(Cutting Edge Length)
symbol thickness
| T1 | 1,98 |
| 02 | 2,38 |
| 03 | 3,18 |
| T3 | 3,97 |
| 04 | 4,76 |
| 05 | 5,56 |
| 06 | 6,35 |
| 07 | 7,94 |
AN
Corner
Confi guration
Face Mills • Victory™ M1200 Mini Series Inserts
P M fi rst choice K
| HNPJ-GD | HNPJ-HD | alternate choice | N | ||||
| S | |||||||
| n | H | ||||||
| HNPJ-GD | |||||||
| cutting | ε | ||||||
| catalogue number | edges | D | L10 | S | BS | R | hm |
| HNPJ0704ANSNGD | 12 | 13 | 6,80 | 4,45 | 1,27 | 1,20 | 0,10 |
| HNPJ0704ANSNGD | |||||||
| nnnn HNPJ-HD |
S N GD
Cutting Edge Insert Hand Edge
Form Geometry
direction of cutter
F sharp rotation
E honed
T T-land
S honed + T-land
leading or major cutting edge inscribed circle “iC” versus cutting edge length “L” M0 For shapes A, L, and X, see position #1; use length of leading cutting edge. radius assumed facet or direction of wiper feed motion edge “L” for shapes
| iC | S | T | R | O | C | H | E | ||||||
| 6,00 | – | – | 06 | – | – | – | – | ||||||
| 6,35 | 06 | 11 | 06 | 02 | 06 | 03 | 06 | MO | round insert | ||||
| 8,00 | – | – | 08 | – | – | – | – | 01 | 0,1mm | ||||
| wiper edge | |||||||||||||
| 9,52 | 09 | 16 | 09 | 04 | 09 | 05 | 09 | 02 | 0,2mm | clearance P | |||
| 10,00 | – | – | 10 | – | – | – | – | 04 | 0,4mm | A | 3º | ||
| 12,00 | – | – | 12 | – | – | – | – | 05 | 0,5mm | B | 5º | ||
| If letter is replaced | |||||||||||||
| 12,70 | 12 | 22 | 12 | 05 | 12 | 07 | 13 | 08 | 0,8mm | C | 7º | ||
| by number(s), refer | |||||||||||||
| 15,88 | 15 | 27 | 15 | 06 | 16 | 09 | 16 | 10 | 1,0mm | to table for radius “r.” | D | 15º | |
| 16,00 | – | – | 16 | – | – | – | – | 12 | 1,2mm | lead angle K | E | 20º | |
| 19,05 | 19 | 33 | 19 | 07 | 19 | 11 | 19 | 15 | 1,5mm | A | 45º | F | 25º |
| 20,00 | – | – | 20 | – | – | – | – | 16 | 1,6mm | D | 60º | G | 30º |
| 25,00 | – | – | 25 | – | – | – | – | 24 | 2,4mm | E | 75º | N | 0º |
| 25,40 | 25 | 4 | 32 | 3,2mm | P | 90º | P | 11º |