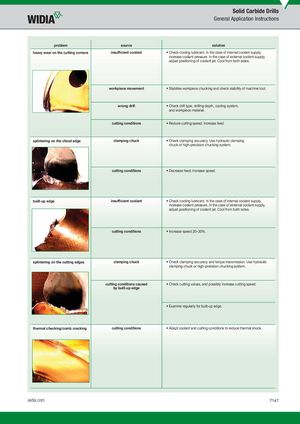
| problem | source | solution |
| heavy wear on the cutting corners | insuffi cient coolant | • Check cooling lubricant. In the case of internal coolant supply, increase coolant pressure. In the case of external coolant supply, adjust positioning of coolant jet. Cool from both sides. |
| workpiece movement | • Stabilise workpiece chucking and check stability of machine tool. |
| wrong drill | • Check drill type, drilling depth, cooling system, and workpiece material. |
| cutting conditions | • Reduce cutting speed; increase feed. |
| splintering on the chisel edge | clamping chuck | • Check clamping accuracy. Use hydraulic clamping chuck or high-precision chucking system. |
| cutting conditions | • Decrease feed; increase speed. |
| built-up edge | insuffi cient coolant cutting conditions | • Check cooling lubricant. In the case of internal coolant supply, increase coolant pressure. In the case of external coolant supply, adjust positioning of coolant jet. Cool from both sides. • Increase speed 20–30%. |
| splintering on the cutting edges | clamping chuck | • Check clamping accuracy and torque transmission. Use hydraulic clamping chuck or high-precision chucking system. |
| cutting conditions caused by built-up edge | • Check cutting values, and possibly increase cutting speed. |
| | • Examine regularly for built-up edge. |
| thermal checking/comb cracking | cutting conditions | • Adapt coolant and cutting conditions to reduce thermal shock. |
 Каталог Widia токарный инструмент 2017
 Каталог Widia трохоидальное фрезерование
 Каталог Widia техническое руководство по разверткам
 Каталог Widia фрезы со сменными пластинами 2016
 Каталог Widia достижения 2020