Каталог Widia инструментальная оснастка - страница 1082
Навигация
 Каталог Widia достижения 2021
 Брошюра Widia решения для аэрокосмической промышленности
 Брошюра Widia техническое руководство
 Каталог Widia токарный инструмент 2020
 Каталог Widia цельные концевые фрезы
 Каталог Widia техническое руководство по разверткам
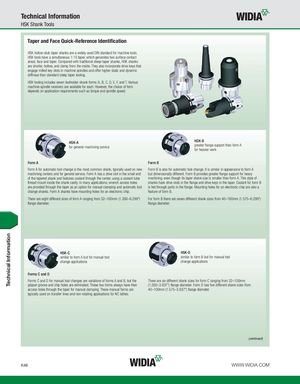
HSK Shank Tools
Taper and Face Quick-Reference Identification
HSK hollow-stub taper shanks are a widely used DIN standard for machine tools. HSK tools have a simultaneous 1:10 taper, which generates two surface contact areas: face and taper. Compared with traditional steep-taper shanks, HSK shanks are shorter, hollow, and clamp from the inside. They also incorporate drive keys that engage milled key-slots in machine spindles and offer higher static and dynamic stiffness than standard steep taper tooling. HSK tooling includes seven toolholder shank forms: A, B, C, D, E, F, and T. Various machine-spindle receivers are available for each. However, the choice of form depends on application requirements such as torque and spindle speed.
HSK-B HSK-A for general-machining service greater flange support than form A for heavier work
| Form A | Form B |
| Form A for automatic tool change is the most common shank, typically used on new | Form B is also for automatic tool change. It is similar in appearance to form A |
| machining centers and for general service. Form A has a drive slot in the small end | but dimensionally different. Form B provides greater flange support for heavy |
| of the tapered shank and features coolant through the center, using a coolant tube | machining, even though its taper shank size is smaller than form A. This style of |
| thread mount inside the shank cavity. In many applications, wrench access holes | shanks have drive slots in the flange and drive keys in the taper. Coolant for form B |
| are provided through the taper as an option for manual clamping and automatic tool | is fed through ports in the flange. Mounting holes for an electronic chip are also a |
| change shanks. Form A shanks have mounting holes for an electronic chip. | feature of form B. |
| There are eight different sizes of form A ranging from 32–160mm (1.260–6.299") | For form B there are seven different shank sizes from 40–160mm (1.575–6.299") |
| flange diameter. | flange diameter. |
HSK-C HSK-D similar to form A but for manual tool similar to form B but for manual tool change applications change applications
Forms C and D Forms C and D for manual tool changes are variations of forms A and B, but the There are six different shank sizes for form C ranging from 32–100mm gripper groove and chip holes are eliminated. These two forms always have their (1.260–3.937") flange diameter. Form D has five different shank sizes from access holes through the taper for manual clamping. These manual forms are 40–100mm (1.575–3.937") flange diameter. typically used on transfer lines and non-rotating applications for NC lathes.
(continued)