Каталог Tungaloy инструмент для автоматов швейцарского типа - страница 304
Навигация
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy глубокое сверление 2
 Каталог Tungaloy зубофрезерование
 Брошюра Tungaloy новая продукция
 Каталог Tungaloy глубокое сверление 1
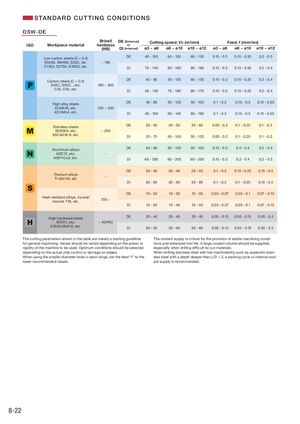
STANDARD CUTTING CONDITIONS
DSW-DE
| Brinell h | DE(External) | Cutting | speed:Vc | (m/min) | Fe | ed:f (mm/r | ev) | ||
| ISO | Workpiece material | ardness (HB) | or DI(Internal) | ø3 ~ ø6 | ø6 ~ ø10 | ø10 ~ ø12 | ø3 ~ ø6 | ø6 ~ ø10 | ø10 ~ ø12 |
| Low carbon steels (C < 0.3) | 180 | DE | 40 - 100 | 60 - 120 | 60 - 130 | 0.15 - 0.3 | 0.15 - 0.35 | 0.2 - 0.5 | |
| SS400, SM490, S25C, etc. C15E4, E275A, E355D, etc. | ~ | DI | 70 - 140 | 80 - 160 | 90 - 190 | 0.15 - 0.3 | 0.15 - 0.35 | 0.2 - 0.5 | |
| Carbon steels (C > 0.3) S45C S55C t | 180 300 | DE | 40 - 90 | 50 - 120 | 60 - 130 | 0.15 - 0.3 | 0.15 - 0.35 | 0.2 - 0.4 | |
| , , , ec. C45, C55, etc. | ~ | DI | 50 - 130 | 70 - 160 | 80 - 170 | 0.15 - 0.3 | 0.15 - 0.35 | 0.2 - 0.4 | |
| High alloy steels | DE | 40 - 80 | 50 - 100 | 50 - 100 | 0.1 - 0.2 | 0.15 - 0.3 | 0.15 - 0.35 | ||
| SCM440 etc | 250 ~ 350 | ||||||||
| , . 42CrMo4, etc. | DI | 40 - 100 | 60 - 140 | 60 - 160 | 0.1 - 0.2 | 0.15 - 0.3 | 0.15 - 0.35 | ||
| Stainless steels | DE | 20 - 40 | 30 - 50 | 30 - 60 | 0.05 - 0.2 | 0.1 - 0.25 | 0.1 - 0.3 | ||
| SUS304, etc. X5CrNi18-9, etc. | ~ 200 | DI | 25 - 75 | 50 - 100 | 50 - 120 | 0.05 - 0.2 | 0.1 - 0.25 | 0.1 - 0.3 | |
| Aluminium alloys ADC12 etc | - | DE | 40 - 90 | 50 - 100 | 50 - 100 | 0.15 - 0.3 | 0.2 - 0.4 | 0.2 - 0.5 | |
| , . AlSi11Cu3, etc. | DI | 60 - 200 | 60 - 200 | 60 - 200 | 0.15 - 0.3 | 0.2 - 0.4 | 0.2 - 0.5 | ||
| Titanium alloys | - | DE | 20 - 40 | 20 - 40 | 20 - 40 | 0.1 - 0.2 | 0.15 - 0.25 | 0.15 - 0.4 | |
| Ti-6Al-4V, etc | DI | 20 - 60 | 30 - 80 | 30 - 80 | 0.1 - 0.2 | 0.1 - 0.25 | 0.15 - 0.4 | ||
| Heat-resistant alloys, Inconel Inconel 718, etc. | 250 ~ | DE DI | 10 - 30 10 - 30 | 10 - 30 10 - 40 | 10 - 30 10 - 40 | 0.03 - 0.07 0.03 - 0.07 | 0.05 - 0.1 0.05 - 0.1 | 0.07 - 0.12 0.07 - 0.15 | |
| High hardened steels | DE | 20 - 40 | 20 - 40 | 20 - 40 | 0.05 - 0.15 | 0.05 - 0.15 | 0.05 - 0.2 | ||
| SKD11, etc. | ~ 40HRC | ||||||||
| X153CrMoV12, etc. | DI | 20 - 50 | 30 - 60 | 30 - 60 | 0.05 - 0.15 | 0.05 - 0.15 | 0.05 - 0.2 |
| The cutting parameters shown in the table are merely a starting guideline | The coolant supply is critical for the provision of stable machining condi- |
| for general machining. Values should be varied depending on the power or | tions and enhanced tool life. A large coolant volume should be supplied, |
| rigidity of the machine to be used. Optimum conditions should be selected | especially when drilling diffi cult-to-cut materials. |
| depending on the actual chip control or damage on edges. | When drilling stainless steel with low machinability such as austenitic stain- |
| When using the smaller diameter tools in each range, set the feed “f” to the | less steel with a depth deeper than L/D = 3, a pecking cycle or internal cool- |
| lower recommended values. | ant supply is recommended. |