Каталог Tungaloy инструмент для автоматов швейцарского типа - страница 300
Навигация
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy глубокое сверление 2
 Каталог Tungaloy зубофрезерование
 Брошюра Tungaloy новая продукция
 Каталог Tungaloy глубокое сверление 1
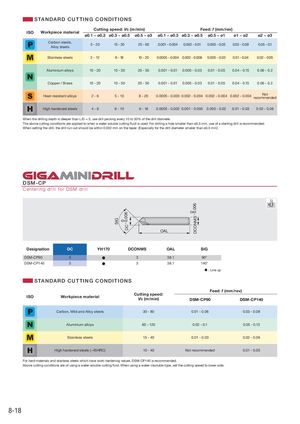
STANDARD CUT TING CONDITIONS
| ISO | Workiece material | Cuttin | g speed:Vc ( | m/min) | Fe | ed:f (mm/re | v) | ||
| p | ø0.1 ~ ø0.3 | ø0.3 ~ ø0.5 | ø0.5 ~ ø3 | ø0.1 ~ ø0.3 | ø0.3 ~ ø0.5 | ø0.5 ~ ø1 | ø1 ~ ø2 | ø2 ~ ø3 | |
| Carbon steels, Alloy steels | 5 - 20 | 15 - 30 | 25 - 60 | 0.001 - 0.004 | 0.002 - 0.01 | 0.005 - 0.05 | 0.03 - 0.09 | 0.05 - 0.1 | |
| Stainless steels | 2 - 12 | 6 - 18 | 10 - 20 | 0.0005 - 0.004 | 0.002 - 0.008 | 0.005 - 0.03 | 0.01 - 0.04 | 0.02 - 0.05 | |
| Aluminium alloys | 10 - 20 | 10 - 30 | 20 - 50 | 0.001 - 0.01 | 0.005 - 0.03 | 0.01 - 0.05 | 0.04 - 0.15 | 0.06 - 0.2 | |
| Copper / Brass | 10 - 20 | 10 - 30 | 20 - 50 | 0.001 - 0.01 | 0.005 - 0.03 | 0.01 - 0.05 | 0.04 - 0.15 | 0.06 - 0.2 | |
| Heat-resistant alloys | 2 - 6 | 5 - 10 | 8 - 20 | 0.0005 - 0.003 | 0.002 - 0.004 | 0.002 - 0.004 | 0.002 - 0.004 | Not recommended | |
| High hardened steels | 4 - 8 | 6 - 10 | 6 - 16 | 0.0005 - 0.002 | 0.001 - 0.005 | 0.005 - 0.02 | 0.01 - 0.03 | 0.02 - 0.06 |
When the drilling depth is deeper than L/D = 5, use drill pecking every 10 to 50% of the drill diameter. The above cutting conditions are applied to when a water soluble cutting fluid is used. For drilling a hole smaller than ø0.3 mm, use of a starting drill is recommended. When setting the drill, the drill run out should be within 0.002 mm on the taper. (Especially for the drill diameter smaller than ø0.5 mm)
DSM-CP
Centering drill for DSM drill
0 0.006-
| Designation | DC | YH170 | DCONMS | ||
| DSM-CP90 | 3 | 䖃 | 3 | ||
| DSM-CP140 | 3 | 䖃 | 3 |
STANDARD CUT TING CONDITIONS
0 0.006-
OAL
OAL SIG
38.1 90° 38.1 140° 䖃 : Line up
Feed: f (mm/rev)
| ISO | Workpiece material | Cutting speed: Vc (m/min) | DSM-CP90 | DSM-CP140 |
| Carbon, Mild and Alloy steels | 30 - 80 | 0.01 - 0.06 | 0.03 - 0.08 | |
| Aluminium alloys | 60 - 120 | 0.02 - 0.1 | 0.05 - 0.15 | |
| Stainless steels | 15 - 40 | 0.01 - 0.03 | 0.02 - 0.06 | |
| High hardened steels (~45HRC) | 10 - 40 | Not recommended | 0.01 - 0.05 |
For hard materials and stainless steels which have work-hardening nature, DSM-CP140 is recommended. Above cutting conditions are of using a water-soluble cutting fluid. When using a water-insoluble type, set the cutting speed to lower side.