Каталог Tungaloy инструмент для автоматов швейцарского типа - страница 203
Навигация
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy глубокое сверление 2
 Каталог Tungaloy зубофрезерование
 Брошюра Tungaloy новая продукция
 Каталог Tungaloy глубокое сверление 1
Technical Guide 1
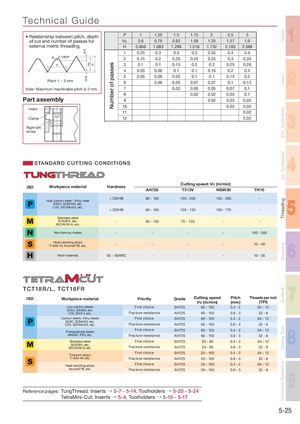
- Relationship between pitch, depth P 1 1.25 1.5 1.75 2 2.5 3 of cut and number of passes for H 0.6 0.76 0.92 1.09 1.25 1.57 1.9
2
external metric threading H 0.866 1.083 1.299 1.516 1.732 2.165 2.598
1 0.25 0.3 0.3 0.3 0.35 0.4 0.4
R 0.1083P 2 0.15 0.2 0.25 0.25 0.25 0.3 0.35
P 3 0.1 0.1 0.15 0.2 0.2 0.25 0.28 2
| 4 | 0.05 0.06 | 0.1 | 0.1 | 0.16 | 0.2 | 0.2 | ||
| 5 | 0.05 0.06 0.05 | 0.1 | 0.1 | 0.15 0.2 | ||||
| Pitch 1 ~ 3 mm | 6 0.06 0.05 0.07 0.07 0.1 0.13 | |||||||
| Note: Maximum machinable pitch is 3 mm. | 7 | 0.02 0.05 0.05 | 0.07 0.1 | |||||
| 8 | 0.02 0.02 | 0.05 0.1 | ||||||
| Part assembly | 9 | 0.02 0.03 0.05 | ||||||
| 10 | 0.02 0.05 | |||||||
| Insert | 3 | |||||||
| 11 | 0.02 | |||||||
| Clamp | 12 | 0.02 |
Right-left screw 4 STANDARD CUTTING CONDITIONS
| Wki til | Hd | Cutting spee | d:Vc (m/min) | |||
| ISO | orpece maera | arness | AH725 | T313V | NS9530 | TH10 |
| High carbon steel / Alloy steel S45C, SCM440, etc. C45, 42CrMoS4, etc. | < 200HB > 200HB | 80 - 180 60 - 160 | 100 - 200 100 - 150 | 150 - 200 100 - 170 | - - | |
| Stainless steel SUS304, etc. X5CrNi18-9, etc. | - | 50 - 130 | 70 - 130 | - | - | |
| Non-ferrous metals | - | - | - | - | 100 - 500 | |
| Heat-resisting alloys Ti-6AI-4V, Inconel718, etc. | - | - | - | - | 10 - 40 | |
| Hard materials | 50 ~ 60HRC | - | - | - | 10 - 30 |
7
TCT18R /L , TCT18FR
| ISO | Workpiece material | Priority | Grade | Cutting speed Vc (m/min) | Pitch (mm) | Threads per inch (TPI) |
| Low carbon steels S15C SS400 t | First choice | SH725 | 60 - 150 | 0.4 - 2 | 64 - 12 | |
| , , ec. C15, St42-1, etc. | Fracture resistance | AH725 | 60 - 150 | 0.8 - 3 | 32 - 8 | |
| Carbon steels, Alloy steels S55C SCM440 etc | First choice | SH725 | 60 - 150 | 0.4 - 2 | 64 - 12 | |
| , , . C55, 42CrMoS4, etc. | Fracture resistance | AH725 | 60 - 150 | 0.8 - 3 | 32 - 8 | |
| Prehardened steels | First choice | SH725 | 60 - 150 | 0.4 - 2 | 64 - 12 | |
| NAK80, PX5, etc. | Fracture resistance | AH725 | 60 - 150 | 0.8 - 3 | 32 - 8 | |
| Stainless steel | First choice | SH725 | 50 - 80 | 0.4 - 2 | 64 - 12 | |
| SUS304, etc. X5CrNi18-9, etc. | Fracture resistance | AH725 | 50 - 80 | 0.8 - 3 | 32 - 8 | |
| Titanium alloys | First choice | SH725 | 30 - 100 | 0.4 - 2 | 64 - 12 | |
| Ti-6AI-4V, etc. | Fracture resistance | AH725 | 30 - 100 | 0.8 - 3 | 32 - 8 | |
| Heat-resisting alloys | First choice | SH725 | 30 - 100 | 0.4 - 2 | 64 - 12 | |
| Inconel718, etc. | Fracture resistance | AH725 | 30 - 100 | 0.8 - 3 | 32 - 8 |
Inconel718, etc. Fracture resistance AH725 30 - 100 0.8 - 3 32 - 8 9
Reference pages: TungThread: Inserts → 5-7 - 5-14, Toolholders → 5-20 - 5-24 TetraMini-Cut: Inserts → 5-4, Toolholders → 5-15 - 5-17