Брошюра Tungaloy новая продукция - страница 133
Навигация
 Каталог Tungaloy глубокое сверление 2
 Каталог Tungaloy глубокое сверление 1
 Каталог Tungaloy зубофрезерование
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy инструмент для автоматов швейцарского типа
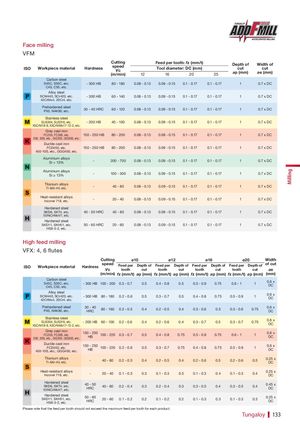
Face milling
VFM
| ISO | Workpiece material | Hardness | Cutting speed Vc | Feedper too Tool diamet | th:fz (mm/t) er: DC(mm) | Depth of cut | Width of cut | ||
| (m/min) | 12 | 16 | 20 | 25 | ap (mm) | ae (mm) | |||
| Carbon steel S45C, S55C, etc. C45, C55, etc. | - 300 HB | 80 - 180 | 0.08 - 0.13 | 0.09 - 0.15 | 0.1 - 0.17 | 0.1 - 0.17 | 1 | 0.7 x DC | |
| Alloy steel SCM440, SCr420, etc. 42CrMo4, 20Cr4, etc. | - 300 HB | 60 - 140 | 0.08 - 0.13 | 0.09 - 0.15 | 0.1 - 0.17 | 0.1 - 0.17 | 1 | 0.7 x DC | |
| Prehardened steel PX5, NAK80, etc. | 30 - 40 HRC | 60 - 120 | 0.08 - 0.13 | 0.09 - 0.15 | 0.1 - 0.17 | 0.1 - 0.17 | 1 | 0.7 x DC | |
| Stainless steel SUS304, SUS316, etc. X5CrNi18-9, X5CrNiMo17-12-2, etc. | - 200 HB | 40 - 100 | 0.08 - 0.13 | 0.09 - 0.15 | 0.1 - 0.17 | 0.1 - 0.17 | 1 | 0.7 x DC | |
| Grey cast iron FC250, FC300, etc. 250, 300, etc., GG250, GG300, etc. | 150 - 250 HB | 80 - 200 | 0.08 - 0.13 | 0.09 - 0.15 | 0.1 - 0.17 | 0.1 - 0.17 | 1 | 0.7 x DC | |
| Ductile cast iron FCD450, etc. 450-10S, etc., GGG450, etc. | 150 - 250 HB | 80 - 200 | 0.08 - 0.13 | 0.09 - 0.15 | 0.1 - 0.17 | 0.1 - 0.17 | 1 | 0.7 x DC | |
| Aluminium alloys Si < 13% | - | 200 - 700 | 0.08 - 0.13 | 0.09 - 0.15 | 0.1 - 0.17 | 0.1 - 0.17 | 1 | 0.7 x DC | |
| Aluminium alloys Si ≥ 13% | - | 100 - 300 | 0.08 - 0.13 | 0.09 - 0.15 | 0.1 - 0.17 | 0.1 - 0.17 | 1 | 0.7 x DC | |
| Titanium alloys Ti-6Al-4V, etc. | - | 40 - 80 | 0.08 - 0.13 | 0.09 - 0.15 | 0.1 - 0.17 | 0.1 - 0.17 | 1 | 0.7 x DC | |
| Heat-resistant alloys Inconel 718, etc. | - | 20 - 40 | 0.08 - 0.13 | 0.09 - 0.15 | 0.1 - 0.17 | 0.1 - 0.17 | 1 | 0.7 x DC | |
| Hardened steel SKD6, SKT4, etc. 55NiCrMoV7, etc. | 40 - 50 HRC | 40 - 80 | 0.08 - 0.13 | 0.09 - 0.15 | 0.1 - 0.17 | 0.1 - 0.17 | 1 | 0.7 x DC | |
| Hardened steel SKD11, SKH51, etc. HS6-5-2, etc. | 50 - 60 HRC | 20 - 60 | 0.08 - 0.13 | 0.09 - 0.15 | 0.1 - 0.17 | 0.1 - 0.17 | 1 | 0.7 x DC |
High feed milling
VFX: 4, 6 flutes
| Cutting | ø1 | 0 | ø1 | 2 | ø1 | 6 | ø | 20 | Width | |||
| ISO | Workpiece material | Hardness | Vc (m/min) speed | fz (mm/t) Feed per tooth | ap (mm) Depth of cut | fz (mm/t) Feed per tooth | ap (mm) Depth of cut | fz (mm/t) Feed per tooth | ap (mm) Depth of cut | fz (mm/t) Feed per tooth | ap (mm) Depth of cut | ae (mm) of cut |
| Carbon steel | 06 x | |||||||||||
| S45C, S55C, etc. C45, C55, etc. | - 300 HB | 100 - 200 | 0.3 - 0.7 | 0.5 | 0.4 - 0.8 | 0.5 | 0.5 - 0.9 | 0.75 | 0.6 - 1 | 1 | . DC | |
| Alloy steel SCM440, SCr420, etc. 42CrMo4, 20Cr4, etc. | - 300 HB | 80 - 180 | 0.2 - 0.6 | 0.5 | 0.3 - 0.7 | 0.5 | 0.4 - 0.8 | 0.75 | 0.5 - 0.9 | 1 | 0.6 x DC | |
| Prehardened steel PX5, NAK80, etc. | 30 - 40 HRC | 80 - 160 | 0.2 - 0.5 | 0.4 | 0.2 - 0.5 | 0.4 | 0.3 - 0.6 | 0.5 | 0.3 - 0.6 | 0.75 | 0.6 x DC | |
| X | Stainless steel SUS304, SUS316, etc. 5CrNi18-9, X5CrNiMo17-12-2, etc. | - 200 HB | 60 - 100 | 0.2 - 0.6 | 0.4 | 0.2 - 0.6 | 0.4 | 0.3 - 0.7 | 0.5 | 0.3 - 0.7 | 0.75 | 0.6 x DC |
| Grey cast iron FC250, FC300, etc. 250, 300, etc., GG250, GG300, etc. | 150 - 250 HB | 100 - 220 | 0.3 - 0.7 | 0.5 | 0.4 - 0.8 | 0.75 | 0.5 - 0.9 | 0.75 | 0.6 - 1 | 1 | 0.6 x DC | |
| Ductile cast iron FCD450, etc. 450-10S, etc., GGG450, etc. | 150 - 250 HB | 100 - 220 | 0.2 - 0.6 | 0.5 | 0.3 - 0.7 | 0.75 | 0.4 - 0.8 | 0.75 | 0.5 - 0.9 | 1 | 0.6 x DC | |
| Titanium alloys Ti-6Al-4V, etc. | - | 40 - 80 | 0.2 - 0.5 | 0.4 | 0.2 - 0.5 | 0.4 | 0.2 - 0.6 | 0.5 | 0.2 - 0.6 | 0.5 | 0.25 x DC | |
| Heat-resistant alloys Inconel 718, etc. | - | 20 - 40 | 0.1 - 0.3 | 0.3 | 0.1 - 0.3 | 0.3 | 0.1 - 0.3 | 0.4 | 0.1 - 0.3 | 0.4 | 0.25 x DC | |
| Hardened steel SKD6, SKT4, etc. 55NiCrMoV7, etc. | 40 - 50 HRC | 40 - 80 | 0.2 - 0.4 | 0.3 | 0.2 - 0.4 | 0.3 | 0.3 - 0.5 | 0.4 | 0.3 - 0.5 | 0.4 | 0.45 x DC | |
| Hardened steel SKD11, SKH51, etc. HS6-5-2, etc. | 50 - 60 HRC | 20 - 60 | 0.1 - 0.2 | 0.2 | 0.1 - 0.2 | 0.2 | 0.1 - 0.3 | 0.3 | 0.1 - 0.3 | 0.3 | 0.25 x DC |
Please note that the feed per tooth should not exceed the maximum feed per tooth for each product.