Каталог TooTool техническая информация 2 - страница 164
Навигация
 Каталог TooTool техническая информация 1
 Общий каталог TooTool
 Каталог TooTool монолитные фрезы
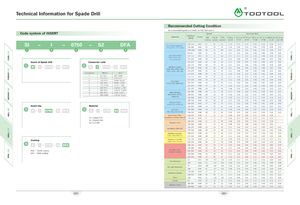
Technical Information for Spade Drill A\
Recommended Cutting Condition
Recommended Speed and Feeds for HSS Drill Inserts
Code system of INSERT Speed Feed (mm/rev)
Hardness
Material Grade TiN TiALN TiCN 9.50 to 13.00 to 17.60 to 24.50 to 35.10 to 48.00 to 65.30 to
(BHN)
m/min m/min m/min 12.50 17.50 24.40 35.00 47.90 65.28 114.48
100-150 M42 61 85 79 0.18 0.25 0.33 0.41 0.51 0.58 0.71
Free Machining Steel
1118, 1215, 12L14, etc 150- 200 M42 55 79 72 0.18 0.25 0.33 0.41 0.51 0.58 0.71
200 + 250 M42 49 73 64 0.15 0.25 0.33 0.41 0.51 0.58 0.71
85 - 125 M42 52 76 67 0.15 0.23 0.30 0.38 0.48 0.58 0.69
Low Carbon Steel 125-175 M42 49 73 64 0.15 0.23 0.30 0.38 0.48 0.58 0.69
1010, 1020, 1025,
1522, 1144, etc. 175 - 225 M42 46 69 59 0.13 0.20 0.25 0.36 0.48 0.53 0.61
Insert of Spade drill Connector code 225 - 275 M42 43 64 55 0.13 0.20 0.25 0.36 0.48 0.53 0.61
125-175 M42 49 73 64 0.15 0.23 0.30 0.38 0.48 0.58 0.69
0750 DFA Medium Carbon 175-225 M42 46 69 59 0.13 0.20 0.25 0.36 0.46 0.53 0.61
Steel 1030, 1040, 1050,
1527, 1140, 1151, etc. 225 -275 M42 43 64 55 0.13 0.20 0.25 0.36 0.46 0.53 0.61
Connector Metric Inch 275-325 M40 40 59 52 0.10 0.18 0.23 0.30 0.41 0.48 0.56
Y 9.5 -11.0 3/8 " - 27/64"
125-175 M42 46 64 59 0.15 0.20 0.25 0.36 0.43 0.48 0.56
Z 11.5 -12.5 7/16" -l/2"
175-225 M42 43 59 55 0.13 0.20 0.25 0.36 0.43 0.48 0.56
0 13.0-17.5 33/64" -11/16" Alloy Steel
1 18.0-24.0 45/64" -15/16” 4140, 5140, 8640, etc. 225 -275 M42 40 55 52 0.13 0.18 0.25 0.36 0.43 0.48 0.56
2 24.5 - 35.00 31/ 32" -!3/8 " 275 - 325 M40 37 52 47 0.10 0.15 0.23 0.30 0.38 0.43 0.51
3 36.0 - 47.0 113/32 " -l7/8"
325 - 375 M40 34 47 44 0.08 0.15 0.23 0.30 0.38 0.43 0.51
4 48.0 -65.0 1 29/32"- 2 9/16"
225 - 300 M40 24 34 30 0.13 0.18 0.23 0.25 0.36 0.43 0.51
5 66.0 - 89.0 2 5 /8" - 3 1/ 2 " High Strength
7 90.0-114.0 3 17/32 " -4 1/2 " Alloy 4340, 4330V, 300-350 M40 18 26 24 0.10 0.18 0.23 0.25 0.36 0.43 0.51
300M, etc.
350-400 M40 15 21 20 0.08 0.15 0.20 0.23 0.30 0.38 0.46
100-150 M42 43 61 55 0.15 0.25 0.30 0.36 0.46 0.53 0.66
Structural Steel
150-250 M42 37 52 47 0.13 0.23 0.25 0.30 0.41 0.48 0.61
A 36, A 516, A 285, etc
Insert dia. Material 250 - 350 M40 30 43 40 0.10 0.20 0.23 0.25 0.36 0.43 0.51
Tool Steel 150 - 200 M40 24 34 32 0.10 0.15 0.20 0.25 0.30 0.38 0.43
0750 750 H13, H12, A4, S3, etc 200-250 M40 18 27 26 0.10 0.15 0.20 0.25 0.30 0.38 0.43
High Temp, Alloy 140 - 220 M40 9 12 11 0.08 0.18 0.20 0.25 0.30 0.38
S2 = Cobalt HSS Hastelloy B, Inconel 600, etc 220-310 M40 8 11 9 0.08 0.15 0.18 0.20 0.25 0.30
S6= Powder HSS 140-220 M40 11 11 14 0.08 0.18 0.20 0.25 0.30 0.38
G2 = Carbide Titanium Alloy
220-310 M40 9 15 11 0.08 0.15 0.18 0.20 0.25 0.30
185-275 M40 23 32 29 0.15 0.20 0.23 0.25 0.36 0.41 0.51
Aerospace Alloy S82
275 -350 M40 18 27 24 0.13 0.18 0.20 0.20 0.30 0.36 0.46
Stainless steel 400 185 - 275 M40 23 32 29 0.15 0.20 0.23 0.25 0.36 0.41 0.51
series, 416, 420, etc. 275 -350 M40 18 27 24 0.13 0.18 0.20 0.20 0.30 0.36 0.46
Stainless steel 300 135 -185 M40 23 32 29 0.08 0.18 0.20 0.25 0.36 0.41 0.51
Coating
series, 304, 316, etc. 185-275 M40 18 27 24 0.08 0.15 0.18 0.20 0.30 0.36 0.46
0750 DFA 120-150 M42 52 76 67 0.18 0.30 0.41 0.51 0.61 0.69 0.76
150-200 M42 46 69 59 0.15 0.28 0.36 0.46 0.56 0.64 0.71
Nodular, Grey,
DFA = TiALN coating 200- 220 M42 40 59 52 0.15 0.23 0.30 0.41 0.46 0.53 0.61
Ductile Cast Iron
DFS = TiSiN coating 220-260 M40 34 50 44 0.13 0.18 0.23 0.30 0.36 0.43 0.51
260 - 320 M40 27 41 37 0.10 0.15 0.18 0.23 0.30 0.36 0.41
30 M42 183 259 229 0.20 0.33 0.41 0.51 0.56 0.64 0.64
Cast Aluminum
180 M42 91 137 122 0.20 0.33 0.41 0.46 0.56 0.64 0.64
30 M42 183 259 229 0.10 0.15 0.25 0.30 0.56 0.64 0.64
Wrought Aluminum
180 M42 91 137 122 0.20 0.33 0.41 0.46 0.56 0.64 0.64
100-200 M40 52 76 67 0.15 0.28 0.36 0.46 0.56 0.66 0.71
Aluminum Bronze
200- 250 M40 40 58 52 0.13 0.18 0.23 0.30 0.36 0.43 0.51
Brass 100 M42 91 136 122 0.18 0.30 0.41 0.51 0.61 0.71 0.76
Copper 60 M40 40 50 46 0.05 0.08 0.15 0.20 0.30 0.36 0.41
300-400 M40 15 29 21 0.08 0.15 0.20 0.23 0.30 0.41 0.46
Hardness Steel
400 - 500 M40 11 14 12 0.05 0.13 0.18 0.20 0.25 0.30 0.41
683 684