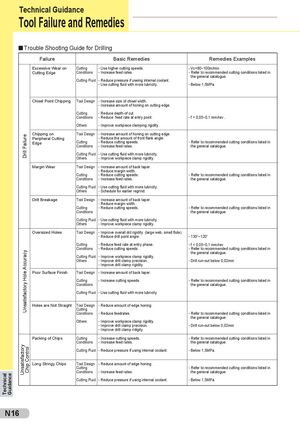
| Failure | | Basic Remedies | Remedies Examples |
| Excessive Wear on Cutting Edge | Cutting Conditions Cutting Fluid | - Use higher cutting speeds. - Increase feed rates. - Reduce pressure if useing internal coolant. - Use cutting fluid with more lubricity. | - Vc=80~100m/min - Refer to recommended cutting conditions listed in the general catalogue. - Below 1,5MPa. |
| Chisel Point Chipping | Tool Design Cutting Conditions Others | - Increase size of chisel width. - Increase amount of honing on cutting edge. - Reduce depth-of cut. - Reduce feed rate at entry point. - Improve workpiece clamping rigidity. | - f = 0,05~0,1 mm/rev . |
| Drill Failure | Chipping on Peripheral Cutting Edge | Tool Design Cutting Conditions Cutting Fluid Others | - Increase amount of honing on cutting edge. - Reduce the amount of front flank angle. - Reduce cutting speeds. - Increase feed rates. - Use cutting fluid with more lubricity. - Improve workpiece clamp rigidity. | - Refer to recommended cutting conditions listed in the general catalogue. |
| Margin Wear | Tool Design Cutting Conditions Cutting Fluid Others | - Increase amount of back taper. - Reduce margin width. - Reduce cutting speeds. - Increase feed rates. - Use cutting fluid with more lubricity. - Schedule for earlier regrind. | - Refer to recommended cutting conditions listed in the general catalogue. |
| Drill Breakage | Tool Design Cutting Conditions Cutting Fluid Others | - Increase amount of back taper. - Reduce margin width. - Reduce cutting speeds. - Use cutting fluid with more lubricity. - Improve workpiece clamp rigidity. | - Refer to recommended cutting conditions listed in the general catalogue. |
| Oversized Holes | Tool Design | - Improve overall dril rigidity. (large web, small flute). - Reduce drill point angle. | - 130°~120° |
| Accuracy | | Cutting Conditions Cutting Fluid Others | - Reduce feed rate at entry phase. - Reduce cutting speeds. - Improve workpiece clamp rigidity. - Improve drill clamp precision. - Improve drill clamp rigidity. | - f = 0,05~0,1 mm/rev - Refer to recommended cutting conditions listed in the general catalogue. - Drill run-out below 0,02mm |
| isfactory Hole | Poor Surface Finish | Tool Design Cutting Conditions Cutting Fluid | - Increase amount of back taper. - Increase cutting speeds. - Use cutting fluid with more lubricity. | - Refer to recommended cutting conditions listed in the general catalogue. |
| Unsat | Holes are Not Straight | Tool Design Cutting Conditions Others | - Reduce amount of edge honing. - Reduce feedrates. - Improve workpiece clamp rigidity. - Improve drill clamp precision. - Improve drill clamp ridigity. | - Refer to recommended cutting conditions listed in the general catalogue. - Drill run-out below 0,02mm |
| Packing of Chips | Cutting Conditions | - Increase cutting speeds. - Increase feed rates. | - Refer to recommended cutting conditions listed in the general catalogue. |
| factory ontrol | | Cutting Fluid | - Reduce pressure if using internal coolant. | - Below 1,5MPa. |
| Unsatis Chip C | Long Stringy Chips | Tool Design Cutting Conditions Cutting Fluid | - Reduce amount of edge honing. - Increase feed rates. - Reduce pressure if using internal coolant. | - Refer to recommended cutting conditions listed in the general catalogue. - Below 1,5MPa. |
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части