Общий каталог Sumitomo 2018 - 2019 - страница 563
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
Technical Guidance
Basics of Milling
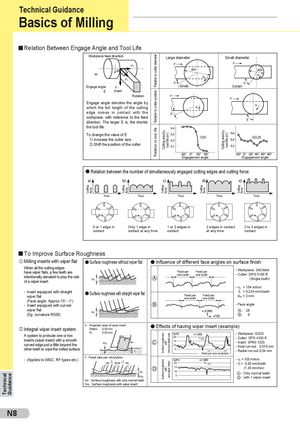
Relation Between Engage Angle and Tool Life
Workpiece feed direction
Relation to cutter position Relation to cutter diameter
Large diameter Small diameter
F F
F2
øD
B
N
N
F3
E E
Engage angle F1 (Small) (Large)
E Insert
Rotation F
F
Engage angle denotes the angle by N
which the full length of the cutting N
edge comes in contact with the E
workpiece, with reference to the feed
E
direction. The larger E is, the shorter
the tool life.
Relation to tool life
Cutting area by
Cutting area by
To change the value of E:
tool life (m3)
tool life (m3)
C50 GG25
1) Increase the cutter size
2) Shift the position of the cutter
Engagement angle Engagement angle
l Relation between the number of simultaneously engaged cutting edges and cutting force:
Cutting
Cutting
Cutting
Cutting
Cutting
force
force
force
force
force
Time Time Time Time Time
0 or 1 edge in Only 1 edge in 1 or 2 edges in 2 edges in contact 2 to 3 edges in
contact contact at any time. contact at any time. contact
To Improve Surface Roughness
j Milling inserts with wiper flat l Surface roughness without wiper flat l Influence of different face angles on surface finish
When all the cutting edges
- Workpiece: 34CrMo4
have wiper flats, a few teeth are Feed per Feed per
- Cutter: DPG 5160 R
one tooth one tooth
intentionally elevated to play the role A (Single tooth)
HC
of a wiper insert.
- vc = 154 m/min
- Insert equipped with straight f t = 0,234 mm/tooth
l Surface roughness with straight wiper flat Feed per Feed per doc = 2 mm
wiper flat one tooth one tooth
(Face angle: Approx 15’ - 1°)
- Insert equipped with curved B - Face angle
wiper flat HF
A : 28’
(Eg. curvature R500) B : 6’
h : Projected value of wiper insert
l Effects of having wiper insert (example)
k Integral wiper insert system Steels : 0,05 mm
Al : 0,03 mm - Workpiece: GG25
common teeth only
Surface roughness
A system to protrude one or two 20
20 - Cutter: DPG 4100 R
inserts (wiper insert) with a smooth 15
C - Insert: SPKN 1203
with
HW
curved edge just a little beyond the 10
- Axial run-out: 0,015 mm
other teeth to wipe the milled surface. h
5
- Radial run-out: 0,04 mm
Feed per one revolution
f : Feed rate per revolution
- (Applies to WGC, RF types etc.) - vc = 105 m/min
Surface roughness
f f
one wiper insert
20 20 - f t = 0,29 mm/tooth
15 (1,45 mm/rev)
D
with
HC 10
C : Only normal teeth
Technical
Guidance
HW 5
D : with 1 wiper insert
Hc : Surface roughness with only normal teeth
Hw : Surface roughness with wiper insert
N8
Basics of Milling
Relation Between Engage Angle and Tool Life
Workpiece feed direction
Relation to cutter position Relation to cutter diameter
Large diameter Small diameter
F F
F2
øD
B
N
N
F3
E E
Engage angle F1 (Small) (Large)
E Insert
Rotation F
F
Engage angle denotes the angle by N
which the full length of the cutting N
edge comes in contact with the E
workpiece, with reference to the feed
E
direction. The larger E is, the shorter
the tool life.
Relation to tool life
Cutting area by
Cutting area by
To change the value of E:
tool life (m3)
tool life (m3)
C50 GG25
1) Increase the cutter size
2) Shift the position of the cutter
Engagement angle Engagement angle
l Relation between the number of simultaneously engaged cutting edges and cutting force:
Cutting
Cutting
Cutting
Cutting
Cutting
force
force
force
force
force
Time Time Time Time Time
0 or 1 edge in Only 1 edge in 1 or 2 edges in 2 edges in contact 2 to 3 edges in
contact contact at any time. contact at any time. contact
To Improve Surface Roughness
j Milling inserts with wiper flat l Surface roughness without wiper flat l Influence of different face angles on surface finish
When all the cutting edges
- Workpiece: 34CrMo4
have wiper flats, a few teeth are Feed per Feed per
- Cutter: DPG 5160 R
one tooth one tooth
intentionally elevated to play the role A (Single tooth)
HC
of a wiper insert.
- vc = 154 m/min
- Insert equipped with straight f t = 0,234 mm/tooth
l Surface roughness with straight wiper flat Feed per Feed per doc = 2 mm
wiper flat one tooth one tooth
(Face angle: Approx 15’ - 1°)
- Insert equipped with curved B - Face angle
wiper flat HF
A : 28’
(Eg. curvature R500) B : 6’
h : Projected value of wiper insert
l Effects of having wiper insert (example)
k Integral wiper insert system Steels : 0,05 mm
Al : 0,03 mm - Workpiece: GG25
common teeth only
Surface roughness
A system to protrude one or two 20
20 - Cutter: DPG 4100 R
inserts (wiper insert) with a smooth 15
C - Insert: SPKN 1203
with
HW
curved edge just a little beyond the 10
- Axial run-out: 0,015 mm
other teeth to wipe the milled surface. h
5
- Radial run-out: 0,04 mm
Feed per one revolution
f : Feed rate per revolution
- (Applies to WGC, RF types etc.) - vc = 105 m/min
Surface roughness
f f
one wiper insert
20 20 - f t = 0,29 mm/tooth
15 (1,45 mm/rev)
D
with
HC 10
C : Only normal teeth
Technical
Guidance
HW 5
D : with 1 wiper insert
Hc : Surface roughness with only normal teeth
Hw : Surface roughness with wiper insert
N8