Общий каталог Sumitomo 2018 - 2019 - страница 478
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
H SUMIBORON
Hardened Steel One-Use Wiper Inserts
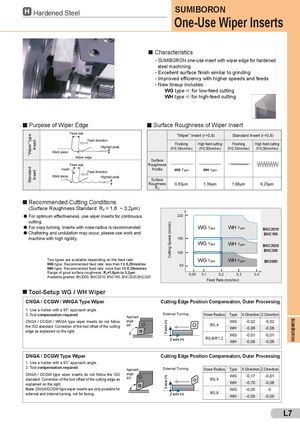
Characteristics
- SUMIBORON one-use insert with wiper edge for hardened
steel machining
- Excellent surface finish similar to grinding
- Improved efficiency with higher speeds and feeds
- New lineup includes:
WG type a for low-feed cutting
WH type a for high-feed cutting
Purpose of Wiper Edge Surface Roughness of Wiper Insert
| Feed rate | ”Wiper” Insert (r=0,8) | Standard Insert (r=0,8) | |||
| Feed direction | |||||
| Finishing | High feed cutting | Finishing | High feed cutting | ||
| Highest peak | (f=0,10mm/rev) | (f=0,30mm/rev) | (f=0,10mm/rev) | (f=0,30mm/rev) | |
| Work piece | |||||
| Wiper edge | |||||
| Surface | |||||
| Feed rate | Roughness |
| Insert | Profile | WG Type | WH Type | |||||
| Feed direction | ||||||||
| Work piece | Highest peak | |||||||
| Surface | ||||||||
| Roughness | 0,63µm | 1,39µm | 1,98µm | 9,20µm |
R Z Recommended Cutting Conditions (Surface Roughness Standard: Rz = 1,6 ~ 3,2µm)
l For optimum effectiveness, use wiper inserts for continuous 220 cutting.
l For copy turning, inserts with nose-radius is recommended. WG T WH T
| ype | ype | BNC2010 | |
| l Chattering and undulation may occur, please use work and | BNC160 | ||
| machine with high rigidity. 150 | |||
| WG T | WH | ||
| ype | Type | BNC2020 | |
| BNC200 | |||
| 100 |
| Two types are available depending on the feed rate: | WG T | WH T | BN2000 | |||
| ype | ype | |||||
| WG type: Recommended feed rate: less than f ≤ 0,20mm/rev | 50 | |||||
| WH type: Recommended feed rate: more than f ≥ 0,20mm/rev |
Range of good surface roughness: Rz=1,6µm to 3,2µm 0,05 0,1 0,2 0,3 0,4
Available grades: BN2000, BNC2010, BNC160, BNC2020,BNC200 Feed Rate (mm/rev) Tool-Setup WG / WH Wiper CNGA / CCGW / WNGA Type Wiper Cutting Edge Position Compensation, Outer Processing
1. Use a holder with a 95° approach angle.
| External Turning | Nose Radius | Type | X-Direction | Z-Direction |
| axis (+) | R0,4 | WG WH | -0,02 -0,06 | -0,02 -0,06 |
| X Z axis (+) | R0,8/R1,2 | WG WH | -0,01 -0,06 | -0,01 -0,06 |
Approach edge as explained on the right.
DNGA / DCGW Type Wiper Cutting Edge Position Compensation, Outer Processing
1. Use a holder with a 93° approach angle.
| Approach | External Turning | Nose Radius | Type | X-Direction | Z-Direction |
| angle 93° | axis (+) | R0,4 | WG WH | -0,17 -0,70 | -0,01 -0,06 |
| X Z axis (+) | R0,8 | WG WH | -0,05 -0,58 | 0 -0,05 |