Каталог Stellram токарный инструмент - страница 201
Навигация
 Каталог Stellram материалы и сплавы
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram фрез со сменными пластинами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
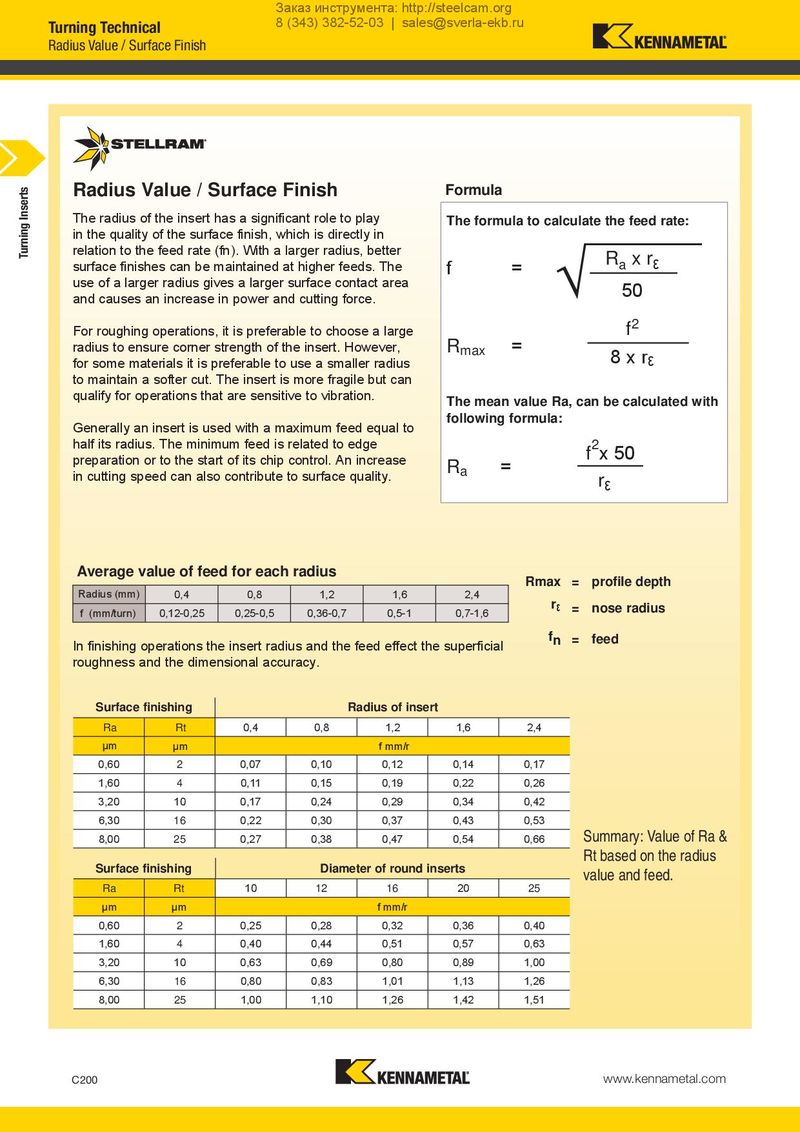
Radius Value / Surface Finish
Radius Value / Surface Finish Formula
The radius of the insert has a significant role to play
The formula to calculate the feed rate:
in the quality of the surface finish, which is directly in
relation to the feed rate (fn). With a larger radius, better ε
| surface finishes can be maintained at higher feeds. The | f | R x r = |
| a | ||
| use of a larger radius gives a larger surface contact area | 50 | |
| and causes an increase in power and cutting force. | ||
| For roughing operations, it is preferable to choose a large | f2 | |
| radius to ensure corner strength of the insert. However, | R | = |
max 8 x rε for some materials it is preferable to use a smaller radius to maintain a softer cut. The insert is more fragile but can qualify for operations that are sensitive to vibration.
The mean value Ra, can be calculated with
Generally an insert is used with a maximum feed equal to following formula:
half its radius. The minimum feed is related to edge 2x 50
| preparation or to the start of its chip control. An increase | = | f | |
| R |
in cutting speed can also contribute to surface quality. a rε
Average value of feed for each radius
Rmax = profile depth
| Radius (mm) | 0,4 | 0,8 | 1,2 | 1,6 | 2,4 | |||||
| rε | ||||||||||
| f (mm/turn) | 0,12-0,25 | 0,25-0,5 | 0,36-0,7 | 0,5-1 | 0,7-1,6 | = nose radius |
In finishing operations the insert radius and the feed effect the superficial fn = feed roughness and the dimensional accuracy.
| Surface f | inishing | R | adius of inse | rt | ||
| Ra | Rt | 0,4 | 0,8 | 1,2 | 1,6 | 2,4 |
| µm | µm | f mm/r | ||||
| 0,60 | 2 | 0,07 | 0,10 | 0,12 | 0,14 | 0,17 |
| 1,60 | 4 | 0,11 | 0,15 | 0,19 | 0,22 | 0,26 |
| 3,20 | 10 | 0,17 | 0,24 | 0,29 | 0,34 | 0,42 |
| 6,30 | 16 | 0,22 | 0,30 | 0,37 | 0,43 | 0,53 |
| 8,00 | 25 | 0,27 | 0,38 | 0,47 | 0,54 | 0,66 |
| Surface f | inishing | Diame | ter of round i | nserts | ||
| Ra | Rt | 10 | 12 | 16 | 20 | 25 |
| µm | µm | f mm/r | ||||
| 0,60 | 2 | 0,25 | 0,28 | 0,32 | 0,36 | 0,40 |
| 1,60 | 4 | 0,40 | 0,44 | 0,51 | 0,57 | 0,63 |
| 3,20 | 10 | 0,63 | 0,69 | 0,80 | 0,89 | 1,00 |
| 6,30 | 16 | 0,80 | 0,83 | 1,01 | 1,13 | 1,26 |
| 8,00 | 25 | 1,00 | 1,10 | 1,26 | 1,42 | 1,51 |