Каталог Stellram фрез со сменными пластинами - страница 4
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
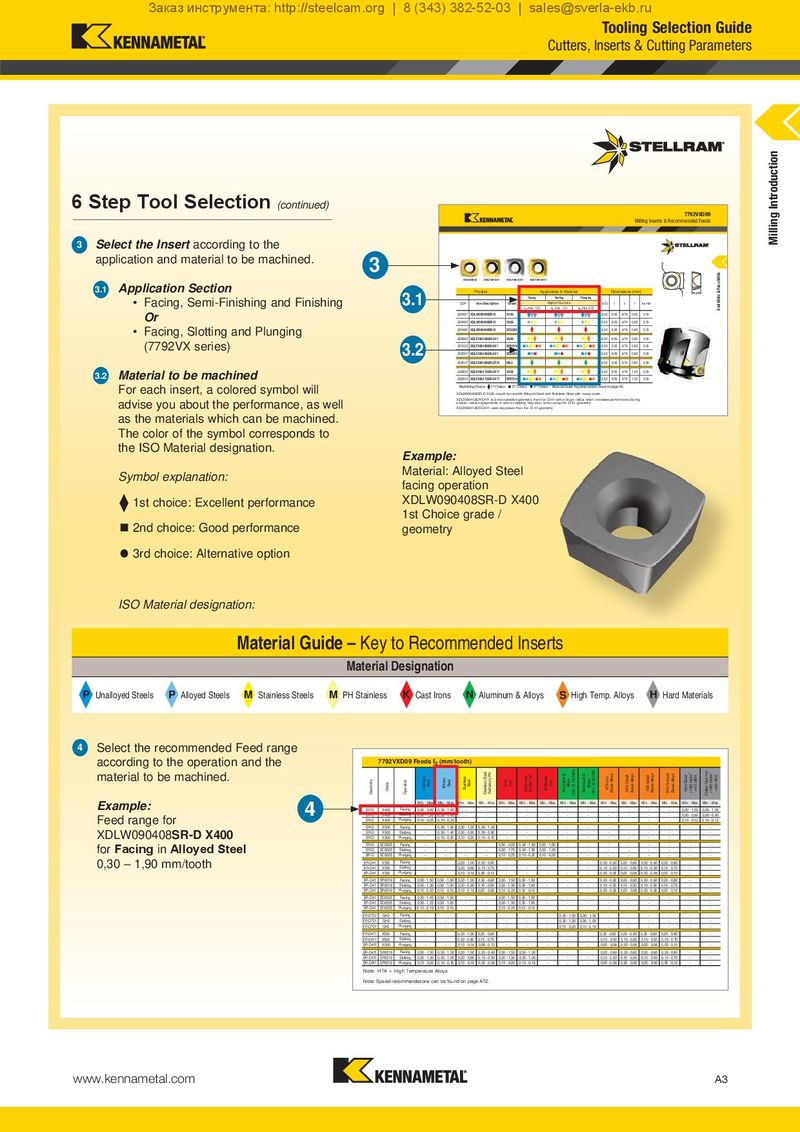
6 Step Tool Selection
(continued)
7792VXD09
Milling Inserts & Recommended Feeds
3 Select the Insert according to the
application and material to be machined. 3
d
| Application Section | XDLW09-D | XDLT09-D41 | XDLT09-D721 | XDLT09-D411 | l | |||
| 3.1 | ||||||||
| 3.1 | Product | Application & Material | s Dimensions (mm) | |||||
| • Facing, Semi-Finishing and Finishing | Facing Slotting | Plunging | r | |||||
| EDP | Item Description | Grade | Depth of Cut (mm) | d (IC) | l s r hm min | |||
| ap max. 1,50 ap max. 1,50 | ae max. 6,00 | |||||||
| Or | 029487 | XDLW090408SR-D | X400 | 9,52 9,52 4,76 0,80 | 0,10 | |||
| 029485 | XDLW090408SR-D | X500 | 9,52 9,52 4,76 0,80 | 0,10 | ||||
| • Facing, Slotting and Plunging | 029486 | XDLW090408SR-D | SC3025 | 9,52 9,52 4,76 0,80 | 0,10 | |||
| 029685 | XDLT090408ER-D41 | X500 | 9,52 9,52 4,76 0,80 | 0,05 | ||||
| (7792VX series) | 3.2 031535 | XDLT090408ER-D41 | SP6519 | 9,52 9,52 4,76 0,80 | 0,05 | |||
| 033067 | XDLT090408ER-D41 | SC6525 | 9,52 9,52 4,76 0,80 | 0,05 | ||||
| 029637 | XDLT090408ER-D721 | GH2 | 9,52 9,52 4,76 0,80 | 0,04 | ||||
| 3.2 | Material to be machined | 030853 | XDLT090412ER-D411 | X500 | 9,52 9,52 4,76 1,20 | 0,05 | ||
| 030854 | XDLT090412ER-D411 | SP6519 | 9,52 9,52 4,76 1,20 | 0,05 |
For each insert, a colored symbol will Machining Choice: 1st Choice 2nd Choice 3rd Choice | Material Guide Key descriptions found on page A5. XDLW090408SR-D X500 should be used for Alloyed Steel and Stainless Steel with heavy scale. advise you about the performance, as well XDLT090412ER-D411 is a more positive geometry than the -D-41 with a larger radius which increases performance during smaller radial engagements or where chipping may occur when using the -D-41 geometry.
XDLT090412ER-D411 uses less power than the -D-41 geometry. as the materials which can be machined. 7792VXD09 Feeds fz (mm/tooth)
The color of the symbol corresponds to
Alloyed Steel Gray Iron Hard Steel >1400 N/mm
| the ISO Material designation. | Spheroidal- Ductile Iron | Chilled Cast Iron >1400 N/mm | ||
| Example: | Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. |
| SR-D X400 | Facing | 0,30 - 2,00 0,30 - 1,90 | - | - | - | - | - - | - - | - | - | - 0,30 - 1,00 0,30 - 1,00 | ||||||
| SR-D X400 | Slotting | 0,30 - 1,50 0,30 - 1,45 | - | - | - | - | - - | - - | - | - | - 0,30 - 0,60 0,30 - 0,80 | ||||||
| SR-D X400 | Plunging | 0,10 - 0,25 0,10 - 0,23 | - | - | - | - | - - | - - | - | - | - 0,10 - 0,12 0,10 - 0,127792VXD09 | ||||||
| Material: Alloyed Steel SR-DX500Facing-0,30 - 1,90 0,30 - 1,20 0,30 - 1,00 | - | - | - - | - - | - | - | - - | - | |||||||||
| Symbol explanation: | SR-D X500 | Slotting | - 0,30 - 1,40 0,30 - 0,90 0,30 - 0,80 | - | - | - - | - - | - | - | - | - | - | |||||
| SR-D X500 | Plunging | - 0,10 - 0,22 0,10 - 0,20 0,10 - 0,15 | - | - | - - | Milling Inserts & Recommended Feeds------- | |||||||||||
| facing operationSR-DSC3025Facing | - | - | - | - 0,30 - 2,00 0,30 - 1,80 0,30 - 1,50 | - | - - | - | - | - | - | - | ||||||
| SR-D SC3025 | Slotting | - | - | - | - 0,30 - 1,70 0,30 - 1,50 0,30 - 1,30 | - | - - | - | - | - | - | - | |||||
| SR-D SC3025 | Plunging | - | - | - | - 0,10 - 0,25 0,10 - 0,22 0,10 - 0,20 | - | - - | - | - | - | - | - | |||||
| ER-D41 | X500 | Facing | - | - 0,20 - 1,00 0,20 - 0,80 | - | - | - - | - 0,20 - 0,60 0,20 - 0,60 0,20 - 0,60 0,20 - 0,80 | - | - | |||||||
| 1st choice: Excellent performance | XDLW090408SR-D X400ER-D41X500Slotting--0,20 - 0,80 0,15 - 0,70 | - | - | - - | - 0,10 - 0,50 0,10 - 0,50 0,10 - 0,50 0,10 - 0,70 | - | - | ||||||||||
| ER-D41 | X500 | Plunging | - | - 0,10 - 0,16 0,08 - 0,12 | - | - | - - | - 0,05 - 0,08 0,05 - 0,08 0,05 - 0,08 0,05 - 0,10 | - | - | |||||||
| ER-D41 SP6519 | Facing | 0,30 - 1,50 0,30 - 1,30 0,20 - 1,00 0,20 - 0,60 0,30 - 1,50 0,30 - 1,30 | - - | - 0,20 - 0,60 0,20 - 0,60 0,20 - 0,60 0,20 - 0,80 | - | - | |||||||||||
| 1st Choice grade / ER-D41 SP6519Slotting0,30 - 1,30 0,30 - 1,00 0,20 - 0,80 0,15 - 0,50 0,30 - 1,30 0,30 - 1,00 | - - | - 0,10 - 0,50 0,10 - 0,50 0,10 - 0,50 0,10 - 0,70 | - | - | |||||||||||||
| ER-D41 SP6519 | Plunging | 0,10 - 0,20 0,10 - 0,16 0,10 - 0,16 0,05 - 0,08 0,10 - 0,20 0,10 - 0,16 | - - | - 0,05 - 0,08 0,05 - 0,08 0,05 - 0,08 0,05 - 0,10 | - | - | |||||||||||
| ER-D41 SC6525 | Facing | 0,30 - 1,45 0,30 - 1,30 | - | - 0,30 - 1,50 0,30 - 1,30 | - - | - - | - | - | - | - | - | ||||||
| ER-D41 SC6525 | Slotting | 0,30 - 1,25 0,30 - 1,00 | - | - 0,30 - 1,30 0,30 - 1,00 | - - | - - | - | - | - | - | - | ||||||
| 2nd choice: Good performance | geometry ER-D41 SC6525 | Plunging | 0,10 - 0,18 0,10 - 0,16 | - | - 0,10 - 0,20 0,10 - 0,16 | - - | - - | - | - | - | - | - | |||||
| ER-D721 | GH2 | Facing | - | - | - | - | - | - | - 0,30 - 1,50 0,30 - 1,30 | - | - | - | - | - | - | ||
| ER-D721 | GH2 | Slotting | - | - | - | - | - | - | - 0,30 - 1,30 0,30 - 1,00 | - | - | - | - | - | - | ||
| ER-D721 | GH2 | Plunging | - | - | - | - | - | - | - 0,10 - 0,20 0,10 - 0,16 | - | - | d - | - | - | - | ||
| ER-D411 X500 | Facing | - | - 0,20 - 1,00 0,20 - 0,80 | - | - | - - | - 0,20 - 0,60 0,20 - 0,60 0,20 - 0,60 0,20 - 0,80 | - | - | ||||||||
| 3rd choice: Alternative option | ER-D411 X500 | Slotting | - | - 0,20 - 0,80 0,15 - 0,70 | - | - | - - | - 0,10 - 0,50 0,10 - 0,50 0,10 - 0,50 0,10 - 0,70 | - | - | |||||||
| ER-D411 X500 | Plunging | - | - 0,10 - 0,16 0,08 - 0,12 | - | - | - - | - 0,05 - 0,08 0,05 - 0,08 0,05 - 0,08 0,05 - 0,10 | - | - | ||||||||
| ER-D411 SP6519 | Facing | 0,30 - 1,50 0,30 - 1,30 0,20 - 1,00 0,20 - 0,60 0,30 - 1,50 0,30 - 1,30 | - - | - 0,20 - 0,60 0,20 - 0,60 0,20 - 0,60 0,20 - 0,80 | - | - | |||||||||||
| XDLT09-D721ER-D411 SP6519XDLT09-D411Slotting XDLT09-D41 XDLW09-D | 0,30 - 1,30 0,30 - 1,00 0,20 - 0,80 0,15 - 0,50 0,30 - 1,30 0,30 - 1,00 | - - | - 0,10 - 0,50 0,10 - 0,50 0,10 - 0,50 0,10 - 0,70 | l - | - | ||||||||||||
| ER-D411 SP6519 | Plunging | 0,10 - 0,20 0,10 - 0,16 0,10 - 0,16 0,05 - 0,08 0,10 - 0,20 0,10 - 0,16 | - - | - 0,05 - 0,08 0,05 - 0,08 0,05 - 0,08 0,05 - 0,10 | - | - | |||||||||||
| Note: HTA = High Temperature Alloys | |||||||||||||||||
| Product Note: Speed recommendations can be found on page A72.Application & Material | Dimensions (mm) | s | |||||||||||||||
| Facing | Slotting | Plunging | r | ||||||||||||||
| EDP | Grade Item Description | www.kennametal.comDepth of Cut (mm) | d (IC) | l s | r h m min | A67 | |||||||||||
| ISO Material designation: | ap max. 1,50 | ap max. 1,50 | a e max. 6,00 | ||||||||||||||
| 029487 | X400 XDLW090408SR-D | 9,52 9,52 4,76 0,80 | 0,10 | ||||||||||||||
| 029485 | X500 XDLW090408SR-D | 9,52 9,52 4,76 0,80 | 0,10 | ||||||||||||||
| Material Guide – Key to Recommended Inserts029486XDLW090408SR-DSC3025 | 9,52 9,52 4,76 0,80 | 0,10 | |||||||||||||||
| 029685 | X500 XDLT090408ER-D41 | 9,52 9,52 4,76 0,80 | 0,05 | ||||||||||||||
| Material Designation031535XDLT090408ER-D41SP6519 | 9,52 9,52 4,76 0,80 | 0,05 | |||||||||||||||
| 033067 | SC6525 XDLT090408ER-D41 | 9,52 9,52 4,76 0,80 | 0,05 | ||||||||||||||
| 029637 | GH2 XDLT090408ER-D721 | 9,52 9,52 4,76 0,80 | 0,04 | ||||||||||||||
| PH Stainless030853XDLT090412ER-D411KCast IronsX500 M Stainless Steels M P Alloyed Steels Unalloyed Steels P | N Aluminum & Alloys | S 9,52 9,52 4,76 1,20High Temp. Alloys0,05 | H | Hard Materials | |||||||||||||
| 030854 | SP6519 XDLT090412ER-D411 | 9,52 9,52 4,76 1,20 | 0,05 | ||||||||||||||
| Machining Choice: 1st Choice 2nd Choice 3rd Choice | Material Guide Key descriptions found on page A5. | |||||||||||||||||
| XDLW090408SR-D X500 should be used for Alloyed Steel and Stainless Steel with heavy scale. | |||||||||||||||||
| XDLT090412ER-D411 is a more positive geometry than the -D-41 with a larger radius which increases performance during | |||||||||||||||||
| smaller radial engagements or where chipping may occur when using the -D-41 geometry. | |||||||||||||||||
| Select the recommended Feed range 4 XDLT090412ER-D411 uses less power than the -D-41 geometry. |
according to the operation and the 7792VXD09 Feeds fz (mm/tooth) material to be machined. Alloyed Steel Gray Iron Spheroidal- Ductile Iron Hard Steel >1400 N/mm
Chilled Cast Iron >1400 N/mm
Example: 4 Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max.
| SR-D | X400 | Facing | 0,30 - 2,00 0,30 - 1,90 | - | - | - | - | - | - | - | - | - | - | - | 0,30 - 1,00 0,30 - 1,00 | ||
| Feed range for SR-D | X400 | Slotting | 0,30 - 1,50 0,30 - 1,45 | - | - | - | - | - | - | - | - | - | - | - | 0,30 - 0,60 0,30 - 0,80 | ||
| SR-D | X400 | Plunging | 0,10 - 0,25 0,10 - 0,23 | - | - | - | - | - | - | - | - | - | - | - | 0,10 - 0,12 0,10 - 0,12 | ||
| SR-D | X500 | Facing | - | 0,30 - 1,90 0,30 - 1,20 0,30 - 1,00 | - | - | - | - | - | - | - | - | - | - | - | ||
| XDLW090408SR-D X400 SR-D | X500 | Slotting | - | 0,30 - 1,40 0,30 - 0,90 0,30 - 0,80 | - | - | - | - | - | - | - | - | - | - | - | ||
| Alloyed Steel Facing SR-D | X500 | Plunging | - | 0,10 - 0,22 0,10 - 0,20 0,10 - 0,15 | - | - | - | - | - | - | - | - | - | - | - | ||
| in for SR-D | SC3025 | Facing | - | - | - | - | 0,30 - 2,00 0,30 - 1,80 0,30 - 1,50 | - | - | - | - | - | - | - | - | ||
| SR-D | SC3025 | Slotting | - | - | - | - | 0,30 - 1,70 0,30 - 1,50 0,30 - 1,30 | - | - | - | - | - | - | - | - | ||
| SR-D | SC3025 | Plunging | - | - | - | - | 0,10 - 0,25 0,10 - 0,22 0,10 - 0,20 | - | - | - | - | - | - | - | - | ||
| 0,30 – 1,90 mm/tooth ER-D41 | X500 | Facing | - | - | 0,20 - 1,00 0,20 - 0,80 | - | - | - | - | - | 0,20 - 0,60 0,20 - 0,60 0,20 - 0,60 0,20 - 0,80 | - | - | ||||
| ER-D41 | X500 | Slotting | - | - | 0,20 - 0,80 0,15 - 0,70 | - | - | - | - | - | 0,10 - 0,50 0,10 - 0,50 0,10 - 0,50 0,10 - 0,70 | - | - | ||||
| ER-D41 | X500 | Plunging | - | - | 0,10 - 0,16 0,08 - 0,12 | - | - | - | - | - | 0,05 - 0,08 0,05 - 0,08 0,05 - 0,08 0,05 - 0,10 | - | - | ||||
| ER-D41 SP6519 | Facing | 0,30 - 1,50 0,30 - 1,30 0,20 - 1,00 0,20 - 0,60 0,30 - 1,50 0,30 - 1,30 | - | - | - | 0,20 - 0,60 0,20 - 0,60 0,20 - 0,60 0,20 - 0,80 | - | - | |||||||||
| ER-D41 SP6519 | Slotting | 0,30 - 1,30 0,30 - 1,00 0,20 - 0,80 0,15 - 0,50 0,30 - 1,30 0,30 - 1,00 | - | - | - | 0,10 - 0,50 0,10 - 0,50 0,10 - 0,50 0,10 - 0,70 | - | - | |||||||||
| ER-D41 SP6519 | Plunging | 0,10 - 0,20 0,10 - 0,16 0,10 - 0,16 0,05 - 0,08 0,10 - 0,20 0,10 - 0,16 | - | - | - | 0,05 - 0,08 0,05 - 0,08 0,05 - 0,08 0,05 - 0,10 | - | - | |||||||||
| ER-D41 SC6525 | Facing | 0,30 - 1,45 0,30 - 1,30 | - | - | 0,30 - 1,50 0,30 - 1,30 | - | - | - | - | - | - | - | - | - | |||
| ER-D41 SC6525 | Slotting | 0,30 - 1,25 0,30 - 1,00 | - | - | 0,30 - 1,30 0,30 - 1,00 | - | - | - | - | - | - | - | - | - | |||
| ER-D41 SC6525 | Plunging | 0,10 - 0,18 0,10 - 0,16 | - | - | 0,10 - 0,20 0,10 - 0,16 | - | - | - | - | - | - | - | - | - | |||
| ER-D721 | GH2 | Facing | - | - | - | - | - | - | - | 0,30 - 1,50 0,30 - 1,30 | - | - | - | - | - | - | |
| ER-D721 | GH2 | Slotting | - | - | - | - | - | - | - | 0,30 - 1,30 0,30 - 1,00 | - | - | - | - | - | - | |
| ER-D721 | GH2 | Plunging | - | - | - | - | - | - | - | 0,10 - 0,20 0,10 - 0,16 | - | - | - | - | - | - | |
| ER-D411 X500 | Facing | - | - | 0,20 - 1,00 0,20 - 0,80 | - | - | - | - | - | 0,20 - 0,60 0,20 - 0,60 0,20 - 0,60 0,20 - 0,80 | - | - | |||||
| ER-D411 X500 | Slotting | - | - | 0,20 - 0,80 0,15 - 0,70 | - | - | - | - | - | 0,10 - 0,50 0,10 - 0,50 0,10 - 0,50 0,10 - 0,70 | - | - | |||||
| ER-D411 X500 | Plunging | - | - | 0,10 - 0,16 0,08 - 0,12 | - | - | - | - | - | 0,05 - 0,08 0,05 - 0,08 0,05 - 0,08 0,05 - 0,10 | - | - | |||||
| ER-D411 SP6519 | Facing | 0,30 - 1,50 0,30 - 1,30 0,20 - 1,00 0,20 - 0,60 0,30 - 1,50 0,30 - 1,30 | - | - | - | 0,20 - 0,60 0,20 - 0,60 0,20 - 0,60 0,20 - 0,80 | - | - | |||||||||
| ER-D411 SP6519 | Slotting | 0,30 - 1,30 0,30 - 1,00 0,20 - 0,80 0,15 - 0,50 0,30 - 1,30 0,30 - 1,00 | - | - | - | 0,10 - 0,50 0,10 - 0,50 0,10 - 0,50 0,10 - 0,70 | - | - | |||||||||
| ER-D411 SP6519 | Plunging | 0,10 - 0,20 0,10 - 0,16 0,10 - 0,16 0,05 - 0,08 0,10 - 0,20 0,10 - 0,16 | - | - | - | 0,05 - 0,08 0,05 - 0,08 0,05 - 0,08 0,05 - 0,10 | - | - |
Note: HTA = High Temperature Alloys Note: Speed recommendations can be found on page A72. www.kennametal.com A67