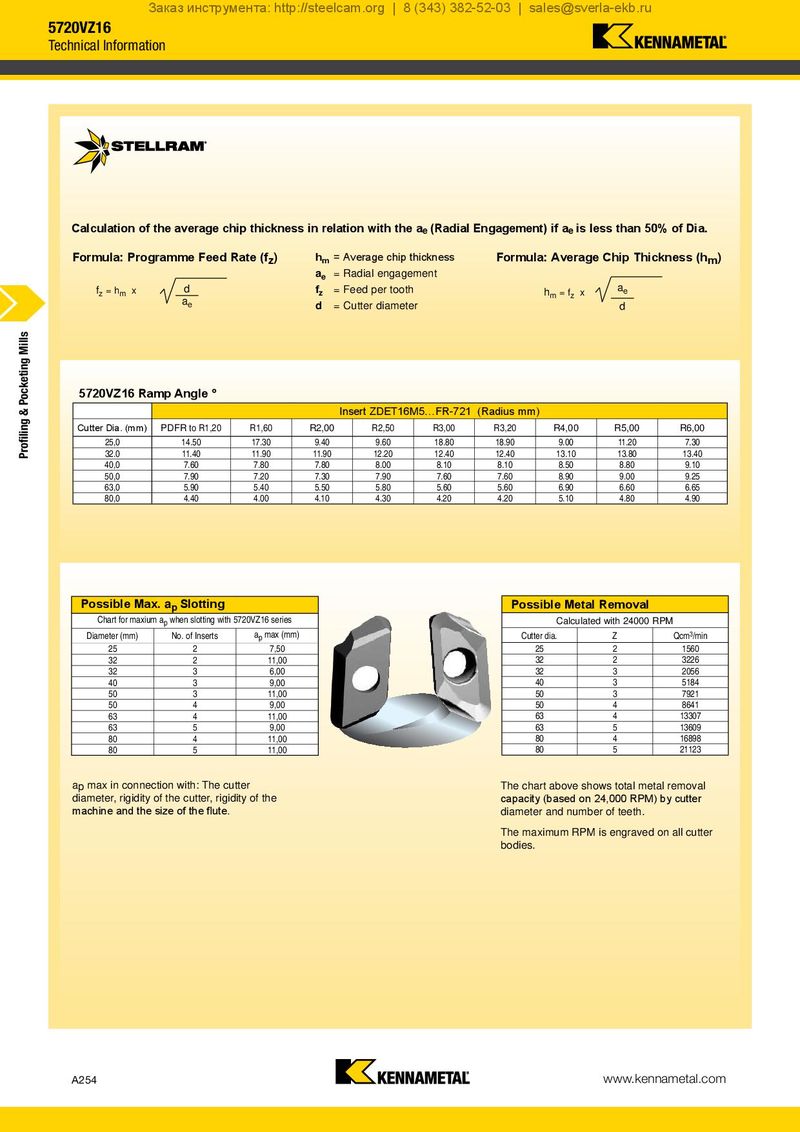
| Calculation of the average chip thickness in relation with the a | (Radial Engagement) if a | is less than 50% of Dia. |
| e | e |
| Formula: Programme Feed Rate (f ) | | h | = Average chip thickness | Formula: Average Chip Thickness (hm) |
| z | | m | |
| | a = Radial engagement | | |
| | | e | |
d f = Feed per tooth a
| f = h | x | | | h | = f x | | e |
| z | m | | z | | m | z | |
| | a | | | | | |
| | e | d = Cutter diameter | | | | d |
5720VZ16 Ramp Angle °
Insert ZDET16M5…FR-721 (Radius mm)
| Cutter Dia. (mm) | PDFR to R1,20 | R1,60 | R2,00 | R2,50 | R3,00 | R3,20 | R4,00 | R5,00 | R6,00 |
| 25,0 | 14.50 | 17.30 | 9.40 | 9.60 | 18.80 | 18.90 | 9.00 | 11.20 | 7.30 |
| 32.0 | 11.40 | 11.90 | 11.90 | 12.20 | 12.40 | 12.40 | 13.10 | 13.80 | 13.40 |
| 40,0 | 7.60 | 7.80 | 7.80 | 8.00 | 8.10 | 8.10 | 8.50 | 8.80 | 9.10 |
| 50,0 | 7.90 | 7.20 | 7.30 | 7.90 | 7.60 | 7.60 | 8.90 | 9.00 | 9.25 |
| 63,0 | 5.90 | 5.40 | 5.50 | 5.80 | 5.60 | 5.60 | 6.90 | 6.60 | 6.65 |
| 80,0 | 4.40 | 4.00 | 4.10 | 4.30 | 4.20 | 4.20 | 5.10 | 4.80 | 4.90 |
| Possible Max. a | | Slotting | | Possible Metal Removal | | | |
| | p | | | | | |
| Chart for maxium ap when slotting with 5720VZ16 series | | | | | | |
| | | | | Calculated with 24000 RPM | | |
| Diameter (mm) | No. of Inserts | ap max (mm) | Cutter dia. | | Z | Qcm 3/min |
| 25 | 2 | 7,50 | 25 | 2 | 1560 |
| 32 | 2 | 11,00 | 32 | 2 | 3226 |
| 32 | 3 | 6,00 | 32 | 3 | 2056 |
| 40 | 3 | 9,00 | 40 | 3 | 5184 |
| 50 | 3 | 11,00 | 50 | 3 | 7921 |
| 50 | 4 | 9,00 | 50 | 4 | 8641 |
| 63 | 4 | 11,00 | 63 | 4 | 13307 |
| 63 | 5 | 9,00 | 63 | 5 | 13609 |
| 80 | 4 | 11,00 | 80 | 4 | 16898 |
| 80 | 5 | 11,00 | 80 | 5 | 21123 |
ap max in connection with: The cutter The chart above shows total metal removal
diameter, rigidity of the cutter, rigidity of the capacity (based on 24,000 RPM) by cutter
machine and the size of the flute. diameter and number of teeth.
The maximum RPM is engraved on all cutter
bodies.
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы