Общий каталог SGS 2018 - страница 56
Навигация
 Каталог SGS шестизубые фрезы T-carb
 Каталог SGS микро инструмент 2021
 Каталог SGS фрезы для алюминия S-carb
 Каталог SGS высокопроизводительные черновые фрезы
 Каталог SGS инструмент для обработки алюминия
 Общий каталог SGS 2015 на русском
POS
4
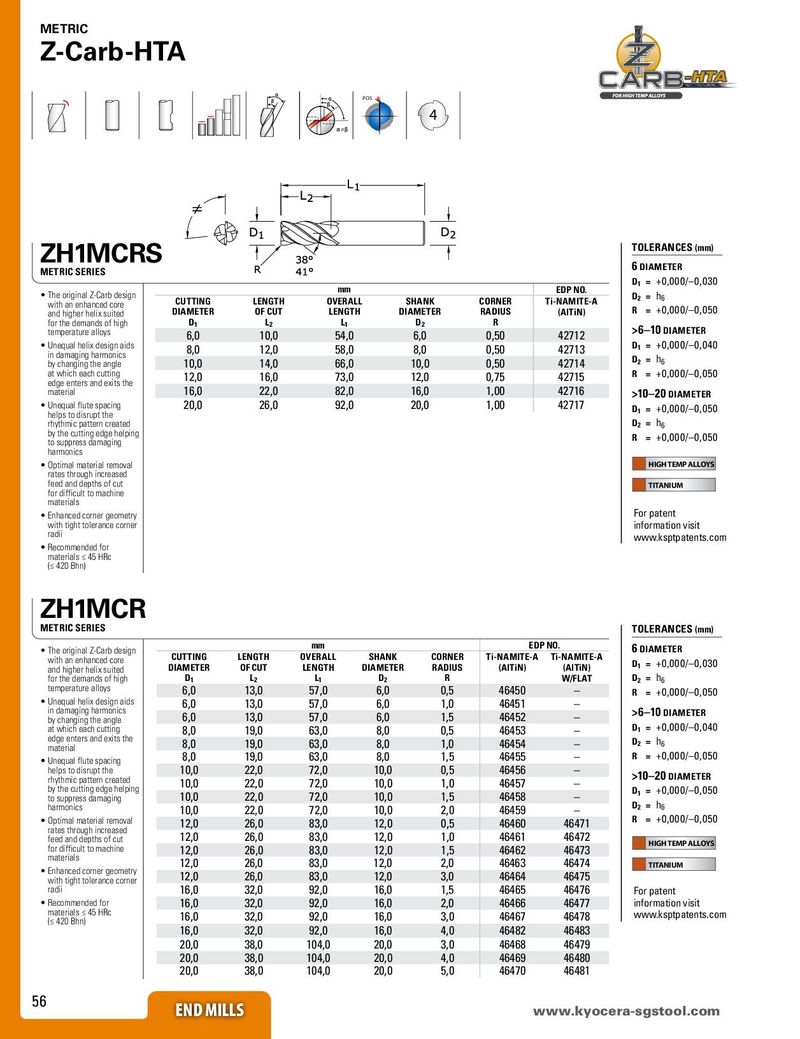
ZH1MCRS TOLERANCES (mm) 6 DIAMETER METRIC SERIES D = +0,000/–0,030
| • The oriinal Z-Carb desin | mm | EDP NO. | ||||
| g g with an enhanced core and higher helix suited | CUTTING DIAMETER | LENGTH OF CUT | OVERALL LENGTH | SHANK DIAMETER | CORNER RADIUS | Ti-NAMITE-A (AlTiN) |
| for the demands of high | D1 | L2 | L1 | D2 | R | |
| temperature alloys | 6,0 | 10,0 | 54,0 | 6,0 | 0,50 | 42712 |
| • Unequal helix design aids in damaging harmonics | 8,0 | 12,0 | 58,0 | 8,0 | 0,50 | 42713 |
| by changing the angle | 10,0 | 14,0 | 66,0 | 10,0 | 0,50 | 42714 |
| at which each cutting edge enters and exits the | 12,0 | 16,0 | 73,0 | 12,0 | 0,75 | 42715 |
| material | 16,0 | 22,0 | 82,0 | 16,0 | 1,00 | 42716 |
| • Unequal flute spacing | 20,0 | 26,0 | 92,0 | 20,0 | 1,00 | 42717 |
1
D 1 = helps to disrupt the rhythmic pattern created D = h 2 6
by the cutting edge helping R = +0,000/–0,050
to suppress damaging harmonics
- Optimal material removal HIGH TEMP ALLOYS rates through increased feed and depths of cut TITANIUM for difficult to machine materials
- Enhanced corner geometry For patent with tight tolerance corner information visit radii www.ksptpatents.com
- Recommended for materials ≤ 45 HRc (≤ 420 Bhn)
ZH1MCR
METRIC SERIES TOLERANCES (mm)
| • Th iil ZCb di | mm | EDP | NO. | ||||
| e orgna -ar esgn with an enhanced core and higher helix suited for the demands of high | CUTTING DIAMETER D1 | LENGTH OF CUT L2 | OVERALL LENGTH L1 | SHANK DIAMETER D2 | CORNER RADIUS R | Ti-NAMITE-A (AlTiN) | Ti-NAMITE-A (AlTiN) W/FLAT |
| temperature alloys | 6,0 | 13,0 | 57,0 | 6,0 | 0,5 | 46450 | – |
| • Unequal helix design aids i di hi | 6,0 | 13,0 | 57,0 | 6,0 | 1,0 | 46451 | – |
| n amagng armoncs by changing the angle | 6,0 | 13,0 | 57,0 | 6,0 | 1,5 | 46452 | – |
| at which each cutting | 8,0 | 19,0 | 63,0 | 8,0 | 0,5 | 46453 | – |
| edge enters and exits the material | 8,0 | 19,0 | 63,0 | 8,0 | 1,0 | 46454 | – |
| • Unequal flute spacing | 8,0 | 19,0 | 63,0 | 8,0 | 1,5 | 46455 | – |
| helps to disrupt the | 10,0 | 22,0 | 72,0 | 10,0 | 0,5 | 46456 | – |
| rhythmic pattern created by the cutting edge helping | 10,0 | 22,0 | 72,0 | 10,0 | 1,0 | 46457 | – |
| to suppress damaging | 10,0 | 22,0 | 72,0 | 10,0 | 1,5 | 46458 | – |
| harmonics | 10,0 | 22,0 | 72,0 | 10,0 | 2,0 | 46459 | – |
| • Optimal material removal rates throuh increased | 12,0 | 26,0 | 83,0 | 12,0 | 0,5 | 46460 | 46471 |
| g feed and depths of cut | 12,0 | 26,0 | 83,0 | 12,0 | 1,0 | 46461 | 46472 |
| for difficult to machine | 12,0 | 26,0 | 83,0 | 12,0 | 1,5 | 46462 | 46473 |
| materials | 12,0 | 26,0 | 83,0 | 12,0 | 2,0 | 46463 | 46474 |
| • Enhanced corner geometry with tight tolerance corner | 12,0 | 26,0 | 83,0 | 12,0 | 3,0 | 46464 | 46475 |
| radii | 16,0 | 32,0 | 92,0 | 16,0 | 1,5 | 46465 | 46476 |
| • Recommended for | 16,0 | 32,0 | 92,0 | 16,0 | 2,0 | 46466 | 46477 |
| materials ≤ 45 HRc (≤ 420 Bhn) | 16,0 | 32,0 | 92,0 | 16,0 | 3,0 | 46467 | 46478 |
| 16,0 | 32,0 | 92,0 | 16,0 | 4,0 | 46482 | 46483 | |
| 20,0 | 38,0 | 104,0 | 20,0 | 3,0 | 46468 | 46479 | |
| 20,0 | 38,0 | 104,0 | 20,0 | 4,0 | 46469 | 46480 | |
| 20,0 | 38,0 | 104,0 | 20,0 | 5,0 | 46470 | 46481 |
1
2 6