Общий каталог SGS 2018 - страница 46
Навигация
 Каталог SGS шестизубые фрезы T-carb
 Каталог SGS микро инструмент 2021
 Каталог SGS фрезы для алюминия S-carb
 Каталог SGS высокопроизводительные черновые фрезы
 Каталог SGS инструмент для обработки алюминия
 Общий каталог SGS 2015 на русском
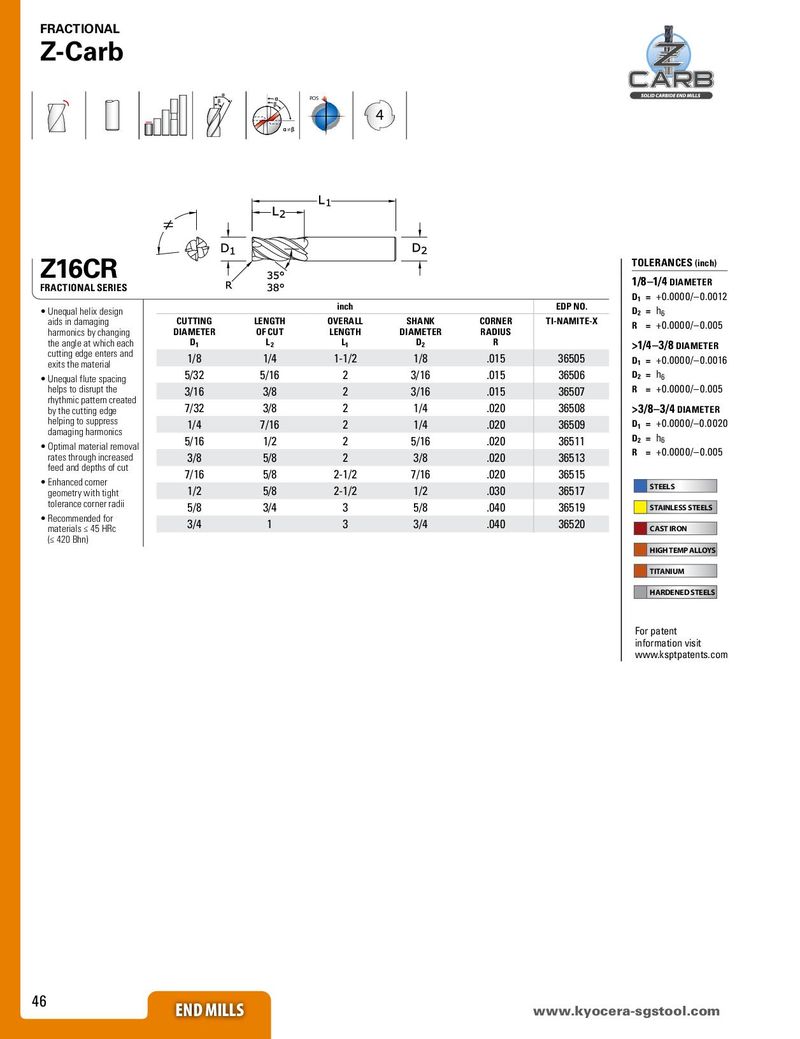
FRACTIONAL
Z-Carb
POS
4
≠
Z16CR TOLERANCES (inch)
1/8–1/4 DIAMETER
FRACTIONAL SERIES
D1 = +0.0000/–0.0012
inch EDP NO. D2 = h6
• Unequal helix design
aids in damaging CUTTING LENGTH OVERALL SHANK CORNER TI-NAMITE-X R = +0.0000/–0.005
harmonics by changing DIAMETER OF CUT LENGTH DIAMETER RADIUS
the angle at which each D1 L2 L1 D2 R >1/4–3/8 DIAMETER
cutting edge enters and
exits the material
1/8 1/4 1-1/2 1/8 .015 36505 D1 = +0.0000/–0.0016
• Unequal flute spacing 5/32 5/16 2 3/16 .015 36506 D2 = h6
helps to disrupt the 3/16 3/8 2 3/16 .015 36507 R = +0.0000/–0.005
rhythmic pattern created
by the cutting edge 7/32 3/8 2 1/4 .020 36508 >3/8–3/4 DIAMETER
helping to suppress 1/4 7/16 2 1/4 .020 36509 D1 = +0.0000/–0.0020
damaging harmonics
5/16 1/2 2 5/16 .020 36511 D2 = h6
• Optimal material removal
R = +0.0000/–0.005
rates through increased 3/8 5/8 2 3/8 .020 36513
feed and depths of cut
7/16 5/8 2-1/2 7/16 .020 36515
• Enhanced corner STEELS
geometry with tight 1/2 5/8 2-1/2 1/2 .030 36517
tolerance corner radii 5/8 3/4 3 5/8 .040 36519 STAINLESS STEELS
• Recommended for
materials ≤ 45 HRc 3/4 1 3 3/4 .040 36520 CAST IRON
(≤ 420 Bhn)
HIGH TEMP ALLOYS
TITANIUM
HARDENED STEELS
For patent
information visit
www.ksptpatents.com
46
END MILLS END MILLS
www.kyocera-sgstool.com