Общий каталог SGS 2018 - страница 47
Навигация
 Каталог SGS шестизубые фрезы T-carb
 Каталог SGS микро инструмент 2021
 Каталог SGS фрезы для алюминия S-carb
 Каталог SGS высокопроизводительные черновые фрезы
 Каталог SGS инструмент для обработки алюминия
 Общий каталог SGS 2015 на русском
POS
4
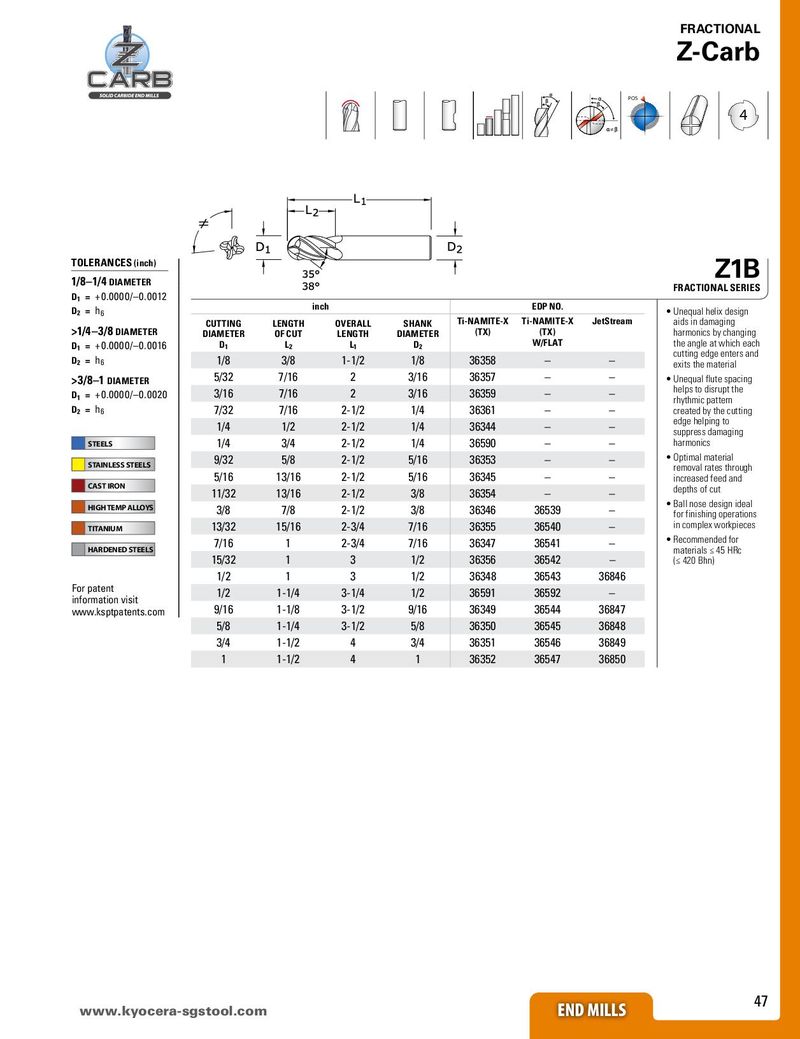
| TOLERANCES(inch) | Z1B | |||||||
| 1/8–1/4DIAMETER D1 = +0.0000/–0.0012 | FRACTIONAL SERIE | |||||||
| D2 =h6 | in | ch | EDP NO. | • Unequal helix design | ||||
| >1/4–3/8DIAMETER | CUTTING DIAMETER | LENGTH OF CUT | OVERALL LENGTH | SHANK DIAMETER | Ti-NAMITE-X (TX) | Ti-NAMITE-X (TX) | JetStream | aids in damaging harmonics by changing |
| D1 = +0.0000/–0.0016 | D1 | L2 | L1 | D2 | W/FLAT | the angle at which eac ttidt | ||
| D2 =h6 | 1/8 | 3/8 | 1-1/2 | 1/8 | 36358 | – | – | cung ege eners an exits the material |
| >3/8–1DIAMETER | 5/32 | 7/16 | 2 | 3/16 | 36357 | – | – | • Unequal flute spacing |
| D1 = +0.0000/–0.0020 | 3/16 | 7/16 | 2 | 3/16 | 36359 | – | – | helps to disrupt the rhythmic pattern |
| D2 =h6 | 7/32 | 7/16 | 2-1/2 | 1/4 | 36361 | – | – | created by the cutting |
| 1/4 | 1/2 | 2-1/2 | 1/4 | 36344 | – | – | edge helping to suppress damaging | |
| STEELS | 1/4 | 3/4 | 2-1/2 | 1/4 | 36590 | – | – | harmonics |
| STAINLESS STEELS | 9/32 | 5/8 | 2-1/2 | 5/16 | 36353 | – | – | • Optimal material removal rates through |
| 5/16 | 13/16 | 2-1/2 | 5/16 | 36345 | – | – | increased feed and | |
| CAST IRON | 11/32 | 13/16 | 2-1/2 | 3/8 | 36354 | – | – | depths of cut |
| HIGH TEMP ALLOYS | 3/8 | 7/8 | 2-1/2 | 3/8 | 36346 | 36539 | – | • Ball nose design ideal for finishing operation |
| TITANIUM | 13/32 | 15/16 | 2-3/4 | 7/16 | 36355 | 36540 | – | in complex workpieces |
| HARDENED STEELS | 7/16 | 1 | 2-3/4 | 7/16 | 36347 | 36541 | – | • Recommended for materials ≤ 45 HRc |
| 15/32 | 1 | 3 | 1/2 | 36356 | 36542 | – | (≤ 420 Bhn) | |
| 1/2 | 1 | 3 | 1/2 | 36348 | 36543 | 36846 | ||
| For patent information visit | 1/2 | 1-1/4 | 3-1/4 | 1/2 | 36591 | 36592 | – | |
| www.ksptpatents.com | 9/16 | 1-1/8 | 3-1/2 | 9/16 | 36349 | 36544 | 36847 | |
| 5/8 | 1-1/4 | 3-1/2 | 5/8 | 36350 | 36545 | 36848 | ||
| 3/4 | 1-1/2 | 4 | 3/4 | 36351 | 36546 | 36849 | ||
| 1 | 1-1/2 | 4 | 1 | 36352 | 36547 | 36850 |