Общий каталог SGS 2018 - страница 123
Навигация
 Каталог SGS шестизубые фрезы T-carb
 Каталог SGS микро инструмент 2021
 Каталог SGS фрезы для алюминия S-carb
 Каталог SGS высокопроизводительные черновые фрезы
 Каталог SGS инструмент для обработки алюминия
 Общий каталог SGS 2015 на русском
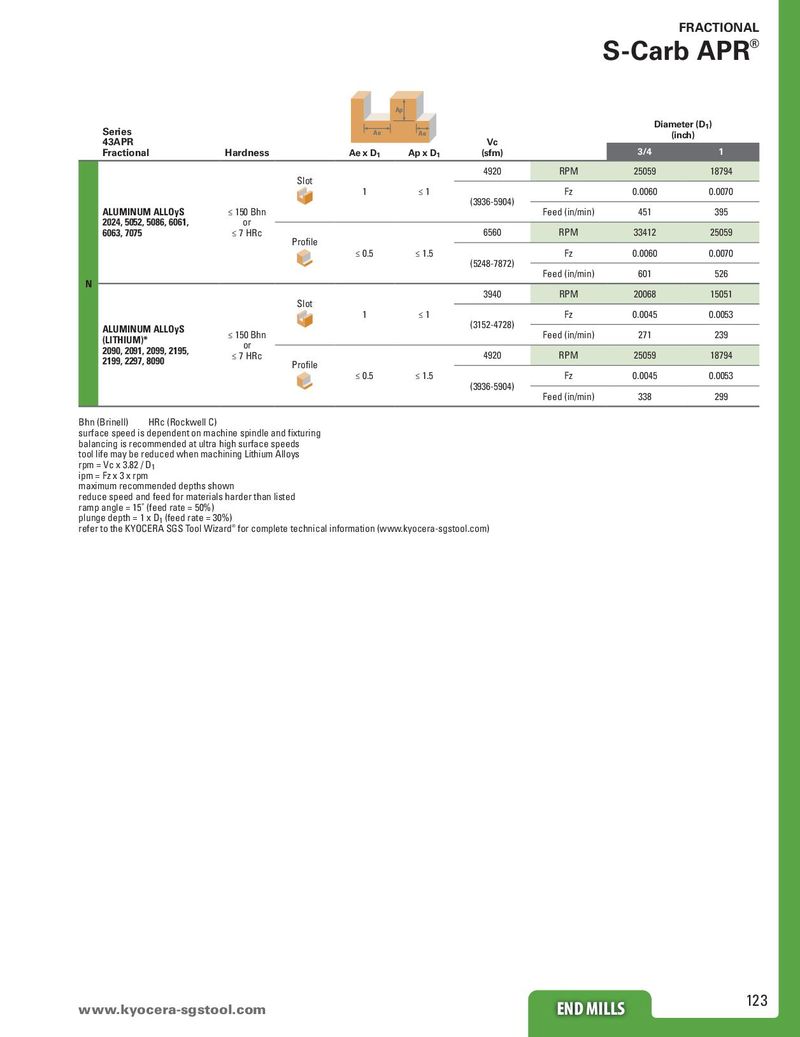
| Series 43APR | Ae | Ap Ae | Vc | Diame (in | ter (D1) ch) | |||
| Fractional | Hardness | Ae x D1 | Ap x D1 | (sfm) | 3/4 | 1 | ||
| Slot | 4920 | RPM | 25059 | 18794 | ||||
| 1 | ≤ 1 | (3936-5904) | Fz | 0.0060 | 0.0070 | |||
| ALUMINUM ALLOyS 2024 5052 5086 6061 | ≤ 150 Bhn or | Feed (in/min) | 451 | 395 | ||||
| , , , , 6063, 7075 | ≤ 7 HRc | Profile | 6560 | RPM | 33412 | 25059 | ||
| ≤ 0.5 | ≤ 1.5 | (5248-7872) | Fz | 0.0060 | 0.0070 | |||
| N | Feed (in/min) | 601 | 526 | |||||
| Slot | 3940 | RPM | 20068 | 15051 | ||||
| 1 | ≤ 1 | 31524728 | Fz | 0.0045 | 0.0053 | |||
| ALUMINUM ALLOyS (LITHIUM) | ≤ 150 Bhn | (-) | Feed (in/min) | 271 | 239 | |||
| 2090, 2091, 2099, 2195, 2199, 2297, 8090 | or ≤ 7 HRc | Profile | 4920 | RPM | 25059 | 18794 | ||
| ≤ 0.5 | ≤ 1.5 | (39365904) | Fz | 0.0045 | 0.0053 | |||
| - | Feed (in/min) | 338 | 299 |
Bhn (Brinell) HRc (Rockwell C) surface speed is dependent on machine spindle and fixturing balancing is recommended at ultra high surface speeds tool life may be reduced when machining Lithium Alloys rpm = Vc x 3.82 / D 1 ipm = Fz x 3 x rpm maximum recommended depths shown reduce speed and feed for materials harder than listed ramp angle = 15˚ (feed rate = 50%) plunge depth = 1 x D (feed rate = 30%) 1 refer to the KYOCERA SGS Tool Wizard® for complete technical information (www.kyocera-sgstool.com)