Каталог SGS монолитный инструмент из композитных материалов - страница 18
Навигация
 Каталог SGS микро инструмент 2021
 Каталог SGS микроинструмент
 Общий каталог SGS 2021
 Общий каталог SGS 2015 на русском
 Каталог SGS фрезы для обработки пластика PCR series
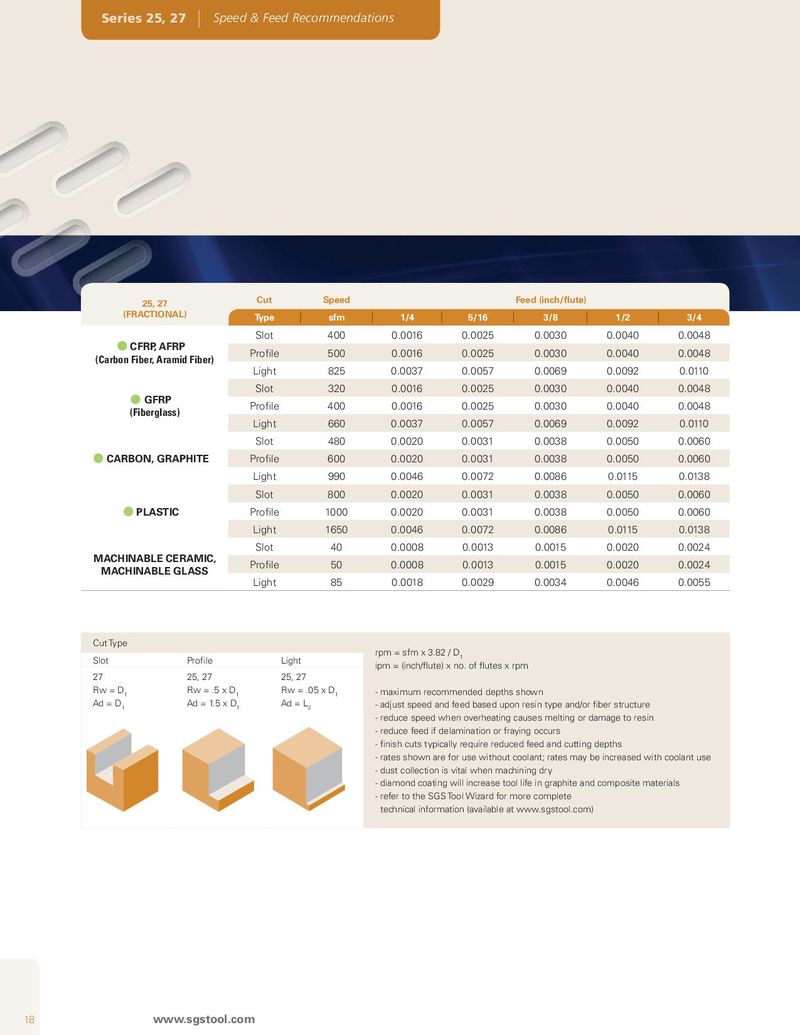
| 25, 27 | Cut | Speed | Feed (inch/flute) | ||||
| (FRACTIONAL) | Type | sfm | 1/4 | 5/16 | 3/8 | 1/2 | 3/4 |
| Slot | 400 | 0.0016 | 0.0025 | 0.0030 | 0.0040 | 0.0048 | |
| CFRP, AFRP (Carbon Fiber Aramid Fiber) | Profile | 500 | 0.0016 | 0.0025 | 0.0030 | 0.0040 | 0.0048 |
| , | Light | 825 | 0.0037 | 0.0057 | 0.0069 | 0.0092 | 0.0110 |
| Slot | 320 | 0.0016 | 0.0025 | 0.0030 | 0.0040 | 0.0048 | |
| GFRP (Fiberlass) | Profile | 400 | 0.0016 | 0.0025 | 0.0030 | 0.0040 | 0.0048 |
| g | Light | 660 | 0.0037 | 0.0057 | 0.0069 | 0.0092 | 0.0110 |
| Slot | 480 | 0.0020 | 0.0031 | 0.0038 | 0.0050 | 0.0060 | |
| CARBON, GRAPHITE | Profile | 600 | 0.0020 | 0.0031 | 0.0038 | 0.0050 | 0.0060 |
| Light | 990 | 0.0046 | 0.0072 | 0.0086 | 0.0115 | 0.0138 | |
| Slot | 800 | 0.0020 | 0.0031 | 0.0038 | 0.0050 | 0.0060 | |
| PLASTIC | Profile | 1000 | 0.0020 | 0.0031 | 0.0038 | 0.0050 | 0.0060 |
| Light | 1650 | 0.0046 | 0.0072 | 0.0086 | 0.0115 | 0.0138 | |
| Slot | 40 | 0.0008 | 0.0013 | 0.0015 | 0.0020 | 0.0024 | |
| MACHINABLE CERAMIC, MACHINABLE GLASS | Profile | 50 | 0.0008 | 0.0013 | 0.0015 | 0.0020 | 0.0024 |
| Light | 85 | 0.0018 | 0.0029 | 0.0034 | 0.0046 | 0.0055 |
| Cut Type | ||
| Slot | Profile | Light |
| 27 | 25, 27 | 25, 27 |
| Rw = D1 | Rw = .5 x D1 | Rw = .05 x D1 |
| Ad = D1 | Ad = 1.5 x D1 | Ad = L2 |
rpm = sfm x 3.82 / D ipm = (inch/flute) x no. of flutes x rpm
- reduce speed when overheating causes melting or damage to resin - reduce feed if delamination or fraying occurs - finish cuts typically require reduced feed and cutting depths - rates shown are for use without coolant; rates may be increased with coolant use - dust collection is vital when machining dry - diamond coating will increase tool life in graphite and composite materials - refer to the SGS Tool Wizard for more complete technical information (available at www.sgstool.com)