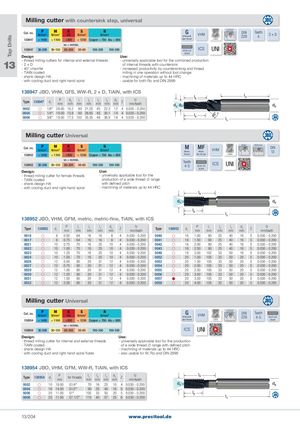
Milling cutter with countersink step, universal
P M K S N G G. Whitworth
Cat. no. pipe thread DIN Teeth
| N/mm | N/mm | HB | N/mm | N/mm | VHM | 2 × D 55° |
| | | | | Whitworth | | |
| 138947 | < 1400 | < 1100 | <300 | < 1250 Copper < 700 Alu < 600 | pipe thread | | coated |
| | | vc = m/min. | | | | UNI |
| | | | | | ICS | |
| 138947 | 30-200 | 30-120 | 80-200 | 30-80 | 100-350 100-350 6535 HA | | |
| | | | | shank | | |
| Design | | | | | Use: | | |
| 13 - thread milling cutters for internal and external threads | - universally applicable tool for the combined production |
| - 2 × D | of internal threads with countersink |
| - 45° chamfer | - increased productivity by countersinking and thread |
| - TiAIN coated | milling in one operation without tool change |
| - shank design HA | - machining of materials up to 44 HRC |
| - with cooling duct and right-hand spiral | - usable for both Rp and DIN 2999 |
| 138947 JBO, VHM, GFS, WW-R, 2 × D, TiAlN, with ICS | |
| Type | 138947 | | P d | l | l l | l | fz d | |
| | | d | 3 | 1 | 2 3 | 5 | 2 | |
| | | 1 | mm mm | mm | mm mm | mm | mm/tooth mm Z | |
| 0002 | | 1/8" 28�00 10�2 | | 80 21�25 45 22�3 12 4 0�020 - 0�200 | | | | |
| 0004 | | 1/4" 19�00 13�8 | | 90 28�65 45 30�1 14 4 0�020 - 0�200 | | | | |
| 0006 | | 3/8" 19�00 17�5 102 35�35 48 36�9 18 4 0�020 - 0�200 | | | | | | |
| Milling cutter Universal | | | | | | | | |
| | P | M | K | S | | N | M | DIN Metric fine Metric MF |
| Cat. no. | | | | | | | | 60° 60° VHM |
| | N/mm2 | N/mm2 | HB | N/mm2 | N/mm2 | | | 13 |
| | | | | | | | Metric | Metric |
| 138952 | < 1400 | < 1100 | <300 | < 1250 Copper < 700 Alu < 600 | | | thread | coated fine thread |
| | | | vc = m/min. | | | | Teeth | UNI |
| | | | | | | | | ICS |
| 138952 | 30-200 | 30-120 | 80-200 | 30-80 | 100-350 | 100-350 | 4-5 | 6535 HA |
| | | | | | | | | shank |
| Design: | | | | | | Use: | | | |
| - thread milling cutter for female threads | | | | | | - universally applicable tool for the | | | |
| - TiAIN coated | | | | | | production of a wide thread x range | | | |
| - shank design HA | | | | | | with defined pitch | | | |
| - with cooling duct and right-hand spiral | | | | | | - machining of materials up to 44 HRC | | | |
138952 JBO, VHM, GFM, metric, metric-fine, TiAlN, with ICS
| | | | P | l | | l l | | d | | | fz | | | P | l | l | l |
| Type | 138952 | | d | | 1 | | 2 | 4 | 2 | Z | | Type | 138952 | d | | 1 | 2 | 4 |
| | | 1 | mm | mm | mm | mm | | mm | | | mm/tooth | | 1 | mm | mm | mm | mm |
| 0016 | | | 8 0�50 | | 64 | 16 | 16 | | 8 | 4 | 0�030 - 0�200 | 0040 | | 16 | 1�00 | 90 | 25 | 40 |
| 0017 | | | 8 0�75 | | 64 | 16 | 16 | | 8 | 4 | 0�030 - 0�200 | 0041 | | 16 | 1�50 | 90 | 25 | 40 |
| 0021 | | 10 | 0�75 | | 70 | 16 | 25 | | 10 | 4 | 0�030 - 0�200 | 0042 | | 16 | 2�00 | 90 | 25 | 40 |
| 0022 | | 10 | 1�00 | | 70 | 16 | 25 | | 10 | 4 | 0�030 - 0�200 | 0043 | | 16 | 2�50 | 90 | 25 | 40 |
| 0023 | | 10 | 1�25 | | 70 | 16 | 25 | | 10 | 4 | 0�030 - 0�200 | 0048 | | 18 | 3�00 | 102 | 33 | 50 |
| 0024 | | 10 | 1�50 | | 70 | 16 | 25 | | 10 | 4 | 0�030 - 0�200 | 0052 | | 20 | 1�00 | 105 | 33 | 50 |
| 0026 | | 12 | 0�50 | | 80 | 20 | 31 | | 12 | 4 | 0�030 - 0�200 | 0053 | | 20 | 1�50 | 105 | 33 | 50 |
| 0027 | | 12 | 0�75 | | 80 | 20 | 31 | | 12 | 4 | 0�030 - 0�200 | 0054 | | 20 | 2�00 | 105 | 33 | 50 |
| 0029 | | 12 | 1�00 | | 80 | 20 | 31 | | 12 | 4 | 0�030 - 0�200 | 0055 | | 20 | 2�50 | 105 | 33 | 50 |
| 0030 | | 12 | 1�25 | | 80 | 20 | 31 | | 12 | 4 | 0�030 - 0�200 | 0056 | | 20 | 3�00 | 105 | 33 | 50 |
| 0031 | | 12 | 1�50 | | 80 | 20 | 31 | | 12 | 4 | 0�030 - 0�200 | 0057 | | 20 | 3�50 | 105 | 33 | 50 |
| 0032 | | 12 | 2�00 | | 80 | 20 | 31 | | 12 | 4 | 0�030 - 0�200 | 0058 | | 20 | 4�00 | 105 | 33 | 50 |
| Milling cutter Universal | | | | | | | | | | | | | | | | | | |
| P | M | | K | S | | | N | | | | | | G | | | | G. Whitworth |
| Cat. no. | | | | | | | | | | | | | | | | | | pipe thread |
| N/mm2 | N/mm2 | | HB | N/mm2 | | | N/mm2 | | | | | | | VHM | | | 55° |
| | | | | | | | | | | | | | Whitworth | | | | |
| 138954 | < 1400 | < 1100 | | <300 | < 1250 Copper < 700 Alu < 600 | | | | | | | | | pipe thread | | | coated | |
| | | vc = m/min. | | | | | | | | | | | | UNI | | | |
| | | | | | | | | | | | | | ICS | | | | |
| 138954 | 30-200 | 30-120 | | 80-200 | 30-80 | | 100-350 | | 100-350 | | | | | | | | | |
| Design: | | | | | | | | | | Use: | | | | | | | | |
| - thread milling cutter for internal and external threads | | | | | | | | | | - universally applicable tool for the production | | | | | | | | |
| - TiAIN coated | | | | | | | | | | of a wide thread x range with defined pitch | | | | | | | | |
| - shank design HA | | | | | | | | | | - machining of materials up to 44 HRC | | | | | | | | |
| - with cooling duct and right hand spiral flutes | | | | | | | | | | - also usable for W, Rp and DIN 2999 | | | | | | | | |
| 138954 JBO, VHM, GFM, WW-R, TiAlN, with ICS | | | | | | | | | | | | | | | | | | |
| Type | 138954 | | P | | | l | l | | l d | | | fz | | | | | | |
| | d | | for threads | | | 1 2 | | 4 | 2 | | | | | | | | |
| | 1 | mm | | | mm | mm | mm | mm Z | | mm/tooth | | | | | | | |
| 0002 | | 10 19�00 | | G1/4" | | 70 | 16 | 25 | 10 | 4 0�030 - 0�200 | | | | | | | | |
| 0004 | | 16 14�00 | | G1/2" | | 90 | 25 | 40 | 16 | 5 0�030 - 0�200 | | | | | | | | |
| 0006 | | 20 11�00 | | G1" | | 105 | 33 | 50 | 20 | 5 0�030 - 0�200 | | | | | | | | |
| 0008 | | 25 11�00 | | G1 1/2" | | 115 | 40 | 57 | 25 | 6 0�030 - 0�200 | | | | | | | | |
| d | | fz |
| 2 | Z | |
| mm | | mm/tooth |
| 16 | 5 | 0�030 - 0�200 |
| 16 | 5 | 0�030 - 0�200 |
| 16 | 5 | 0�030 - 0�200 |
| 16 | 5 | 0�030 - 0�200 |
| 18 | 5 | 0�030 - 0�200 |
| 20 | 5 | 0�030 - 0�200 |
| 20 | 5 | 0�030 - 0�200 |
| 20 | 5 | 0�030 - 0�200 |
| 20 | 5 | 0�030 - 0�200 |
| 20 | 5 | 0�030 - 0�200 |
| 20 | 5 | 0�030 - 0�200 |
| 20 | 5 | 0�030 - 0�200 |
| DIN | | Teeth |
| 228 | | 6535 HA 4-5 |
| | shank |