Общий каталог Osawa 2018 - страница 472
Навигация
 Общий каталог Osawa 2021
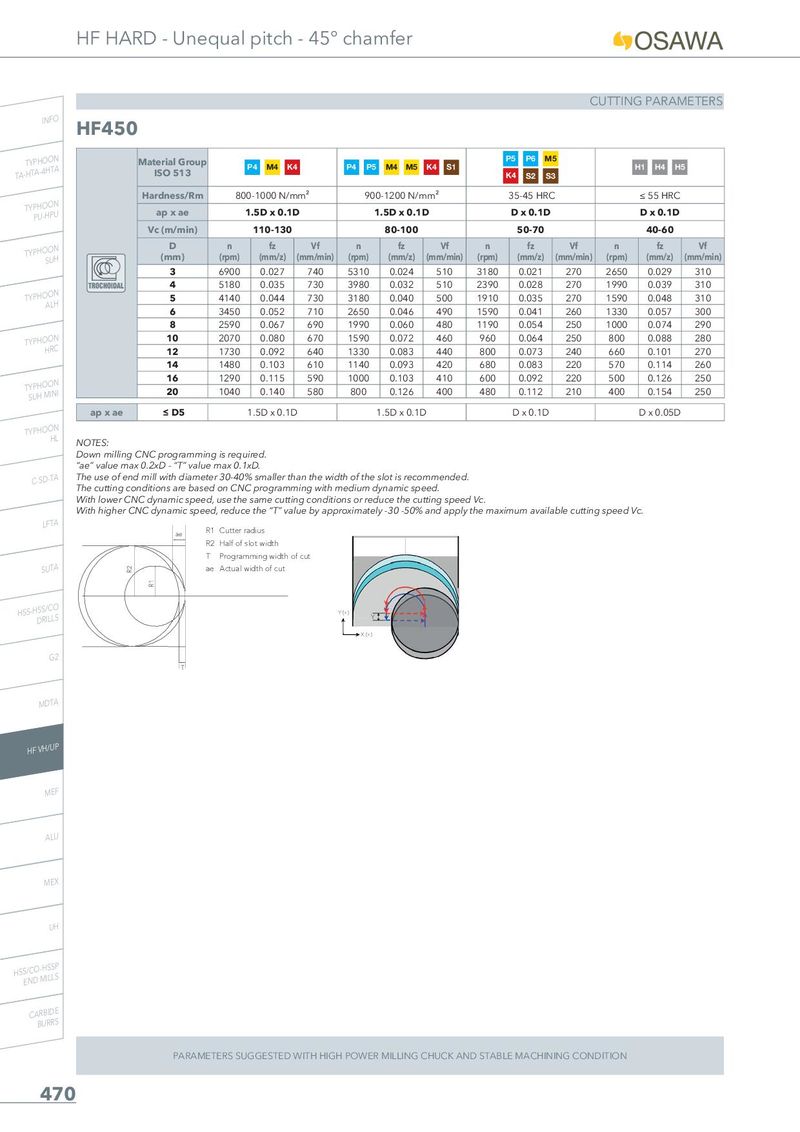
CUTTING PARAMETERS
INFO HF450
| Material Group ISO 513 | P4 M4 K | 4 | P4 P5 | M4 M5 | K4 S1 | P5 P6 M5 K4 S2 S3 | H1 H4 H | 5 | |||||
| Hardness/Rm | 80 | 0-1000 N/m | m² | 90 | 0-1200 N/m | m² | 35-45 HRC | ≤ 55 HRC | |||||
| ap x ae | 1 | .5D x 0.1 | D | 1 | .5D x 0.1 | D | D x 0.1D | D x 0.1D | |||||
| Vc (m/min) | 110-130 | 80-100 | 50-70 | 40-60 | |||||||||
| D | n | fz | Vf | n | fz | Vf | n | fz | Vf | n | fz | Vf | |
| (mm) | (rpm) | (mm/z) | (mm/min) | (rpm) | (mm/z) | (mm/min) | (rpm) | (mm/z) | (mm/min) | (rpm) | (mm/z) | (mm/min) | |
| 3 | 6900 | 0.027 | 740 | 5310 | 0.024 | 510 | 3180 | 0.021 | 270 | 2650 | 0.029 | 310 | |
| ROCHOIDAL | 4 | 5180 | 0.035 | 730 | 3980 | 0.032 | 510 | 2390 | 0.028 | 270 | 1990 | 0.039 | 310 |
| 5 | 4140 | 0.044 | 730 | 3180 | 0.040 | 500 | 1910 | 0.035 | 270 | 1590 | 0.048 | 310 | |
| 6 | 3450 | 0.052 | 710 | 2650 | 0.046 | 490 | 1590 | 0.041 | 260 | 1330 | 0.057 | 300 | |
| 8 | 2590 | 0.067 | 690 | 1990 | 0.060 | 480 | 1190 | 0.054 | 250 | 1000 | 0.074 | 290 | |
| 10 | 2070 | 0.080 | 670 | 1590 | 0.072 | 460 | 960 | 0.064 | 250 | 800 | 0.088 | 280 | |
| 12 | 1730 | 0.092 | 640 | 1330 | 0.083 | 440 | 800 | 0.073 | 240 | 660 | 0.101 | 270 | |
| 14 | 1480 | 0.103 | 610 | 1140 | 0.093 | 420 | 680 | 0.083 | 220 | 570 | 0.114 | 260 | |
| 16 | 1290 | 0.115 | 590 | 1000 | 0.103 | 410 | 600 | 0.092 | 220 | 500 | 0.126 | 250 | |
| 20 | 1040 | 0.140 | 580 | 800 | 0.126 | 400 | 480 | 0.112 | 210 | 400 | 0.154 | 250 | |
| ap x ae | ≤ D5 | 1.5D x 0.1D | 1.5D x 0.1D | D x 0.1D | D x 0.05D |
PU-HPU
SUH
ALH
TYPHOON
SUH MINI
TYPHOON HL NOTES: Down milling CNC programming is required. “ae” value max 0.2xD - “T” value max 0.1xD. The use of end mill with diameter 30-40% smaller than the width of the slot is recommended. C-SD-TA The cutting conditions are based on CNC programming with medium dynamic speed. With lower CNC dynamic speed, use the same cutting conditions or reduce the cutting speed Vc. With higher CNC dynamic speed, reduce the “T” value by approximately -30 -50% and apply the maximum available cutting speed Vc. LFTA R1 Cutter radius ae R2 Half of slot width T Programming width of cut SUTA ae Actual width of cut
HSS-HSS/CO DRILLS
G2
Y (+) Y X (+)
T
MDTA
HF VH/UP
MEF
ALU
MEX
UH
HSS/CO-HSSP END MILLS
CARBIDE