Общий каталог Lamina Technologies 2019 - 2020 - страница 185
Навигация
 Общий каталог Lamina Technologies 2017 - 2018
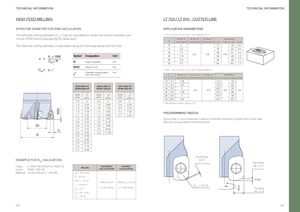
HIGH FEED MILLING LT 752 / LT 910 - CUTTER LINE
EFFECTIVE DIAMETER FOR RPM CALCULATION V x 1000 APPLICATION PARAMETERS
n = c π
The effective cutting diameter (D ) must be calculated to obtain the correct revolution per Dx eff LT 752 - SHOULDER MILLING - APKT 060204-PDTR minute (RPM) and consequently the table feed.eff
| D | α° max. for linear ramping | Ap max. for linear ramping | Ae max. for linear plunging | C min. | Helical P max. | Milling C max. | P max. | |
| 10 | 3 | 14 | 19 | 3.0 | ||||
| 12 | 2.2 | 18 | 23 | 2.5 | α° | |||
| 16 | 1.5 | 26 | 31 | 2.0 | ||||
| 20 | 1.15 | 5.2 | 0.6 | 34 | 0.9 | 39 | 1.8 | |
| 25 | 0.9 | 44 | 49 | 1.7 | ||||
| 32 | 0.7 | 58 | 63 | 1.7 |
eff
| n = | Vc x 1000 | Symbol | Designation | Unit |
| π x Deff | D | Cutter Diameter | mm | |
| Deff= | D -l | DOC | Depth of cut Diameter compensation (see chart below) | mm mm |
| D | D1 | α° max. for linear ramping | Ap max. for linear ramping | Ae max. for linear plunging | C min. | Helical P max. | Milling C max. | P max. |
| 10 | 4.7 | 1.25 | 14.7 | 18 | ||||
| 12 | 6.7 | 2.5 | 18.7 | 22 | ||||
| 16 | 10.7 | 2 | 26.7 | 30 | ||||
| 20 | 14.7 | 1.25 | 0.5 | 2.4 | 34.7 | 0.5 | 38 | 0.5 |
| 25 | 19.7 | 1 | 44.7 | 48 | ||||
| 32 | 26.7 | 0.9 | 58.7 | 62 |
| SDKX 0 SDKW 0 | 904-HF 904-HF | SDKX 1 SDKW 1 | 205-HF 205-HF | APKT 0 APKW 0 | 602-HF 602-HF |
| DOC (mm) | l (mm) | DOC (mm) | l (mm) | DOC (mm) | l (mm) |
| 1.5 | 0 | 2.0 | 0 | 0.5 | 0 |
| 1.4 | 0.22 | 1.8 | 0.66 | 0.4 | 0.32 |
| 1.3 | 0.58 | 1.6 | 1.58 | 0.3 | 0.72 |
| 1.2 | 1.04 | 1.4 | 2.58 | 0.2 | 1.28 |
| 1.1 | 1.52 | 1.2 | 3.66 | 0.1 | 2.22 |
| 1.0 | 2.02 | 1.0 | 4.84 | ||
| 0.9 | 2.54 | 0.8 | 6.16 | ||
| 0.8 | 3.10 | 0.6 | 7.66 | ||
| 0.7 | 3.70 | 0.4 | 9.44 | ||
| 0.6 | 4.34 | 0.2 | 11.76 | ||
| 0.5 | 5.06 | ||||
| 0.4 | 5.82 | ||||
| 0.3 | 6.72 | ||||
| 0.2 | 7.74 | ||||
| 0.1 | 9.06 |
(see chart below)
/2
D
Uncut Area
| EXAMPLE FOR D | CALCUATION | 0.22 | ||||
| eff | High Feed | |||||
| Cutter: LT 903 S-W-D040/4 (D=40/Z=4) | Ap = 0.5 | |||||
| INCORRECT | CORRECT | |||||
| VALUES |
| Insert: SDKX 1205-HF | CALCULCATION | CALCULATION | ||
| Material: Lamina Group 3 – 280 HB | Vc = 120 m/min | |||
| D = 40 mm | ||||
| DOC = 1.0 mm | ||||
| RPM for D=40 | RPM for D | =35.16 |
l = 4.84 mm eff R = R1.20
n = 954 rev/min n = 1085 rev/min prog RH
D = D - l Plunging
eff Ae = 2.4 D = 40 – 4.84 eff D = 35.16
eff