Общий каталог Lamina Technologies 2019 - 2020 - страница 180
Навигация
 Общий каталог Lamina Technologies 2017 - 2018
MACHINING RECOMMENDATIONS COOLANT GUIDE
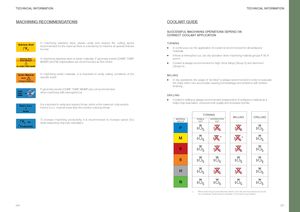
SUCCESSFUL MACHINING OPERATIONS DEPEND ON CORRECT COOLANT APPLICATION In machining stainless steel, please verify and respect the cutting speed TURNING
Stainless Steel recommended for the insert as there is a tendency to machine at speeds that are
V In continuous cut, the application of coolant is recommended for all workpiece C too low. materials.
- If there is interrupted cut, use dry operation when machining material groups P, M, K
| Stainless Steel | In machining stainless steel or exotic materials, P geometry inserts (CNMP, TNMP, | and H. | |
| Exotic Material | WNMP) and NX chipbreakers are recommended as first choice. | • |
Coolant is always recommended for High-Temp Alloys (Group S) and Aluminum NX-CNMP-TNMP-WNMP (Group N). Exotic Material In machining exotic materials, it is important to verify cutting conditions of the MILLING
specific insert.
Verify ! In dry operations, the usage of “air blow” is always recommended in order to evacuate
Cutting Conditions the chips which can accumulate causing tool breakage and problems with surface finishing. P geometry inserts (CNMP, TNMP, WNMP) are not recommended CNMP when machining with interrupted cut.
TNMP DRILLING WNMP
- Coolant in drilling is always recommended independent of workpiece material as it helps chip evacuation, improves hole quality and increases tool life.
Feed It is important to verify and respect Amax, which is the maximum chip section. x d.o.c. = Feed x d.o.c. must be lower than the number noted as Amax. Amax TURNING MILLING DRILLING
| V | To increase machining productivity, it is recommended to increase speed (Vc) | MATERIAL | STABLE | INTERRUPTED | |||
| while respecting chip size calculation. | GROUP | CUT | CUT | ||||
| C | |||||||
| Productivity | P |
M * *
K S H N
- When machining Duplex Stainless Steels, both wet and dry operations should be considered, depending on variables in the machining process.