Каталог Iscar вращающийся инструмент 2017 - страница 68
Навигация
 Каталог Iscar токарные пластины ISO 2022
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar решения для глубокого сверления
 Каталог Iscar полирующие фрезы
 Новые режущие инструменты Iscar 2026
 Каталог Iscar новые продукты 2018
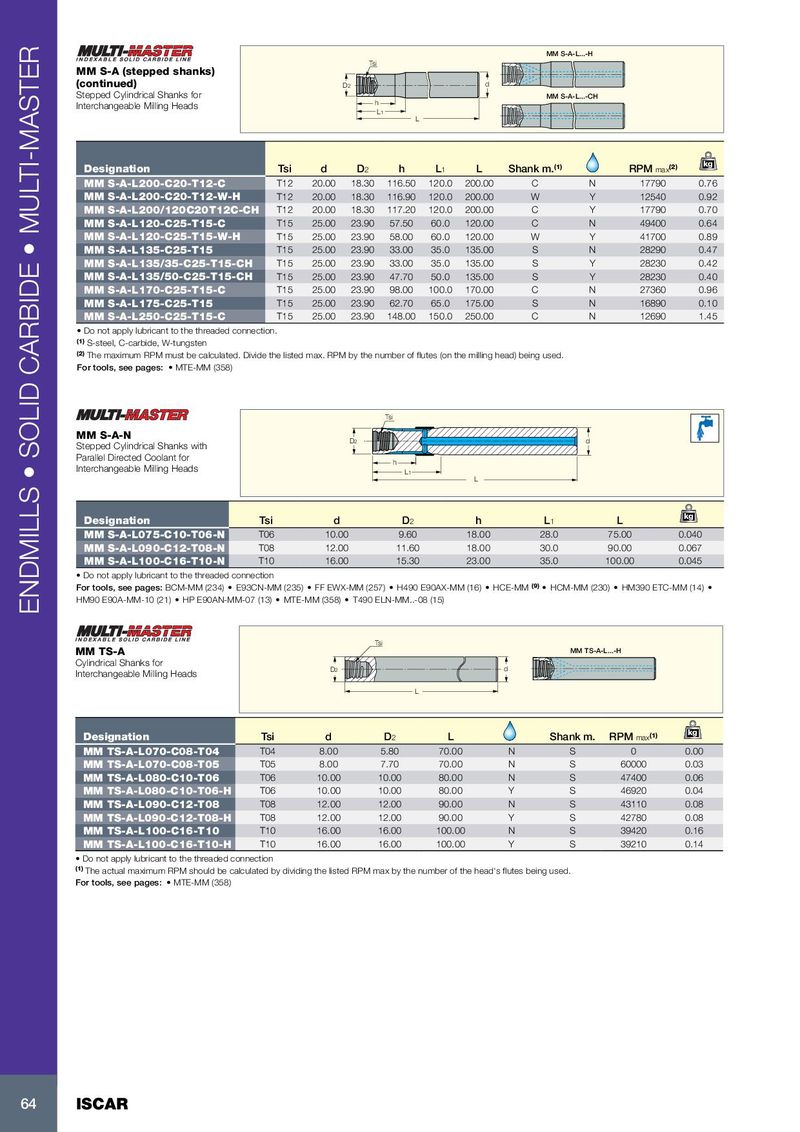
| MM S-A (stepped shanks) | Tsi | MM S-A-L...-H |
| (continued) | d D2 | |
| Stepped Cylindrical Shanks for | MM S-A-L...-CH | |
| Interchangeable Milling Heads | L1 L h |
| Designation | Tsi | d | D2 | h | L1 | L | Shank m.(1) | RPMmax(2) | kg | |
| MM S-A-L200-C20-T12-C | T12 | 20.00 | 18.30 | 116.50 | 120.0 | 200.00 | C | N | 17790 | 0.76 |
| MM S-A-L200-C20-T12-W-H | T12 | 20.00 | 18.30 | 116.90 | 120.0 | 200.00 | W | Y | 12540 | 0.92 |
| MM S-A-L200/120C20T12C-CH | T12 | 20.00 | 18.30 | 117.20 | 120.0 | 200.00 | C | Y | 17790 | 0.70 |
| MM S-A-L120-C25-T15-C | T15 | 25.00 | 23.90 | 57.50 | 60.0 | 120.00 | C | N | 49400 | 0.64 |
| MM S-A-L120-C25-T15-W-H | T15 | 25.00 | 23.90 | 58.00 | 60.0 | 120.00 | W | Y | 41700 | 0.89 |
| MM S-A-L135-C25-T15 | T15 | 25.00 | 23.90 | 33.00 | 35.0 | 135.00 | S | N | 28290 | 0.47 |
| MM S-A-L135/35-C25-T15-CH | T15 | 25.00 | 23.90 | 33.00 | 35.0 | 135.00 | S | Y | 28230 | 0.42 |
| MM S-A-L135/50-C25-T15-CH | T15 | 25.00 | 23.90 | 47.70 | 50.0 | 135.00 | S | Y | 28230 | 0.40 |
| MM S-A-L170-C25-T15-C | T15 | 25.00 | 23.90 | 98.00 | 100.0 | 170.00 | C | N | 27360 | 0.96 |
| MM S-A-L175-C25-T15 | T15 | 25.00 | 23.90 | 62.70 | 65.0 | 175.00 | S | N | 16890 | 0.10 |
| MM S-A-L250-C25-T15-C | T15 | 25.00 | 23.90 | 148.00 | 150.0 | 250.00 | C | N | 12690 | 1.45 |
- Do not apply lubricant to the threaded connection.
(1) S-steel, C-carbide, W-tungsten (2) The maximum RPM must be calculated. Divide the listed max. RPM by the number of flutes (on the milling head) being used. For tools, see pages: MTE-MM (358)
| Tsi | |||||||
| MM S-A-N Stepped Cylindrical Shanks with Parallel Directed Coolant for Interchangeable Milling Heads | D2 | h L1 | L | d | |||
| Designation | Tsi | d | D2 | h | L1 | L | kg |
| MM S-A-L075-C10-T06-N | T06 | 10.00 | 9.60 | 18.00 | 28.0 | 75.00 | 0.040 |
| MM S-A-L090-C12-T08-N | T08 | 12.00 | 11.60 | 18.00 | 30.0 | 90.00 | 0.067 |
| MM S-A-L100-C16-T10-N | T10 | 16.00 | 15.30 | 23.00 | 35.0 | 100.00 | 0.045 |
- Do not apply lubricant to the threaded connection
For tools, see pages: BCM-MM (234) E93CN-MM (235) FF EWX-MM (257) H490 E90AX-MM (16) HCE-MM (9) HCM-MM (230) HM390 ETC-MM (14) HM90 E90A-MM-10 (21) HP E90AN-MM-07 (13) MTE-MM (358) T490 ELN-MM..-08 (15)
| MM TS-A | Tsi | MM TS-A | -L...-H | |||||
| Cylindrical Shanks for Interchangeable Milling Heads | D2 | d | ||||||
| L | ||||||||
| Designation | Tsi | d | D2 | L | Shank m. | RPMmax(1) | kg | |
| MM TS-A-L070-C08-T04 | T04 | 8.00 | 5.80 | 70.00 | N | S | 0 | 0.00 |
| MM TS-A-L070-C08-T05 | T05 | 8.00 | 7.70 | 70.00 | N | S | 60000 | 0.03 |
| MM TS-A-L080-C10-T06 | T06 | 10.00 | 10.00 | 80.00 | N | S | 47400 | 0.06 |
| MM TS-A-L080-C10-T06-H | T06 | 10.00 | 10.00 | 80.00 | Y | S | 46920 | 0.04 |
| MM TS-A-L090-C12-T08 | T08 | 12.00 | 12.00 | 90.00 | N | S | 43110 | 0.08 |
| MM TS-A-L090-C12-T08-H | T08 | 12.00 | 12.00 | 90.00 | Y | S | 42780 | 0.08 |
| MM TS-A-L100-C16-T10 | T10 | 16.00 | 16.00 | 100.00 | N | S | 39420 | 0.16 |
| MM TS-A-L100-C16-T10-H | T10 | 16.00 | 16.00 | 100.00 | Y | S | 39210 | 0.14 |
- Do not apply lubricant to the threaded connection
(1) The actual maximum RPM should be calculated by dividing the listed RPM max by the number of the head's flutes being used. For tools, see pages: MTE-MM (358)