Каталог Iscar вращающийся инструмент 2017 - страница 279
Навигация
 Каталог Iscar токарные пластины ISO 2022
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar решения для глубокого сверления
 Каталог Iscar полирующие фрезы
 Новые режущие инструменты Iscar 2026
 Каталог Iscar новые продукты 2018
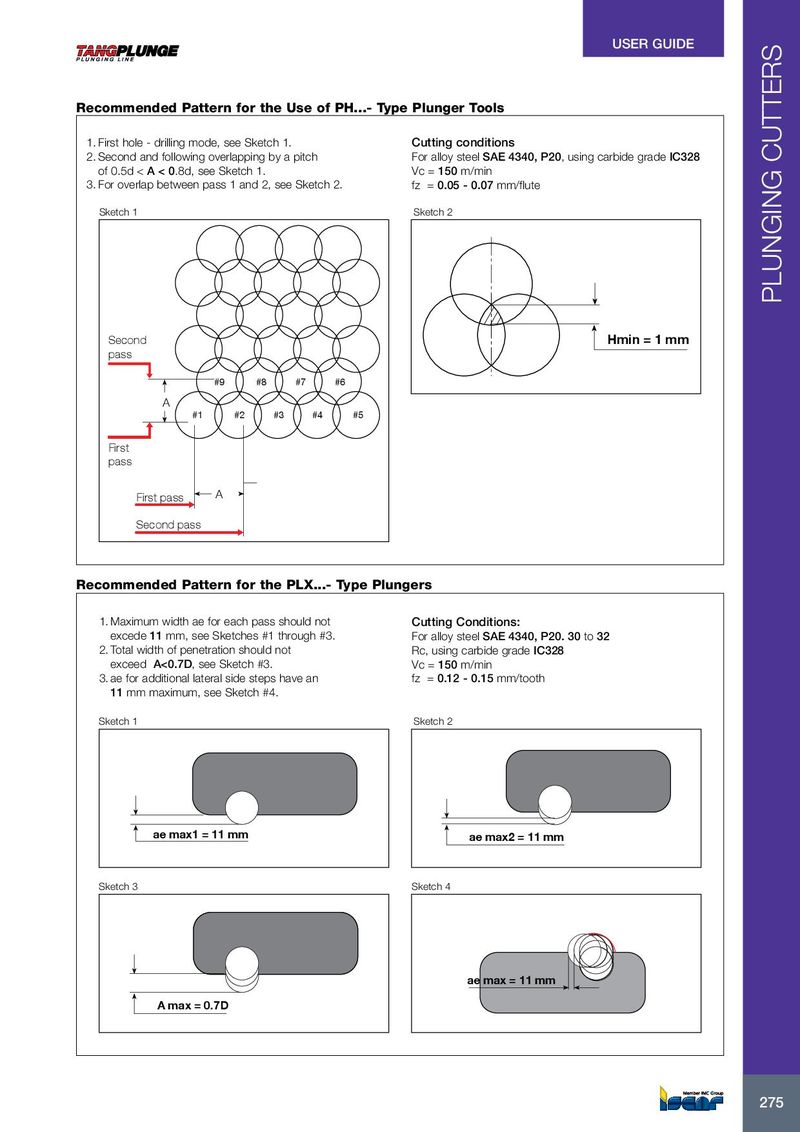
Recommended Pattern for the Use of PH...- Type Plunger Tools
| 1. First hole - drilling mode, see Sketch 1. | Cutting conditions | |
| 2. Second and following overlapping by a pitch | For alloy steel SAE 4340, P20, using carbide grade IC328 | |
| of 0.5d < A < 0.8d, see Sketch 1. | Vc = 150 m/min | |
| 3. For overlap between pass 1 and 2, see Sketch 2. | fz = 0.05 - 0.07 mm/flute | |
| Sketch 1 | Sketch 2 |
Second Hmin = 1 mm pass
| #9 | #8 | #7 | #6 | |
| A |
#1 #2 #3 #4 #5
First pass First pass A Second pass
Recommended Pattern for the PLX...- Type Plungers
| 1. Maximum width ae for each pass should not | Cutting Conditions: |
| excede 11 mm, see Sketches #1 through #3. | For alloy steel SAE 4340, P20. 30 to 32 |
| 2. Total width of penetration should not | Rc, using carbide grade IC328 |
| exceed A<0.7D, see Sketch #3. | Vc = 150 m/min |
| 3. ae for additional lateral side steps have an | fz = 0.12 - 0.15 mm/tooth |
| 11 mm maximum, see Sketch #4. | |
| Sketch 1 | Sketch 2 |
ae max1 = 11 mm ae max2 = 11 mm
Sketch 3 Sketch 4 Dt Di
ae max = 11 mm A max = 0.7D