Каталог Iscar вращающийся инструмент 2017 - страница 276
Навигация
 Каталог Iscar токарные пластины ISO 2022
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar решения для глубокого сверления
 Каталог Iscar полирующие фрезы
 Новые режущие инструменты Iscar 2026
 Каталог Iscar новые продукты 2018
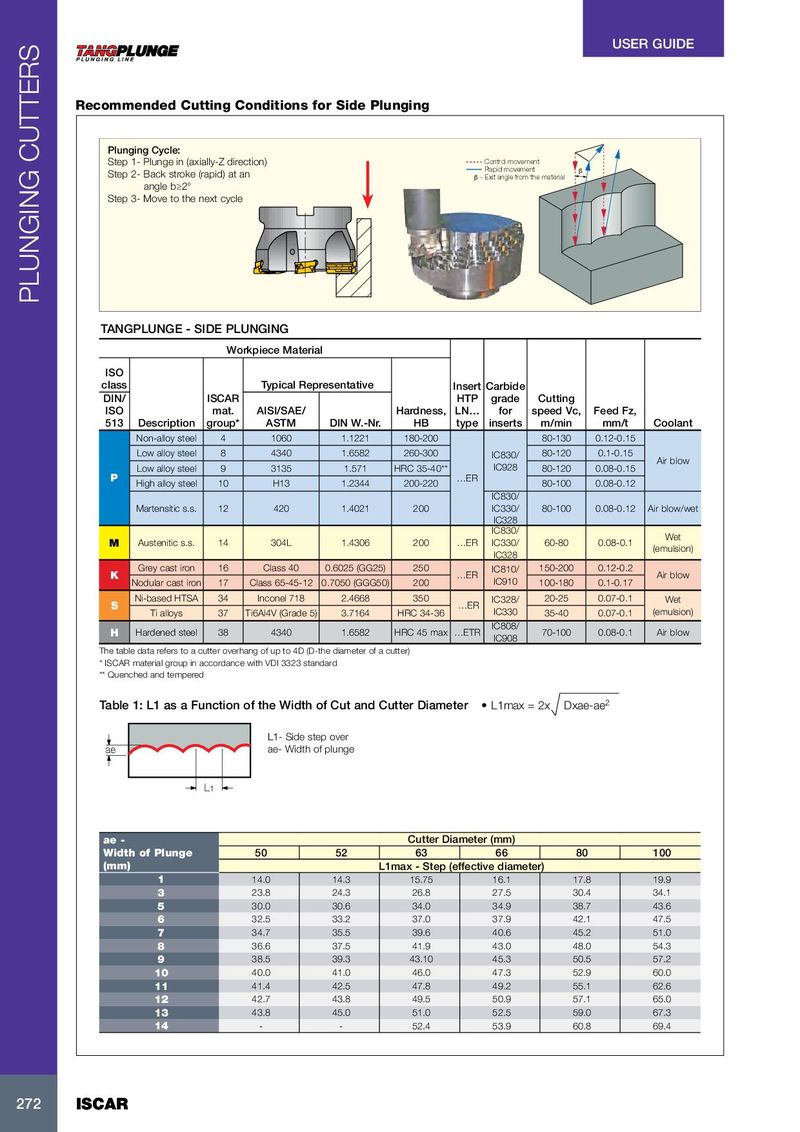
Recommended Cutting Conditions for Side Plunging
Plunging Cycle: Step 1- Plunge in (axially-Z direction) Control movement
Step 2- Back stroke (rapid) at an Rapid movement β
β - Exit angle from the material angle b≥2° Step 3- Move to the next cycle
TANGPLUNGE - SIDE PLUNGING
Workpiece Material
ISO
| class | Typical Representative | Insert Carbide | |||||||
| DIN/ | ISCAR | HTP | grade | Cutting | |||||
| ISO | mat. | AISI/SAE/ | Hardness, | LN… | for | speed Vc, | Feed Fz, | ||
| 513 | Description | group* | ASTM | DIN W.-Nr. | HB | type | inserts | m/min | Coolant mm/t |
| Non-alloy steel | 4 | 1060 | 1.1221 | 180-200 | 80-130 | 0.12-0.15 | |||
| Low alloy steel | 8 | 4340 | 1.6582 | 260-300 | IC830/ | 80-120 | 0.1-0.15 | ||
| Air blow | |||||||||
| Low alloy steel | 9 | 3135 | 1.571 | HRC 35-40** | IC928 | 80-120 | 0.08-0.15 | ||
| P | …ER | ||||||||
| High alloy steel | 10 | H13 | 1.2344 | 200-220 | 80-100 | 0.08-0.12 | |||
| IC830/ | |||||||||
| Martensitic s.s. | 12 | 420 | 1.4021 | 200 | IC330/ | 80-100 | Air blow/wet 0.08-0.12 | ||
| IC328 | |||||||||
| IC830/ | |||||||||
| M | Wet | ||||||||
| Austenitic s.s. | 14 | 304L | 1.4306 | 200 | …ER | IC330/ | 60-80 | 0.08-0.1 | |
| (emulsion) | |||||||||
| IC328 | |||||||||
| Grey cast iron | 16 | Class 40 | 0.6025 (GG25) | 250 | IC810/ | 150-200 | 0.12-0.2 | ||
| K | …ER | Air blow | |||||||
| Nodular cast iron | 17 | Class 65-45-12 0.7050 (GGG50) | 200 | IC910 | 100-180 | 0.1-0.17 | |||
| Ni-based HTSA | 34 | Inconel 718 | 2.4668 | 350 | IC328/ | 20-25 | Wet 0.07-0.1 | ||
| S | …ER | ||||||||
| Ti alloys 37 | Ti6Al4V (Grade 5) | 3.7164 | HRC 34-36 | IC330 | 35-40 | (emulsion) 0.07-0.1 | |||
| H | IC808/ | ||||||||
| Hardened steel | 38 | 4340 | 1.6582 | HRC 45 max …ETR | 70-100 | Air blow 0.08-0.1 |
IC908 The table data refers to a cutter overhang of up to 4D (D-the diameter of a cutter) * ISCAR material group in accordance with VDI 3323 standard ** Quenched and tempered
Table 1: L1 as a Function of the Width of Cut and Cutter Diameter • L1max = 2x Dxae-ae 2
L1- Side step over ae ae- Width of plunge
L1
| ae - | Cutter Dia | meter (mm) | ||||
| Width of Plunge | 50 | 52 | 63 | 66 | 80 | 100 |
| (mm) | L1max - Step (ef | fective diameter | ) | |||
| 1 | 14.0 | 14.3 | 15.75 | 16.1 | 17.8 | 19.9 |
| 3 | 23.8 | 24.3 | 26.8 | 27.5 | 30.4 | 34.1 |
| 5 | 30.0 | 30.6 | 34.0 | 34.9 | 38.7 | 43.6 |
| 6 | 32.5 | 33.2 | 37.0 | 37.9 | 42.1 | 47.5 |
| 7 | 34.7 | 35.5 | 39.6 | 40.6 | 45.2 | 51.0 |
| 8 | 36.6 | 37.5 | 41.9 | 43.0 | 48.0 | 54.3 |
| 9 | 38.5 | 39.3 | 43.10 | 45.3 | 50.5 | 57.2 |
| 10 | 40.0 | 41.0 | 46.0 | 47.3 | 52.9 | 60.0 |
| 11 | 41.4 | 42.5 | 47.8 | 49.2 | 55.1 | 62.6 |
| 12 | 42.7 | 43.8 | 49.5 | 50.9 | 57.1 | 65.0 |
| 13 | 43.8 | 45.0 | 51.0 | 52.5 | 59.0 | 67.3 |
| 14 | - | - | 52.4 | 53.9 | 60.8 | 69.4 |