Каталог Iscar вращающийся инструмент 2017 - страница 236
Навигация
 Каталог Iscar токарные пластины ISO 2022
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar решения для глубокого сверления
 Каталог Iscar полирующие фрезы
 Новые режущие инструменты Iscar 2026
 Каталог Iscar новые продукты 2018
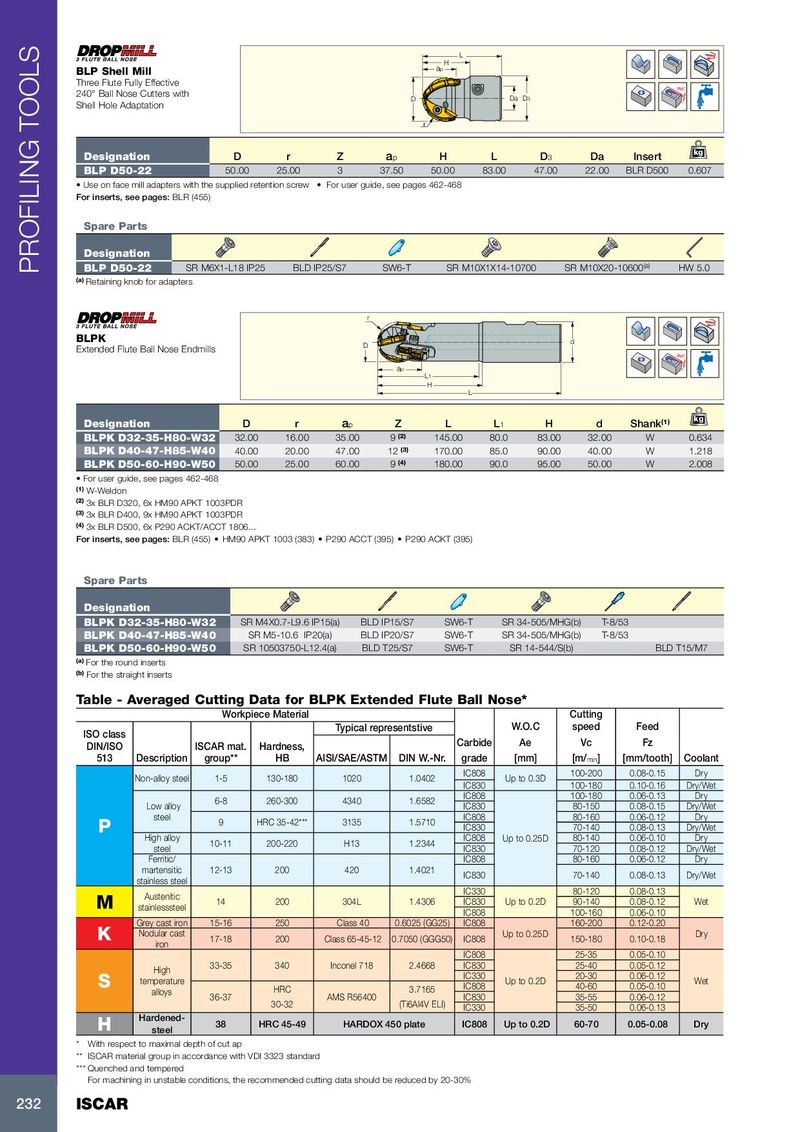
| BLP Shell Mill | ap L H | |||||||||
| Three Flute Fully Effective 240° Ball Nose Cutters with Shell Hole Adaptation | D r | D3 Da | Rd° | |||||||
| Designation | D | r | Z | ap H L | D3 | Da | Inse | rt | kg | |
| BLP D50-22 | 50.00 | 25.00 | 3 | 37.50 50.00 83.00 | 47.00 | 22.00 | BLR D | 500 | 0.607 |
- Use on face mill adapters with the supplied retention screw
- For user guide, see pages 462-468
For inserts, see pages: BLR (455)
| Spare Parts | ||||||
| Designation | ||||||
| BLP D50-22 | SR M6X1-L18 IP25 | BLD IP25/S7 | SW6-T | SR M10X1X14-10700 | SR M10X20-10600(a) | HW 5.0 |
(a) Retaining knob for adapters
| BLPK | D r | d | |||||||||
| Extended Flute Ball Nose Endmills | ap | L1 H L | Rd° | ||||||||
| Designation | D | r | ap | Z | L | L1 | H | d | Shan | k(1) | kg |
| BLPK D32-35-H80-W32 | 32.00 | 16.00 | 35.00 | 9(2) | 145.00 | 80.0 | 83.00 | 32.00 | W | 0.634 | |
| BLPK D40-47-H85-W40 | 40.00 | 20.00 | 47.00 | 12(3) | 170.00 | 85.0 | 90.00 | 40.00 | W | 1.218 | |
| BLPK D50-60-H90-W50 | 50.00 | 25.00 | 60.00 | 9(4) | 180.00 | 90.0 | 95.00 | 50.00 | W | 2.008 |
- For user guide, see pages 462-468
(1) W-Weldon (2) 3x BLR D320, 6x HM90 APKT 1003PDR (3) 3x BLR D400, 9x HM90 APKT 1003PDR (4) 3x BLR D500, 6x P290 ACKT/ACCT 1806... For inserts, see pages: BLR (455) HM90 APKT 1003 (383) P290 ACCT (395) P290 ACKT (395)
Spare Parts
| Designation | ||||||
| BLPK D32-35-H80-W32 | SR M4X0.7-L9.6 IP15(a) | BLD IP15/S7 | SW6-T | SR 34-505/MHG(b) | T-8/53 | |
| BLPK D40-47-H85-W40 | SR M5-10.6 IP20(a) | BLD IP20/S7 | SW6-T | SR 34-505/MHG(b) | T-8/53 | |
| BLPK D50-60-H90-W50 | SR 10503750-L12.4(a) | BLD T25/S7 | SW6-T | SR 14-544/S(b) | BLD T15/M7 |
(a) For the round inserts (b) For the straight inserts
Table - Averaged Cutting Data for BLPK Extended Flute Ball Nose*
| Workp | iece Material | Cutting | ||||||||
| ISO class | Typical repr | esentstive | W.O.C | speed | Feed | |||||
| DIN/ISO 513 | Description | ISCAR mat. group | Hardness, HB | AISI/SAE/ASTM | DIN W.-Nr. | Carbide grade | Ae [mm] | Vc [m/min] | Fz [mm/tooth] | Coolant |
| Non-alloy steel | 1-5 | 130-180 | 1020 | 1.0402 | IC808 | Up to 0.3D | 100-200 | 0.08-0.15 | Dry | |
| IC830 | 100-180 | 0.10-0.16 | Dry/Wet | |||||||
| 68 | 260300 | 4340 | 16582 | IC808 | 100-180 | 0.06-0.13 | Dry | |||
| Low alloy | - | - | . | IC830 | 80-150 | 0.08-0.15 | Dry/Wet | |||
| steel | 9 | HRC 35-42 | 3135 | 15710 | IC808 | 80-160 | 0.06-0.12 | Dry | ||
| P | . | IC830 | 70-140 | 0.08-0.13 | Dry/Wet | |||||
| High alloy steel | 10-11 | 200-220 | H13 | 1.2344 | IC808 IC830 | Up to 0.25D | 80-140 70-120 | 0.06-0.10 0.08-0.12 | Dry Dry/Wet | |
| Ferritic/ | IC808 | 80-160 | 0.06-0.12 | Dry | ||||||
| martensitic stainless steel | 12-13 | 200 | 420 | 1.4021 | IC830 | 70-140 | 0.08-0.13 | Dry/Wet | ||
| M | Austenitic stainlesssteel | 14 | 200 | 304L | 1.4306 | IC330 IC830 IC808 | Up to 0.2D | 80-120 90-140 100-160 | 0.08-0.13 0.08-0.12 0.06-0.10 | Wet |
| Grey cast iron | 15-16 | 250 | Class 40 | 0.6025 (GG25) | IC808 | 160-200 | 0.12-0.20 | |||
| K | Nodular cast iron | 17-18 | 200 | Class 65-45-12 | 0.7050 (GGG50) | IC808 | Up to 0.25D | 150-180 | 0.10-0.18 | Dry |
| Hih | 33-35 | 340 | Inconel 718 | 2.4668 | IC808 IC830 | 25-35 25-40 | 0.05-0.10 0.05-0.12 | |||
| g | IC330 | 20-30 | 0.06-0.12 | |||||||
| S | temperature | HRC | 37165 | IC808 | Up to 0.2D | 40-60 | 0.05-0.10 | Wet | ||
| alloys | 36-37 | AMS R56400 | . | IC830 | 35-55 | 0.06-0.12 | ||||
| 30-32 | (Ti6Al4V ELI) | IC330 | 35-50 | 0.06-0.13 | ||||||
| H | Hardened- steel | 38 | HRC 45-49 | HARDOX 4 | 50 plate | IC808 | Up to 0.2D | 60-70 | 0.05-0.08 | Dry |
* With respect to maximal depth of cut ap ** ISCAR material group in accordance with VDI 3323 standard *** Quenched and tempered For machining in unstable conditions, the recommended cutting data should be reduced by 20-30%