Каталог Iscar токарный инструмент 2017 - страница 347
Навигация
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar расточные системы 2022
 Каталог Iscar высокоточные развертки и метчики 2022
 Токарные инструменты Iscar (часть 2) 2026
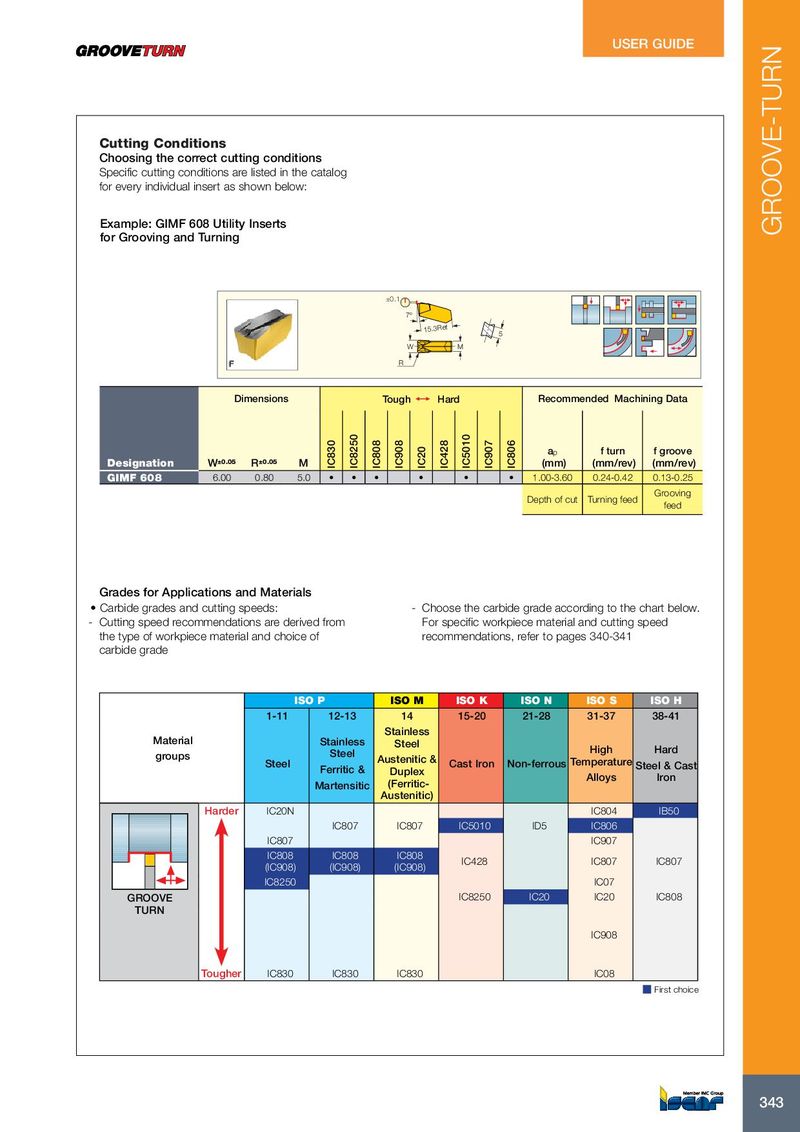
Cutting Conditions
Choosing the correct cutting conditions Specific cutting conditions are listed in the catalog for every individual insert as shown below: Example: GIMF 608 Utility Inserts for Grooving and Turning
±0.1 7º 15.3Ref 5 W M R
Dimensions Tough 1 Hard Recommended Machining Data
| ap | f turn | f groove | |||||||||||
| Designation | W±0.05 | R ±0.05 | M | (mm) | (mm/rev) | (mm/rev) | |||||||
| GIMF 608 | 6.00 | 0.80 | 5.0 | • | • | • | • | • | • | 1.00-3.60 | 0.24-0.42 | 0.13-0.25 |
Grooving Depth of cut Turning feed feed
Grades for Applications and Materials
- Carbide grades and cutting speeds: - Choose the carbide grade according to the chart below.
- Cutting speed recommendations are derived from For specific workpiece material and cutting speed the type of workpiece material and choice of recommendations, refer to pages 340-341 carbide grade
| IS | O P | ISO M | ISO K | ISO N | ISO S | ISO H | ||
| Material groups | 1-11 Steel | 12-13 Stainless Steel Ferritic & Martensitic | 14 Stainless Steel Austenitic & Duplex (Ferritic- Austenitic) | 15-20 Cast Iron | 21-28 Non-ferrous | 31-37 High Temperature Alloys | 38-41 Hard Steel & Cast Iron | |
| Harder | IC20N | IC804 | IB50 | |||||
| IC807 | IC807 | IC5010 | ID5 | IC806 | ||||
| IC807 | IC907 | |||||||
| IC808 (IC908) IC8250 | IC808 (IC908) | IC808 (IC908) | IC428 | IC807 IC07 | IC807 | |||
| GROOVE TURN | Tougher | IC830 | IC830 | IC830 | IC8250 | IC20 | IC20 IC908 IC08 | IC808 |
First choice