Каталог Iscar токарный инструмент 2017 - страница 314
Навигация
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar расточные системы 2022
 Каталог Iscar высокоточные развертки и метчики 2022
 Токарные инструменты Iscar (часть 2) 2026
GROOVE-TURN
Workpiece
22.0
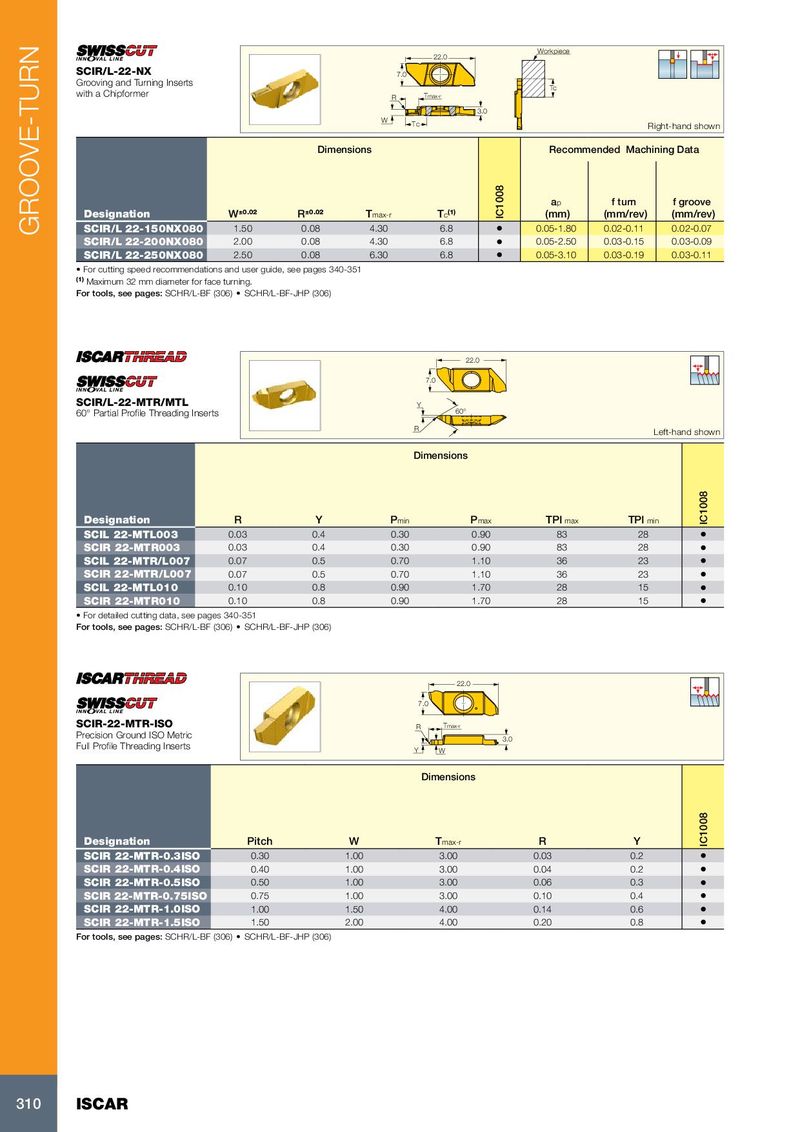
SCIR/L-22-NX 7.0
Grooving and Turning Inserts
Tc
with a Chipformer R Tmax-r
3.0
W
Tc Right-hand shown
Dimensions Recommended Machining Data
IC1008
ap f turn f groove
Designation W±0.02 R±0.02 Tmax-r Tc(1) (mm) (mm/rev) (mm/rev)
SCIR/L 22-150NX080 1.50 0.08 4.30 6.8 • 0.05-1.80 0.02-0.11 0.02-0.07
SCIR/L 22-200NX080 2.00 0.08 4.30 6.8 • 0.05-2.50 0.03-0.15 0.03-0.09
SCIR/L 22-250NX080 2.50 0.08 6.30 6.8 • 0.05-3.10 0.03-0.19 0.03-0.11
• For cutting speed recommendations and user guide, see pages 340-351
(1) Maximum 32 mm diameter for face turning.
For tools, see pages: SCHR/L-BF (306) • SCHR/L-BF-JHP (306)
22.0
7.0
SCIR/L-22-MTR/MTL Y
60° Partial Profile Threading Inserts 60°
R
Left-hand shown
Dimensions
IC1008
Designation R Y Pmin Pmax TPI max TPI min
SCIL 22-MTL003 0.03 0.4 0.30 0.90 83 28 •
SCIR 22-MTR003 0.03 0.4 0.30 0.90 83 28 •
SCIL 22-MTR/L007 0.07 0.5 0.70 1.10 36 23 •
SCIR 22-MTR/L007 0.07 0.5 0.70 1.10 36 23 •
SCIL 22-MTL010 0.10 0.8 0.90 1.70 28 15 •
SCIR 22-MTR010 0.10 0.8 0.90 1.70 28 15 •
• For detailed cutting data, see pages 340-351
For tools, see pages: SCHR/L-BF (306) • SCHR/L-BF-JHP (306)
22.0
7.0
SCIR-22-MTR-ISO R Tmax-r
Precision Ground ISO Metric 3.0
Full Profile Threading Inserts Y W
Dimensions
IC1008
Designation Pitch W Tmax-r R Y
SCIR 22-MTR-0.3ISO 0.30 1.00 3.00 0.03 0.2 •
SCIR 22-MTR-0.4ISO 0.40 1.00 3.00 0.04 0.2 •
SCIR 22-MTR-0.5ISO 0.50 1.00 3.00 0.06 0.3 •
SCIR 22-MTR-0.75ISO 0.75 1.00 3.00 0.10 0.4 •
SCIR 22-MTR-1.0ISO 1.00 1.50 4.00 0.14 0.6 •
SCIR 22-MTR-1.5ISO 1.50 2.00 4.00 0.20 0.8 •
For tools, see pages: SCHR/L-BF (306) • SCHR/L-BF-JHP (306)
310 ISCAR