Каталог Iscar токарный инструмент 2017 - страница 312
Навигация
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar расточные системы 2022
 Каталог Iscar высокоточные развертки и метчики 2022
 Токарные инструменты Iscar (часть 2) 2026
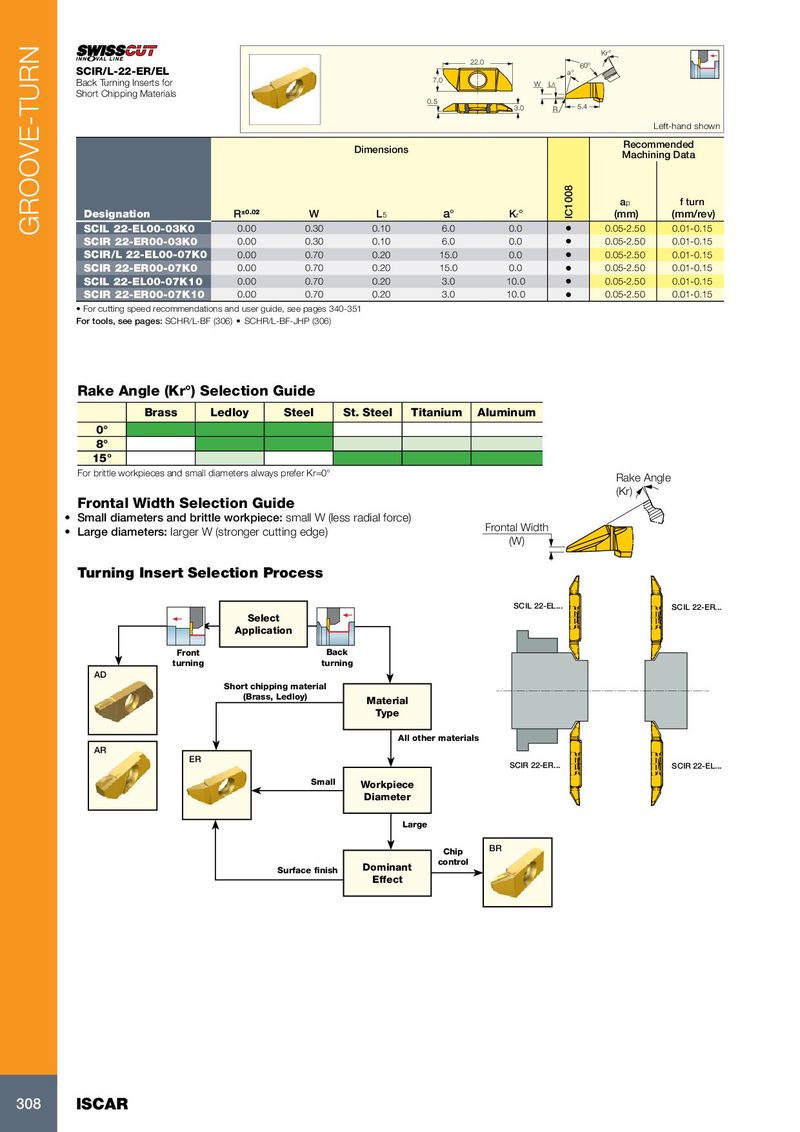
GROOVE-TURN
Kr°
22.0 60°
SCIR/L-22-ER/EL a°
Back Turning Inserts for 7.0
W L5
Short Chipping Materials
0.5
3.0 R 5.4
Left-hand shown
Recommended
Dimensions
Machining Data
IC1008
ap f turn
Designation R±0.02 W L5 a° Kr° (mm) (mm/rev)
SCIL 22-EL00-03K0 0.00 0.30 0.10 6.0 0.0 • 0.05-2.50 0.01-0.15
SCIR 22-ER00-03K0 0.00 0.30 0.10 6.0 0.0 • 0.05-2.50 0.01-0.15
SCIR/L 22-EL00-07K0 0.00 0.70 0.20 15.0 0.0 • 0.05-2.50 0.01-0.15
SCIR 22-ER00-07K0 0.00 0.70 0.20 15.0 0.0 • 0.05-2.50 0.01-0.15
SCIL 22-EL00-07K10 0.00 0.70 0.20 3.0 10.0 • 0.05-2.50 0.01-0.15
SCIR 22-ER00-07K10 0.00 0.70 0.20 3.0 10.0 • 0.05-2.50 0.01-0.15
• For cutting speed recommendations and user guide, see pages 340-351
For tools, see pages: SCHR/L-BF (306) • SCHR/L-BF-JHP (306)
Rake Angle (Kr°) Selection Guide
Brass Ledloy Steel St. Steel Titanium Aluminum
0°
8°
15°
For brittle workpieces and small diameters always prefer Kr=0°
Rake Angle
(Kr)
Frontal Width Selection Guide
• Small diameters and brittle workpiece: small W (less radial force)
• Large diameters: larger W (stronger cutting edge) Frontal Width
(W)
Turning Insert Selection Process
SCIL 22-EL... SCIL 22-ER...
Select
Application
Front Back
turning turning
AD
Short chipping material
(Brass, Ledloy)
Material
Type
All other materials
AR
ER
SCIR 22-ER... SCIR 22-EL...
Small Workpiece
Diameter
Large
Chip BR
control
Surface finish Dominant
Effect
308 ISCAR