Каталог Iscar токарный инструмент 2017 - страница 260
Навигация
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar расточные системы 2022
 Каталог Iscar высокоточные развертки и метчики 2022
 Токарные инструменты Iscar (часть 2) 2026
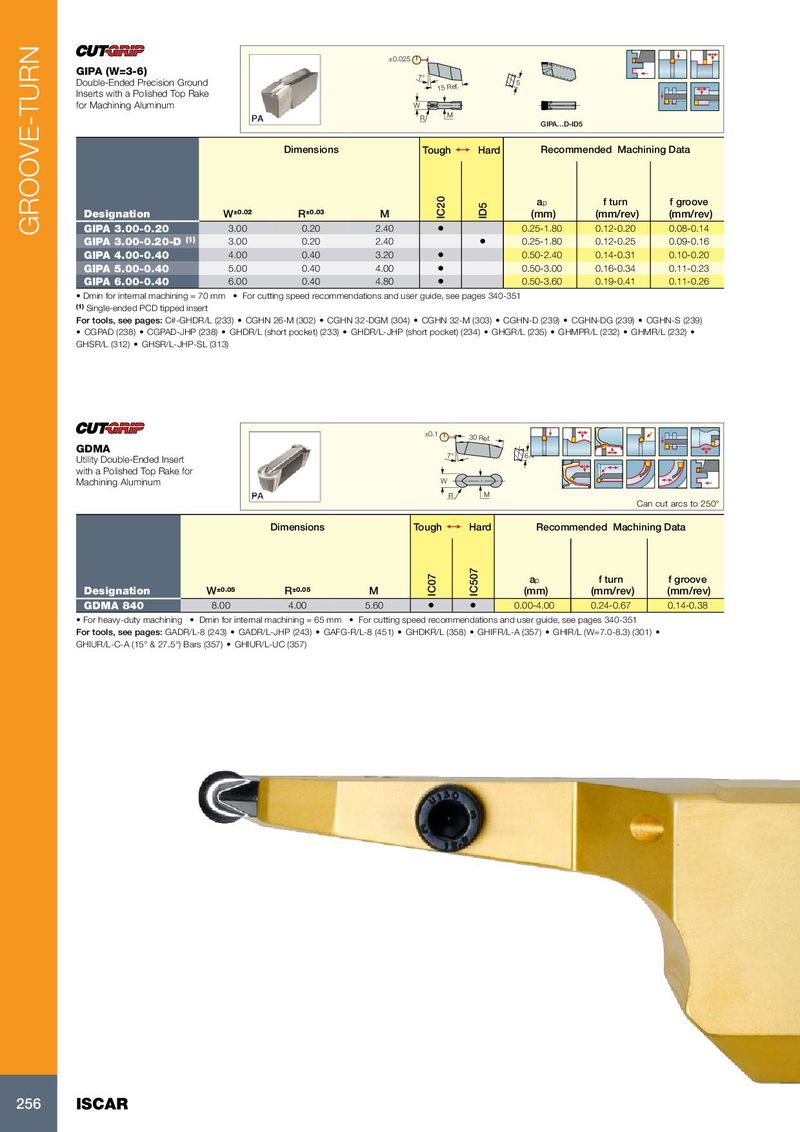
GIPA (W=3-6)
Double-Ended Precision Ground 7° Inserts with a Polished Top Rake 15 Ref. for Machining Aluminum W R M GIPA…D-ID5
Dimensions Tough 1 Hard Recommended Machining Data
| a p | f turn | f groove | ||||||
| Designation | W ±0.02 | R±0.03 | M | (mm) | (mm/rev) | (mm/rev) | ||
| GIPA 3.00-0.20 | 3.00 | 0.20 | 2.40 | • | 0.25-1.80 | 0.12-0.20 | 0.08-0.14 | |
| GIPA 3.00-0.20-D (1) | 3.00 | 0.20 | 2.40 | • 0.25-1.80 | 0.12-0.25 | 0.09-0.16 | ||
| GIPA 4.00-0.40 | 4.00 | 0.40 | 3.20 | • | 0.50-2.40 | 0.14-0.31 | 0.10-0.20 | |
| GIPA 5.00-0.40 | 5.00 | 0.40 | 4.00 | • | 0.50-3.00 | 0.16-0.34 | 0.11-0.23 | |
| GIPA 6.00-0.40 | 6.00 | 0.40 | 4.80 | • | 0.50-3.60 | 0.19-0.41 | 0.11-0.26 |
- Dmin for internal machining = 70 mm
- For cutting speed recommendations and user guide, see pages 340-351
(1) Single-ended PCD tipped insert For tools, see pages: C#-GHDR/L (233) CGHN 26-M (302) CGHN 32-DGM (304) CGHN 32-M (303) CGHN-D (239) CGHN-DG (239) CGHN-S (239)
- CGPAD (238)
- CGPAD-JHP (238)
- GHDR/L (short pocket) (233)
- GHDR/L-JHP (short pocket) (234)
- GHGR/L (235)
- GHMPR/L (232)
- GHMR/L (232)
GHSR/L (312) GHSR/L-JHP-SL (313)
±0.1 30 Ref.
GDMA
| Utility Double-Ended Insert | 7° | 6.4 | ||
| with a Polished Top Rake for | ||||
| Machining Aluminum | W | |||
| R | M | |||
| Can cut arcs to 250° |
Dimensions Tough 1 Hard Recommended Machining Data
| ap | f turn | f groove | |||||||
| Designation | W±0.05 | R ±0.05 | M | (mm) | (mm/rev) | (mm/rev) | |||
| GDMA 840 | 8.00 | 4.00 | 5.60 | • | • | 0.00-4.00 | 0.24-0.67 | 0.14-0.38 |
- For heavy-duty machining
- Dmin for internal machining = 65 mm
- For cutting speed recommendations and user guide, see pages 340-351
For tools, see pages: GADR/L-8 (243) GADR/L-JHP (243) GAFG-R/L-8 (451) GHDKR/L (358) GHIFR/L-A (357) GHIR/L (W=7.0-8.3) (301) GHIUR/L-C-A (15° & 27.5°) Bars (357) GHIUR/L-UC (357)