Каталог Iscar токарный инструмент 2017 - страница 166
Навигация
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar расточные системы 2022
 Каталог Iscar высокоточные развертки и метчики 2022
 Токарные инструменты Iscar (часть 2) 2026
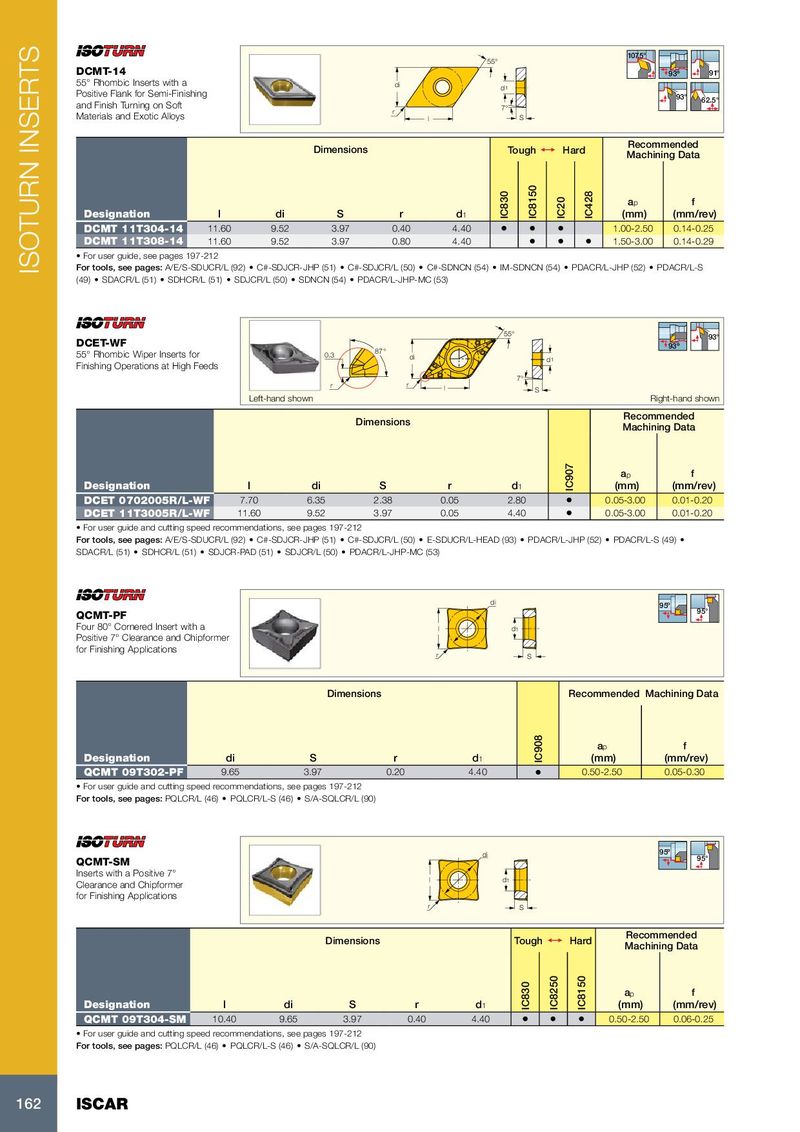
DCMT-14
di d Positive Flank for Semi-Finishing 1 and Finish Turning on Soft r 7° Materials and Exotic Alloys S l Dimensions Tough 1 Hard
93° 62.5°
Recommended Machining Data
ap f
| Designation | l | di | S | r | d 1 | (mm) | (mm/rev) | ||||
| DCMT 11T304-14 | 11.60 | 9.52 | 3.97 | 0.40 | 4.40 | • | • | • | 1.00-2.50 | 0.14-0.25 | |
| DCMT 11T308-14 | 11.60 | 9.52 | 3.97 | 0.80 | 4.40 | • | • | • | 1.50-3.00 | 0.14-0.29 |
- For user guide, see pages 197-212
For tools, see pages: A/E/S-SDUCR/L (92) C#-SDJCR-JHP (51) C#-SDJCR/L (50) C#-SDNCN (54) IM-SDNCN (54) PDACR/L-JHP (52) PDACR/L-S (49) SDACR/L (51) SDHCR/L (51) SDJCR/L (50) SDNCN (54) PDACR/L-JHP-MC (53)
DCET-WF
| 55° Rhombic Wiper Inserts for | 0.3 | 87° | |
| di | |||
| Finishing Operations at High Feeds |
r r l
Left-hand shown Dimensions
55° d 1 7° S
93° 93º
Right-hand shown Recommended Machining Data
ap f
| Designation | l | di | S | r | d1 | (mm) | (mm/rev) | |
| DCET 0702005R/L-WF | 7.70 | 6.35 | 2.38 | 0.05 | 2.80 | • | 0.05-3.00 | 0.01-0.20 |
| DCET 11T3005R/L-WF | 11.60 | 9.52 | 3.97 | 0.05 | 4.40 | • | 0.05-3.00 | 0.01-0.20 |
- For user guide and cutting speed recommendations, see pages 197-212
For tools, see pages: A/E/S-SDUCR/L (92) C#-SDJCR-JHP (51) C#-SDJCR/L (50) E-SDUCR/L-HEAD (93) PDACR/L-JHP (52) PDACR/L-S (49) SDACR/L (51) SDHCR/L (51) SDJCR-PAD (51) SDJCR/L (50) PDACR/L-JHP-MC (53)
di 95º QCMT-PF 95°
Four 80° Cornered Insert with a l d
1 Positive 7° Clearance and Chipformer for Finishing Applications r S
Dimensions Recommended Machining Data
a p f
| Designation | di | S | r | d 1 | (mm) | (mm/rev) | |
| QCMT 09T302-PF | 9.65 | 3.97 | 0.20 | 4.40 | • | 0.50-2.50 | 0.05-0.30 |
- For user guide and cutting speed recommendations, see pages 197-212
For tools, see pages: PQLCR/L (46) PQLCR/L-S (46) S/A-SQLCR/L (90)
di 95º QCMT-SM 95° Inserts with a Positive 7°
Clearance and Chipformer l d1
for Finishing Applications r S Recommended Dimensions Tough 1 Hard
Machining Data
ap f
| Designation | l | di | S | r | d1 | (mm) | (mm/rev) | |||
| QCMT 09T304-SM | 10.40 | 9.65 | 3.97 | 0.40 | 4.40 | • | • | • | 0.50-2.50 | 0.06-0.25 |
For tools, see pages: PQLCR/L (46) PQLCR/L-S (46) S/A-SQLCR/L (90)