Каталог Iscar токарный инструмент 2017 - страница 152
Навигация
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar расточные системы 2022
 Каталог Iscar высокоточные развертки и метчики 2022
 Токарные инструменты Iscar (часть 2) 2026
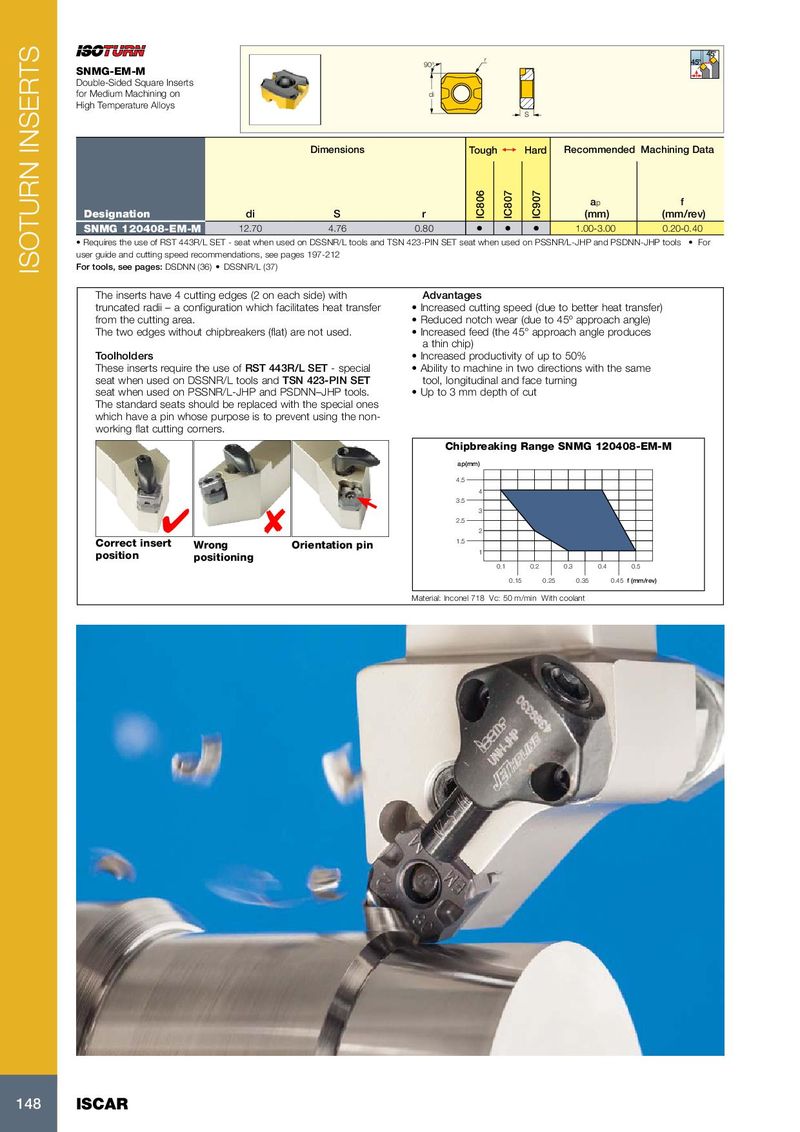
SNMG-EM-M 90° Double-Sided Square Inserts for Medium Machining on di High Temperature Alloys S
Dimensions Tough 1 Hard Recommended Machining Data
ap f
| Designation | di | S | r | (mm) | (mm/rev) | |||
| SNMG 120408-EM-M | 12.70 | 4.76 | 0.80 | • | • | • | 1.00-3.00 | 0.20-0.40 |
- Requires the use of RST 443R/L SET - seat when used on DSSNR/L tools and TSN 423-PIN SET seat when used on PSSNR/L-JHP and PSDNN-JHP tools
- For
user guide and cutting speed recommendations, see pages 197-212 For tools, see pages: DSDNN (36) DSSNR/L (37)
| The inserts have 4 cutting edges (2 on each side) with | Advantages |
| truncated radii – a configuration which facilitates heat transfer | • Increased cutting speed (due to better heat transfer) |
| from the cutting area. | • Reduced notch wear (due to 45º approach angle) |
| The two edges without chipbreakers (flat) are not used. | • Increased feed (the 45° approach angle produces |
| a thin chip) | |
| Toolholders | • Increased productivity of up to 50% |
| These inserts require the use of RST 443R/L SET - special | • Ability to machine in two directions with the same |
| seat when used on DSSNR/L tools and TSN 423-PIN SET | tool, longitudinal and face turning |
| seat when used on PSSNR/L-JHP and PSDNN–JHP tools. | • Up to 3 mm depth of cut |
The standard seats should be replaced with the special ones which have a pin whose purpose is to prevent using the non- working flat cutting corners. Chipbreaking Range SNMG 120408-EM-M
ap(mm) 4.5 4 3.5 3 2.5 2
| Correct insert | Wrong | Orientation pin | 1.5 | |
| position | positioning | 1 |
0.1 0.2 0.3 0.4 0.5
0.15 0.25 0.35 0.45 f (mm/rev)
Material: Inconel 718 Vc: 50 m/min With coolant