Каталог Iscar сверла со сменной режущей частью 2022 - страница 78
Навигация
 Каталог Iscar монолитные фрезы 2022
 Каталог Iscar токарный инструмент
 Каталог Iscar инструмент для мелкоразмерной обработки
 Каталог Iscar токарный инструмент для нарезания канавок
 Каталог Iscar полирующие фрезы
 Каталог Iscar дисковые фрезы и фрезерные пластины 2022
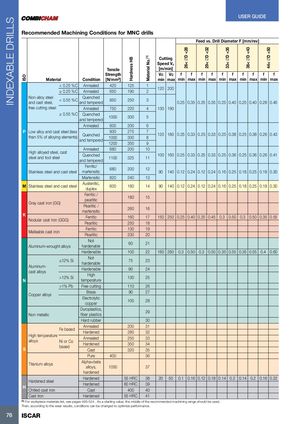
Recommended Machining Conditions for MNC drills
| Tensile | ness HB | rial No.(1) | Cutt Spee [m/m | ing d Vc in] | 26 | Feed | vs. Dr 29 | ill Dia | mete 33 | r F[m | m/rev 36 | ] 44 | ||||
| ISO Material | Condition | Strength [N/mm2] | Hard | Mate | Vc min | Vc max | f min | f max | f min | f max | f min | f max | f min | f max | f min | f max |
| < 0.25 %C ≥ 0.25 %C | Annealed Annealed | 420 650 | 125 190 | 1 2 | 120 | 200 | ||||||||||
| Non-alloy steel and cast steel, < 0.55 %C | Quenched and tempered | 850 | 250 | 3 | 0.25 | 0.35 | 0.25 | 0.35 | 0.25 | 0.40 | 0.25 | 0.40 | 0.28 | 0.45 | ||
| free cutting steel ≥ 0.55 %C | Annealed Quenched and tempered | 750 1000 | 220 300 | 4 5 | 130 | 190 | ||||||||||
| Annealed | 600 | 200 | 6 | |||||||||||||
| P Low alloy and cast steel (less than 5% of alloying elements) | Quenched and temered | 930 1000 | 275 300 | 7 8 | 120 | 180 | 0.25 | 0.33 | 0.25 | 0.33 | 0.25 | 0.38 | 0.25 | 0.38 | 0.26 | 0.43 |
| p | 1200 | 350 | 9 | |||||||||||||
| Annealed | 680 | 200 | 10 | |||||||||||||
| High alloyed steel, cast steel and tool steel | Quenched and tempered | 1100 | 325 | 11 | 100 | 160 | 0.25 | 0.33 | 0.25 | 0.33 | 0.25 | 0.36 | 0.25 | 0.36 | 0.26 | 0.41 |
| Stainless steel and cast steel | Ferritic/ martensitic Martensitic | 680 820 | 200 240 | 12 13 | 90 | 140 | 0.12 | 0.24 | 0.12 | 0.24 | 0.16 | 0.25 | 0.18 | 0.25 | 0.18 | 0.30 |
| M Stainless steel and cast steel | Austenitic, duplex | 600 | 180 | 14 | 90 | 140 | 0.12 | 0.24 | 0.12 | 0.24 | 0.16 | 0.25 | 0.18 | 0.25 | 0.18 | 0.30 |
| Ferritic / pearlitic | 180 | 15 | ||||||||||||||
| Gray cast iron (GG) | Pearlitic / | 260 | 16 | |||||||||||||
| martensitic | ||||||||||||||||
| K NdltiGGG | Ferritic | 160 | 17 | 150 | 250 | 0.25 | 0.40 | 0.25 | 0.45 | 0.3 | 0.50 | 0.3 | 0.50 | 0.35 | 0.55 | |
| ouar cas ron () | Pearlitic | 250 | 18 | |||||||||||||
| Ferritic | 130 | 19 | ||||||||||||||
| Malleable cast iron | Pearlitic | 230 | 20 | |||||||||||||
| Not | ||||||||||||||||
| Aluminum-wrought alloys | hardenable | 60 | 21 | |||||||||||||
| Hardenable | 100 | 22 | 160 | 260 | 0.3 | 0.50 | 0.3 | 0.50 | 0.35 | 0.55 | 0.35 | 0.55 | 0.4 | 0.60 | ||
| Not | ||||||||||||||||
| Aluminum- ≤12% Si | hardenable | 75 | 23 | |||||||||||||
| Hardenable | 90 | 24 | ||||||||||||||
| N cast alloys >12% Si | High temperature | 130 | 25 | |||||||||||||
| >1% Pb | Free cutting | 110 | 26 | |||||||||||||
| Brass | 90 | 27 | ||||||||||||||
| Copper alloys | Electrolytic copper | 100 | 28 | |||||||||||||
| Duroplastics | ||||||||||||||||
| Non metallic | , fiberplastics | 29 | ||||||||||||||
| Hard rubber | 30 | |||||||||||||||
| Annealed | 200 | 31 | ||||||||||||||
| Hih temerature Fe based | Hardened | 280 | 32 | |||||||||||||
| g p | Annealed | 250 | 33 | |||||||||||||
| alloys Ni or Co | ||||||||||||||||
| S based | Hardened Cast | 350 320 | 34 35 | |||||||||||||
| Pure | 400 | 36 | ||||||||||||||
| Titanium alloys | Alpha+beta | |||||||||||||||
| alloys, | 1050 | 37 | ||||||||||||||
| Hardened steel | hardened Hardened | 55 HRC | 38 | 20 | 50 | 0.1 | 0.16 | 0.12 | 0.18 | 0.14 | 0.2 | 0.14 | 0.2 | 0.16 | 0.22 | |
| Hardened | 60 HRC | 39 | ||||||||||||||
| H Chilled cast iron | Cast | 400 | 40 | |||||||||||||
| Cast iron | Hardened | 55 HRC | 41 |
(1) For workpiece materials list, see pages 495-524 . As a starting value, the middle of the recommended machining range should be used. Then, according to the wear results, conditions can be changed to optimize performance.