Каталог Iscar сверла со сменной режущей частью 2022 - страница 124
Навигация
 Каталог Iscar монолитные фрезы 2022
 Каталог Iscar токарный инструмент
 Каталог Iscar инструмент для мелкоразмерной обработки
 Каталог Iscar токарный инструмент для нарезания канавок
 Каталог Iscar полирующие фрезы
 Каталог Iscar дисковые фрезы и фрезерные пластины 2022
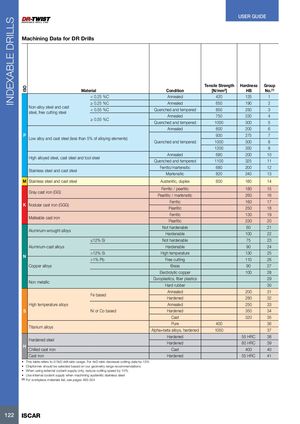
Machining Data for DR Drills
| ISO Material | Condition | Tensile Strength [N/mm2] | Hardness HB | Group No.(1) |
| < 0.25 %C | Annealed | 420 | 125 | 1 |
| Nlltldt ≥ 0.25 %C | Annealed | 650 | 190 | 2 |
| on-aoy see an cas steel free cutting steel < 0.55 %C | Quenched and tempered | 850 | 250 | 3 |
| , ≥ 055 %C | Annealed | 750 | 220 | 4 |
| . | Quenched and tempered | 1000 | 300 | 5 |
| Annealed | 600 | 200 | 6 | |
| P Low allo and cast steel (less than 5% of alloin elements) | 930 | 275 | 7 | |
| y yg | Quenched and tempered | 1000 | 300 | 8 |
| 1200 | 350 | 9 | ||
| Hih alloed steel cast steel and tool steel | Annealed | 680 | 200 | 10 |
| g y , | Quenched and tempered | 1100 | 325 | 11 |
| Stiltldttl | Ferritic/martensitic | 680 | 200 | 12 |
| aness see an cas see | Martensitic | 820 | 240 | 13 |
| M Stainless steel and cast steel | Austenitic, duplex | 600 | 180 | 14 |
| Gra cast iron (GG) | Ferritic /pearlitic | 180 | 15 | |
| y | Pearlitic / martensitic | 260 | 16 | |
| K Nodlar cast iron (GGG) | Ferritic | 160 | 17 | |
| u | Pearlitic | 250 | 18 | |
| Malleable cast iron | Ferritic | 130 | 19 | |
| Pearlitic | 230 | 20 | ||
| Not hardenable | 60 | 21 | ||
| Aluminum-wrought alloys | Hardenable | 100 | 22 | |
| ≤12% Si | Not hardenable | 75 | 23 | |
| Aluminum-cast alloys | Hardenable | 90 | 24 | |
| N >12% Si | High temperature | 130 | 25 | |
| >1% Pb | Free cutting | 110 | 26 | |
| Copper alloys | Brass | 90 | 27 | |
| Electrolytic copper | 100 | 28 | ||
| Non metallic | Duroplastics, fiberplastics | 29 | ||
| Hard rubber | 30 | |||
| F bd | Annealed | 200 | 31 | |
| e ase | Hardened | 280 | 32 | |
| High temperature alloys | Annealed | 250 | 33 | |
| S Ni or Co based | Hardened | 350 | 34 | |
| Cast | 320 | 35 | ||
| Titanium allos | Pure | 400 | 36 | |
| y | Alpha+beta alloys, hardened | 1050 | 37 | |
| Hardened steel | Hardened | 55 HRC | 38 | |
| H | Hardened | 60 HRC | 39 | |
| Chilled cast iron | Cast | 400 | 40 | |
| Cast iron | Hardened | 55 HRC | 41 |
- This table refers to 2/3xD drill ratio usage. For 4xD ratio decrease cutting data by 15%
- Chipformer should be selected based on our geometry range recommendations
- When using external coolant supply only, reduce cutting speed by 10%
- Use internal coolant supply when machining austenitic stainless steel
(1) For workpiece materials list, see pages 495-524