Каталог Iscar сверла ружейные и для глубокого сверления 2022 - страница 110
Навигация
 Каталог Iscar новые продукты 2018
 Каталог Iscar полирующие фрезы
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar инструмент для нарезания резьбы
 Каталог Iscar токарные державки ISO 2022
 Фрезерные инструменты Iscar 2026
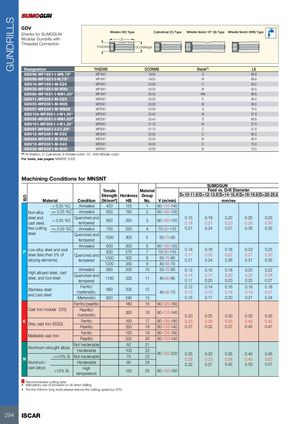
GDV
| hanks for SUMOGUN odular Gundrills with | LS Weldon (W) Type Cylindrical (C) Type | Whistle Notch 15° (S) Type | Whistle Notch (WN) Type |
| hreaded Connection | THSZWS DCONMSg6 | ||
| Designation | THSZWS DCONMS | Shank(1) | LS |
| GDV56-MF16X1-I-WN.75" | MF16X1 19.05 | S | 69.8 |
| GDV99-MF16X1-I-W.75" | MF16X1 19.05 | W | 69.8 |
| GDV10-MF16X1-M-C20 | MF16X1 20.00 | C | 50.0 |
| GDV22-MF16X1-M-W20 | MF16X1 20.00 | W | 50.0 |
| GDV80-MF16X1-I-WN1.00" | MF16X1 25.40 | WN | 69.8 |
| GDV11-MF20X1-M-C25 | MF20X1 25.00 | C | 56.0 |
| GDV23-MF20X1-M-W25 | MF20X1 25.00 | W | 56.0 |
| GDV57-MF20X1-M-WN25 | MF20X1 25.00 | S | 70.0 |
| GDV100-MF20X1-I-W1.00" | MF20X1 25.40 | W | 57.9 |
| GDV58-MF20X1-I-WN1.00" | MF20X1 25.40 | S | 69.8 |
| GDV101-MF20X1-I-W1.25" | MF20X1 31.75 | W | 57.9 |
| GDV97-MF20X1-I-C1.25" | MF20X1 31.75 | C | 57.9 |
| GDV12-MF20X1-M-C32 | MF20X1 32.00 | C | 60.0 |
| GDV24-MF20X1-M-W32 | MF20X1 32.00 | W | 60.0 |
| GDV13-MF20X1-M-C40 | MF20X1 40.00 | C | 70.0 |
| GDV25-MF20X1-M-W40 | MF20X1 40.00 | W | 70.0 |
(1) W-Weldon, C-Cylindrical, S-Whistle notch 15°, WN-Whistle notch
For tools, see pages: MNSNT (293)
Machining Conditions for MNSNT
| SUMO | GUN | |||||||||
| Tensile | Material | Feed | vs. Drill Dia | meter | ||||||
| O | Strength | Hardness | Group | D=10-11.9 | D=12-13.9 | D=14-15.9 | D=16-19.9 | D=20-25.9 | ||
| IS Material | Condition | [N/mm2] | HB | No. | V (m/min) | mm/rev | ||||
| < 0.25 %C | Annealed | 420 | 125 | 1 | 80-110-140 | |||||
| Non-alloy >= 0.25 %C | Annealed | 650 | 190 | 2 | 80-105-130 | |||||
| steel and < 055 %C | Quenched and | 850 | 250 | 3 | 80-100-120 | 0.15 | 0.18 | 0.20 | 0.25 | 0.25 |
| cast steel, . | tempered | 0.18 | 0.21 | 0.23 | 0.30 | 0.30 | ||||
| free cutting >= 0.55 %C | Annealed | 750 | 220 | 4 | 70-90-110 | 0.21 | 0.24 | 0.27 | 0.35 | 0.35 |
| steel | Quenched and tempered | 1000 | 300 | 5 | 50-70-90 | |||||
| Annealed | 600 | 200 | 6 | 80-100-120 | ||||||
| P Low alloy steel and cast | 930 | 275 | 7 | 70-90-110 | 0.14 | 0.16 | 0.18 | 0.23 | 0.25 | |
| steel (less than 5% of | Quenched and | 017 | 020 | 022 | 027 | 030 | ||||
| alloying elements) | tempered | 1000 1200 | 300 350 | 8 9 | 50-70-90 40-55-70 | . 0.21 | . 0.24 | . 0.26 | . 0.31 | . 0.35 |
| Hih alloed steel cast | Annealed | 680 | 200 | 10 | 50-70-90 | 0.12 | 0.15 | 0.18 | 0.20 | 0.22 |
| g y , steel, and tool steel | Quenched and tempered | 1100 | 325 | 11 | 40-60-80 | 0.14 0.17 | 0.17 0.20 | 0.20 0.23 | 0.22 0.25 | 0.24 0.27 |
| Stainless steel dttl | Ferritic/ martensitic. | 680 | 200 | 12 | 40-55-70 | 0.12 0.13 | 0.14 0.15 | 0.16 0.18 | 0.16 0.19 | 0.18 0.21 |
| an cas see | Martensitic | 820 | 240 | 13 | 0.15 | 0.17 | 0.20 | 0.21 | 0.24 | |
| Ferritic/pearlitic | 180 | 15 | 90-125-160 | |||||||
| Cast iron nodular (GG) | Pearlitic/ martensitic | 260 | 16 | 80-110-140 | 0.20 | 0.25 | 0.30 | 0.35 | 0.35 | |
| K GtiGGG | Ferritic | 160 | 17 | 90-135-180 | 0.23 | 0.28 | 0.33 | 0.40 | 0.42 | |
| rey cas ron () | Pearlitic | 250 | 18 | 80-110-140 | 0.27 | 0.32 | 0.37 | 0.45 | 0.47 | |
| Ferritic | 130 | 19 | 90-125-160 | |||||||
| Malleable cast iron | Pearlitic | 230 | 20 | 80-110-140 | ||||||
| Aluminum-wrought alloys | Not hardenable | 60 | 21 | |||||||
| Hdbl | 100 | 22 | ||||||||
| arenae | 90-155-220 | 025 | 030 | 035 | 040 | 045 | ||||
| N | Not hardenable | 75 | 23 | . 028 | . 033 | . 038 | . 045 | . 050 | ||
| Aluminum- | Hardenable | 90 | 24 | . 0.32 | . 0.37 | . 0.42 | . 0.50 | . 0.57 | ||
| cast alloys >12% Si | High temperature | 130 | 25 | 80-120-160 |
Recommended cutting data
- Mandatory use of emulsion or oil when drilling
- For the 400mm long tools please reduce the cutting speed by 20%.