Каталог Iscar сверла ружейные и для глубокого сверления 2022 - страница 111
Навигация
 Каталог Iscar новые продукты 2018
 Каталог Iscar полирующие фрезы
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar инструмент для нарезания резьбы
 Каталог Iscar токарные державки ISO 2022
 Фрезерные инструменты Iscar 2026
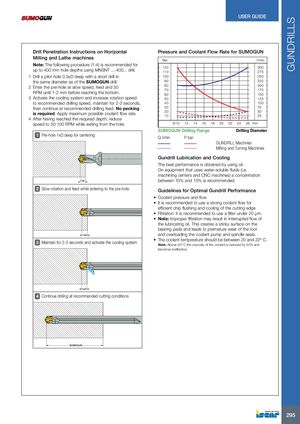
Drill Penetration Instructions on Horizontal Pressure and Coolant Flow Rate for SUMOGUN
Milling and Lathe machines
Bar l/min
Note: The following procedure (1-4) is recommended for
| up to 400 mm hole depths using MNSNT ...-400... drill. | 120 | 300 | |
| 110 | 275 | ||
| 1 Drill a pilot hole 0.5xD deep with a short drill in | 100 | 250 | |
| the same diameter as of the SUMOGUN drill. | 90 | 225 | |
| 2 Enter the pre-hole at slow speed, feed and 50 | 80 | 200 | |
| RPM until 1-2 mm before reaching the bottom. | 70 | 175 | |
| 60 | 150 | ||
| 3 Activate the cooling system and increase rotation speed | 50 | 125 | |
| to recommended drilling speed, maintain for 2-3 seconds, | 40 | 100 | |
| then continue at recommended drilling feed. No pecking | 30 | 75 | |
| is required. Apply maximum possible coolant flow rate. | 20 | 50 | |
| 10 | 25 | ||
| 4 After having reached the required depth, reduce |
speed to 50-100 RPM while exiting from the hole. Ø10 12 14 16 18 20 22 24 26 mm
SUMOGUN Drilling Range SUMOGUN Drilling RangeDrilling DiameterDrilling Diameter 1 Pre-hole 1xD deep for centering Q l/min P bar GUNDRILL Machines
Milling and Turning Machines
Gundrill Lubrication and Cooling
The best performance is obtained by using oil. On equipment that uses water-soluble fluids (i.e. machining centers and CNC machines) a concentration between 10% and 15% is recommended. 1xD
2 Slow rotation and feed while entering to the pre-hole Guidelines for Optimal Gundrill Performance
- Coolant pressure and flow
- It is recommended to use a strong coolant flow for efficient chip flushing and cooling of the cutting edge
- Filtration: It is recommended to use a filter under 20 µm.
- Note: Improper filtration may result in interrupted flow of the lubricating oil. This creates a sticky surface on the bearing pads and leads to premature wear of the tool and overloading the coolant pump and spindle seals.
1xD
- The coolant temperature should be between 20 and 22º C.
3 Maintain for 2-3 seconds and activate the cooling system
Note: Above 50º C the viscosity of the coolant is reduced by 50% and becomes ineffective.
1xD 4 Continue drilling at recommended cutting conditions
SUMOGUN