Каталог Iscar отрезка 2022 - страница 117
Навигация
 Токарные инструменты Iscar (часть 1) 2026
 Каталог Iscar монолитные фрезы 2022
 Инструменты для обработки отверстий Iscar 2026
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar расточные системы
 Каталог Iscar токарный инструмент 2017
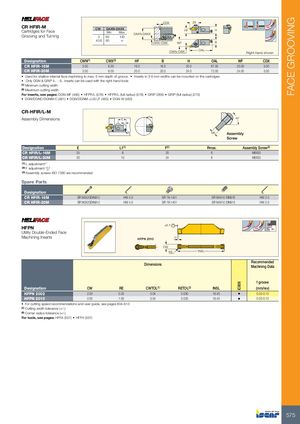
| CR HFIR-M Cartridges for Face | CW | DAXN- Min | DAXX Max | CDX DAXNDAXX | HF H 25 | |
| Grooving and Turning | 3 | 60 | 130 | - | ||
| 4,5,6 | 60 | ∞ | CWN CWN-CWX | WF -CWX OAL B | Right-hand shown | |
| Designation | CWN(1) | CWX(2 | ) | HF B | H OAL | WF CDX |
| CR HFIR-16M | 3.00 | 6.00 | 16.0 16.0 | 20.0 67.00 | 20.00 5.00 | |
| CR HFIR-20M | 3.00 | 6.00 | 20.0 20.0 | 24.0 72.00 | 24.00 5.00 |
- Used for shallow internal face machining to max. 5 mm depth of groove
- Inserts in 3-6 mm widths can be mounted on the cartridges
- Only DGN & GRIP 4.. - 6.. inserts can be used with the right-hand tools
(1) Minimum cutting width (2) Maximum cutting width
For inserts, see pages: DGN-MF (485) HFPR/L (576) HFPR/L (full radius) (576) GRIP (269) GRIP (full radius) (270)
- DGN/DGNC/DGNM-C (481)
- DGN/DGNM-J/JS/JT (483)
- DGN-W (482)
| CR-HFIR/L-M Assembly Dimensions | E R L1 | F | Assembly Screw 45º M8 | |||
| Designation | E | L1(1) | F(2) | Rmax. As | semblyScrew(3) | |
| CR HFIR/L-16M | 25 | 8 | 20 | 6 | M8X30 | |
| CR HFIR/L-20M | 30 | 10 | 24 | 6 | M8X30 |
(1) L adjustment±1 (2) F adjustment +0.3 -0 (3) Assembly screws ISO 7380 are recommended
| Spare Parts | |||||
| Designation | |||||
| CR HFIR-16M | SR M5X20DIN912 | HW 4.0 | SR 76-1401 | SR M4X10 DIN916 | HW 2.0 |
| CR HFIR-20M | SR M5X20DIN912 | HW 4.0 | SR 76-1401 | SR M4X10 DIN913 | HW 2.0 |
HFPN ±0.1
Utility Double-Ended Face
Machining Inserts 7° HFPN 2010 CW RE INSL
| Dimensions | Recommended Machining Data | ||||||
| Designation | CW | RE | CWTOL(1) | RETOL(2) | INSL | IC808 | f groove (mm/rev) |
| HFPN 2002 | 2.00 | 0.20 | 0.04 | 0.030 | 19.40 | • | 0.03-0.10 |
| HFPN 2010 | 2.00 | 1.00 | 0.04 | 0.030 | 19.40 | • | 0.03-0.10 |
- For cutting speed recommendations and user guide, see pages 604-613
(1) Cutting width tolerance (+/-) (2) Corner radius tolerance (+/-)
For tools, see pages: HFFA (557) HFFH (557)