Каталог Iscar обработка канавок 2022 - страница 195
Навигация
 Каталог Iscar монолитные концевые фрезы и система multi-master
 Фрезерные инструменты Iscar 2026
 Каталог Iscar сверла ружейные и для глубокого сверления 2022
 Каталог Iscar токарные державки ISO 2022
 Каталог Iscar инструмент для обработки алюминиевых колёс
TOOLS FOR ALUMINUM WHEELS
LH OAL
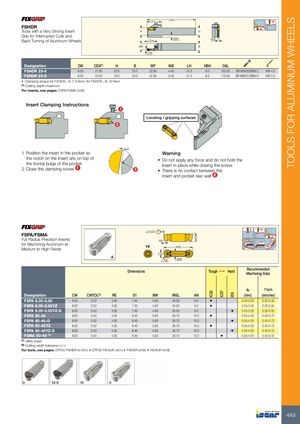
FSHDR
Tools with a Very Strong Insert H H
Grip for Interrupted Cuts and
HBH WB
Back Turning of Aluminum Wheels CDX
WF B
CW
Designation CW CDX(1) H B WF WB LH HBH OAL
FSHDR 25-6 6.00 21.00 25.0 25.0 22.80 4.40 51.0 8.0 150.00 SR M5X20DIN912 HW 4.0
FSHDR 25-8 8.00 25.50 25.0 25.0 22.30 5.40 51.5 8.0 170.00 SR M6X25 DIN912 HW 5.0
• Clamping torque for FSHDR..-6: 7.5 Nxm, for FSHDR..-8: 10 Nxm
(1) Cutting depth maximum
For inserts, see pages: FSPA/FSMA (449)
Insert Clamping Instructions
1
Locating / gripping surfaces
2
1 Position the insert in the pocket so Warning
the notch on the insert sits on top of • Do not apply any force and do not hold the
the frontal bulge of the pocket insert in place while closing the screw.
2 Close the clamping screw 1 2 • There is no contact between the
insert and pocket rear wall 2
±0.025
FSPA/FSMA S1
Full Radius Precision Inserts AN
for Machining Aluminum at YZ lNSL
Medium to High Feeds
CW
RE BW
Recommended
Dimensions Tough 1 Hard
Machining Data
ap f turn
IC20
IC07
ID5
Designation CW CWTOL(2) RE S1 BW INSL AN (mm) (mm/rev)
FSPA 6.00-3.00 6.00 0.02 3.00 7.50 4.60 25.00 9.0 • 0.05-3.00 0.30-0.55
FSPA 6.00-3.00YZ 6.00 0.02 3.00 7.50 4.60 25.00 9.0 • 0.05-3.00 0.30-0.55
FSPA 6.00-3.00YZ-D 6.00 0.02 3.00 7.50 4.60 25.00 9.0 • 0.05-3.00 0.30-0.55
FSPA 80-40 8.00 0.02 4.00 8.40 5.60 29.70 10.0 • 0.05-4.00 0.40-0.72
FSPA 80-40-D 8.00 0.02 4.00 8.40 5.60 29.70 10.0 • 0.05-4.00 0.40-0.72
FSPA 80-40YZ 8.00 0.02 4.00 8.40 5.60 29.70 10.0 • 0.05-4.00 0.40-0.72
FSPA 80-40YZ-D 8.00 0.02 4.00 8.40 5.60 29.70 10.0 • 0.05-4.00 0.40-0.72
FSMA 80-40 (1) 8.00 0.04 4.00 8.40 5.60 29.70 10.0 • 0.05-4.00 0.40-0.72
(1) Utility insert
(2) Cutting width tolerance (+/-)
For tools, see pages: DTF50 FSHDR-8 (451) • DTF50 FSHIUR (451) • FSHDR (449) • FSHIUR (448)
449