Каталог Iscar обработка канавок 2022 - страница 177
Навигация
 Каталог Iscar монолитные концевые фрезы и система multi-master
 Фрезерные инструменты Iscar 2026
 Каталог Iscar сверла ружейные и для глубокого сверления 2022
 Каталог Iscar токарные державки ISO 2022
 Каталог Iscar инструмент для обработки алюминиевых колёс
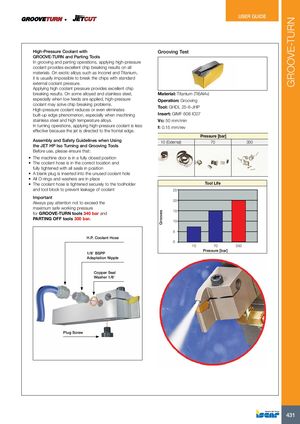
High-Pressure Coolant with Grooving Test
GROOVE-TURN and Parting Tools In grooving and parting operations, applying high-pressure coolant provides excellent chip breaking results on all materials. On exotic alloys such as Inconel and Titanium,
it is usually impossible to break the chips with standard external coolant pressure. Applying high coolant pressure provides excellent chip
| breaking results. On some alloyed and stainless steel, | Material: Titanium (Ti6Al4v) |
| especially when low feeds are applied, high-pressure | Operation: Grooving |
| coolant may solve chip breaking problems. | |
| Tool: GHDL 25-6-JHP | |
| High-pressure coolant reduces or even eliminates | |
| built-up edge phenomenon, especially when machining | Insert: GIMF 608 IC07 |
| stainless steel and high temperature alloys. | Vc: 50 mm/min |
| In turning operations, applying high-pressure coolant is less | f: 0.15 mm/rev |
| effective because the jet is directed to the frontal edge. | |
| Pressure [bar] | |
| Assembly and Safety Guidelines when Using | 350 70 10 (External) |
the JET HP Iso Turning and Grooving Tools Before use, please ensure that:
- The machine door is in a fully closed position
- The coolant hose is in the correct location and fully tightened with all seals in position
- A blank plug is inserted into the unused coolant hole
- All O-rings and washers are in place
- The coolant hose is tightened securely to the toolholder Tool Life and tool block to prevent leakage of coolant 25 Important Always pay attention not to exceed the 20 maximum safe working pressure for GROOVE-TURN tools 340 bar and 15 PARTING OFF tools 300 bar.
10 5 H.P. Coolant Hose 0
10 70 350
Pressure [bar] 1/8” BSPP Adaptation Nipple
Copper Seal Washer 1/8”
Plug Screw