Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 42
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
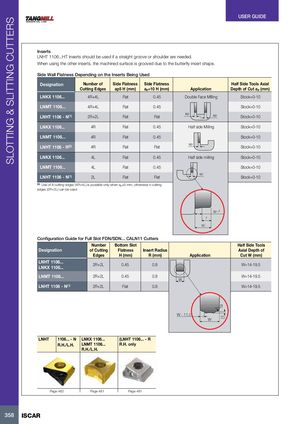
Inserts LNHT 1106...HT inserts should be used if a straight groove or shoulder are needed. When using the other inserts, the machined surface is grooved due to the butterfly insert shape. Side Wall Flatness Depending on the Inserts Being Used
| Designation | Number of Cutting Edges | Side Flatness ap5 H (mm) | Side Flatness ap=10 H (mm) | Application | Half Side Tools Axial Depth of Cut ap (mm) |
| LNKX 1106... | 4R+4L | Flat | 0.45 | Double Face MIlling | Stock=0-10 |
| LNMT 1106... | 4R+4L | Flat | 0.45 | Stock=0-10 | |
| LNHT 1106 - N(1) | 2R+2L | Flat | Flat | ap ap | Stock=0-10 |
| LNKX 1106... | 4R | Flat | 0.45 | Half side Milling | Stock=0-10 |
| LNMT 1106... | 4R | Flat | 0.45 | Stock=0-10 | |
| LNHT 1106 - R(2) | 4R | Flat | Flat | ap | Stock=0-10 |
| LNKX 1106... | 4L | Flat | 0.45 | Half side milling | Stock=0-10 |
| LNMT 1106... | 4L | Flat | 0.45 | Stock=0-10 | |
| LNHT 1106 - N(1) | 2L | Flat | Flat | ap | Stock=0-10 |
| )Use of 8 cutting edges (4 dges (2R+2L) can be used Configuration Guide | R+4L) is possible only for Full Slot FDN | when ap≤5 mm, othe /SDN... CALN1 | rwise 4 cutting 1 Cutters | ap 7 ap-7 | |
| Designation | Number of Cutting Edges | Bottom Slot Flatness H (mm) | Insert Radius R (mm) | Application | Half Side Tools Axial Depth of Cut W (mm) |
| LNHT 1106... LNKX 1106... | 2R+2L | 0.45 | 0.8 | W=14-19.5 | |
| LNMT 1106... | 2R+2L | 0.45 | 0.8 | W | W=14-19.5 |
| LNHT 1106 - N(1) | 2R+2L | Flat | 0.8 | W=14-19.5 | |
| W WÊ-Ê11.0 R H |
| LNHT | 1106... - N | LNKX 1106... | (LNHT 1106... - R |
| R.H./L.H. | LNMT 1106... | R.H. only |
R.H./L.H.
Page 482 Page 481 Page 481