Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 221
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
W1 S
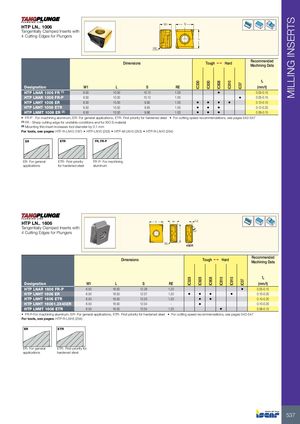
HTP LN.. 1006
Tangentially Clamped Inserts with
4 Cutting Edges for Plungers
L
RE
Recommended
Dimensions Tough 1 Hard
Machining Data
fz
IC330
IC830
IC808
IC810
IC07
Designation W1 L S RE (mm/t)
HTP LNAR 1006 FR (1) 6.50 10.50 10.13 1.00 • 0.05-0.15
HTP LNAR 1006 FR-P 6.50 10.50 10.13 1.00 • 0.05-0.15
HTP LNHT 1006 ER 6.50 10.50 9.93 1.00 • • • • 0.10-0.15
HTP LNHT 1006 ETR 6.50 10.50 9.93 1.00 • • • 0.12-0.20
HTP LNMT 1006 ER (2) 6.50 10.50 9.96 1.00 • • • 0.08-0.15
• FR-P - For machining aluminum, ER- For general applications, ETR- First priority for hardened steel • For cutting speed recommendations, see pages 542-547
(1) FR - Sharp cutting edge for unstable conditions and for ISO S material
(2) Mounting this insert increases tool diameter by 0.1 mm
For tools, see pages: HTF-R-LN10 (197) • HTP-LN10 (253) • HTP-M-LN10 (253) • HTP-R-LN10 (254)
ER ETR FR, FR-P
ER- For general ETR- First priority FR-P- For machining
applications for hardened steel aluminum
W1 1.2
S
HTP LN.. 1606
Tangentially Clamped Inserts with
45°
4 Cutting Edges for Plungers L
RE
45ER
Recommended
Dimensions Tough 1 Hard
Machining Data
fz
IC328
IC928
IC908
IC810
IC910
IC07
Designation W1 L S RE (mm/t)
HTP LNAR 1606 FR-P 6.50 16.50 12.28 1.20 • 0.05-0.15
HTP LNHT 1606 ER 6.50 16.50 12.07 1.20 • • • • 0.10-0.20
HTP LNHT 1606 ETR 6.50 16.50 12.03 1.20 • • 0.10-0.20
HTP LNHT 16061.2X45ER 6.50 16.50 12.04 - • 0.10-0.20
HTP LNMT 1606 ETR 6.50 16.50 12.04 1.20 • 0.08-0.15
• FR-P-For machining aluminum, ER- For general applications, ETR- First priority for hardened steel • For cutting speed recommendations, see pages 542-547
For tools, see pages: HTP-R-LN16 (254)
ER ETR
ER- For general ETR- First priority for
applications hardened steel
537