Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 213
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
7˚
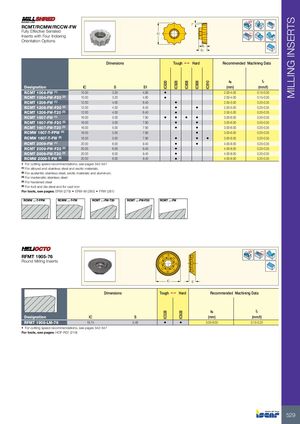
RCMT/RCMW/RCCW-FW
Fully Effective Serrated
IC Rd°
Inserts with Four Indexing
Orientation Options
S
S1
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC830
IC928
IC808
IC908
IC910
Designation IC S S1 (mm) (mm/t)
RCMT 1004-FW (1) 10.00 3.20 4.80 • 2.00-4.00 0.15-0.30
RCMT 1004-FW-F20 (2) 10.00 3.20 4.80 • 2.00-4.00 0.15-0.30
RCMT 1206-FW (1) 12.00 4.00 6.40 • 2.50-5.00 0.20-0.35
RCMT 1206-FW-F20 (2) 12.00 4.00 6.40 • • 2.50-5.00 0.20-0.35
RCMT 1206-FW-T20 (3) 12.00 4.00 6.40 • 2.50-5.00 0.20-0.35
RCMT 1607-FW (1) 16.00 5.00 7.90 • • • • 3.00-6.00 0.20-0.35
RCMT 1607-FW-F20 (2) 16.00 5.00 7.90 • • 3.00-6.00 0.20-0.35
RCMT 1607-FW-T20 (3) 16.00 5.00 7.90 • • 3.00-6.00 0.20-0.35
RCMW 1607-T-FPW (4) 16.00 5.00 7.90 • 3.00-6.00 0.20-0.35
RCMW 1607-T-FW (5) 16.00 5.00 7.90 • • • 3.00-6.00 0.20-0.35
RCMT 2009-FW (1) 20.00 6.00 9.40 • • 4.00-8.00 0.20-0.35
RCMT 2009-FW-F20 (2) 20.00 6.00 9.40 • 4.00-8.00 0.20-0.35
RCMT 2009-FW-T20 (3) 20.00 6.00 9.40 • 4.00-8.00 0.20-0.35
RCMW 2009-T-FW (5) 20.00 6.00 9.40 • 4.00-8.00 0.20-0.35
• For cutting speed recommendations, see pages 542-547
(1) For alloyed and stainless steel and exotic materials.
(2) For austenitic stainless steel, exotic materials and aluminum.
(3) For martensitic stainless steel
(4) For hardened steel
(5) For tool and die steel and for cast iron
For tools, see pages: ERW (279) • ERW-M (280) • FRW (281)
RCMW ...-T-FPW RCMW ...-T-FW RCMT ...-FW-T20 RCMT ...-FW-F20 RCMT ...-FW
Rd°
RFMT 1905-76
4
3
5
Round Milling Inserts 2
6
1
7
8
IC S
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC328
IC928
Designation IC S (mm) (mm/t)
RFMT 1905-LM-76 19.74 5.48 • • 3.00-8.00 0.15-0.25
• For cutting speed recommendations, see pages 542-547
For tools, see pages: HOF-R07 (219)
529