Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 205
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
RE ...CS
S1
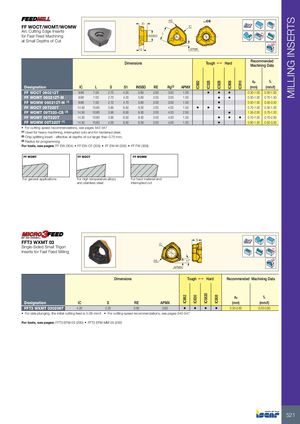
FF WOCT/WOMT/WOMW IC
Arc Cutting Edge Inserts L Rd°
for Fast Feed Machining INSBD
at Small Depths of Cut
S APMX
Recommended
Dimensions Tough 1 Hard
Machining Data
ap fz
IC882
IC328
IC928
IC908
IC910
Designation IC L S S1 INSBD RE Rg(3) APMX (mm) (mm/t)
FF WOCT 060212T 9.86 7.00 2.70 4.20 5.60 2.00 3.00 1.00 • • • 0.30-1.00 0.30-1.00
FF WOMT 060212T-M 9.86 7.00 2.70 4.20 5.60 2.00 3.00 1.00 • • 0.30-1.00 0.70-1.50
FF WOMW 060212T-M (1) 9.86 7.00 2.70 4.70 5.60 2.00 3.00 1.00 • 0.50-1.00 0.50-3.50
FF WOCT 09T320T 14.50 10.60 3.95 6.50 9.30 2.00 4.00 1.50 • • • 0.70-1.50 0.30-1.00
FF WOMT 09T320-CS (2) 14.50 10.60 3.95 6.50 9.30 2.00 4.20 2.00 • 1.50-2.00 0.70-1.20
FF WOMT 09T320T 14.50 10.60 3.95 6.50 9.30 2.00 4.00 1.50 • • • 0.70-1.50 0.70-2.00
FF WOMW 09T320T (1) 14.50 10.60 4.00 6.50 9.30 2.00 4.00 1.50 • 0.80-1.50 0.50-3.50
• For cutting speed recommendations, see pages 542-547
(1) Used for heavy machining, interrupted cuts and for hardened steel.
(2) Chip splitting insert - effective at depths of cut larger than 0.75 mm.
(3) Radius for programming
For tools, see pages: FF EW (304) • FF EW-CF (305) • FF EW-M (305) • FF FW (309)
FF WOMT FF WOCT FF WOMW
For general applications For high temperature alloys For hard material and
and stainless steel interrupted cut
S
FFT3 WXMT 03 IC
Single-Sided Small Trigon Rd°
Inserts for Fast Feed Milling
RE 17˚
APMX
Dimensions Tough 1 Hard Recommended Machining Data
IC5820
ap fz
IC882
IC830
IC808
Designation IC S RE APMX (mm) (mm/t)
FFT3 WXMT 030206T 4.20 2.20 0.60 0.60 • • • • 0.20-0.60 0.20-0.80
• For side plunging, the initial cutting feed is 0.08 mm/t • For cutting speed recommendations, see pages 542-547
For tools, see pages: FFT3 EFM-03 (293) • FFT3 EFM-MM 03 (293)
521