Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 197
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
L
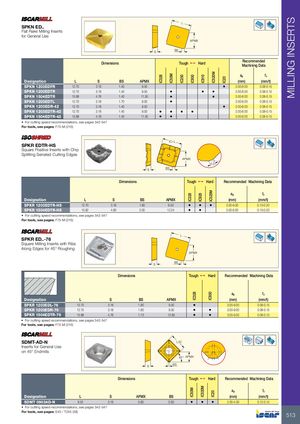
SPKN ED..
Flat Rake Milling Inserts
for General Use
APMX
BS
S
Recommended
Dimensions Tough 1 Hard
Machining Data
IC520M
ap fz
IC50M
IC328
IC250
IC950
IC910
IC20
Designation L S BS APMX (mm) (mm/t)
SPKN 1203EDFR 12.70 3.18 1.40 9.50 • 3.00-8.00 0.08-0.15
SPKN 1203EDTR 12.70 3.18 1.40 9.50 • • • 3.00-8.00 0.08-0.15
SPKN 1504EDTR 15.88 4.76 1.40 11.50 • • 3.00-8.00 0.08-0.15
SPKN 1203EDTL 12.70 3.18 1.70 9.50 • 3.00-8.00 0.08-0.15
SPKN 1203EDR-42 12.70 3.18 1.40 9.50 • 3.00-8.00 0.08-0.15
SPKN 1203EDTR-42 12.70 3.18 1.40 9.50 • • • • 3.00-8.00 0.08-0.15
SPKN 1504EDTR-42 15.88 4.76 1.40 11.50 • • 3.00-8.00 0.08-0.15
• For cutting speed recommendations, see pages 542-547
For tools, see pages: F75-M (216)
IC=L
SPKR EDTR-HS
Square Positive Inserts with Chip
Splitting Serrated Cutting Edges
APMX
0.5
S BS
Dimensions Tough 1 Hard Recommended Machining Data
IC520M
ap fz
IC328
Designation L S BS APMX IC928 (mm) (mm/t)
SPKR 1203EDTR-HS 12.70 3.18 1.60 9.50 • • • 3.00-9.00 0.10-0.20
SPKR 1504EDTR-HS 15.82 4.80 2.00 12.24 • • 3.00-9.00 0.10-0.20
• For cutting speed recommendations, see pages 542-547
For tools, see pages: F75-M (216)
L
SPKR ED..-76
Square Milling Inserts with Ribs
Along Edges for 45° Roughing
APMX
BS
S
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC328
IC950
Designation L S BS APMX (mm) (mm/t)
SPKR 1203EDL-76 12.70 3.18 1.80 9.50 • 3.00-9.00 0.08-0.15
SPKR 1203EDR-76 12.70 3.18 1.80 9.50 • • 3.00-9.00 0.08-0.15
SPKR 1504EDTR-76 15.88 4.76 1.73 12.65 • • 3.00-9.00 0.08-0.15
• For cutting speed recommendations, see pages 542-547
For tools, see pages: F75-M (216)
SDMT-AD-N L/IC
Inserts for General Use
on 45° Endmills
45° APMX
BS
S
Dimensions Tough 1 Hard Recommended Machining Data
IC520M
IC50M
ap fz
IC20
Designation L S APMX BS (mm) (mm/t)
SDMT 0903AD-N 9.52 3.18 5.60 0.90 • • • 2.00-4.00 0.12-0.15
• For cutting speed recommendations, see pages 542-547
For tools, see pages: E45 / T245 (38)
513
L
SPKN ED..
Flat Rake Milling Inserts
for General Use
APMX
BS
S
Recommended
Dimensions Tough 1 Hard
Machining Data
IC520M
ap fz
IC50M
IC328
IC250
IC950
IC910
IC20
Designation L S BS APMX (mm) (mm/t)
SPKN 1203EDFR 12.70 3.18 1.40 9.50 • 3.00-8.00 0.08-0.15
SPKN 1203EDTR 12.70 3.18 1.40 9.50 • • • 3.00-8.00 0.08-0.15
SPKN 1504EDTR 15.88 4.76 1.40 11.50 • • 3.00-8.00 0.08-0.15
SPKN 1203EDTL 12.70 3.18 1.70 9.50 • 3.00-8.00 0.08-0.15
SPKN 1203EDR-42 12.70 3.18 1.40 9.50 • 3.00-8.00 0.08-0.15
SPKN 1203EDTR-42 12.70 3.18 1.40 9.50 • • • • 3.00-8.00 0.08-0.15
SPKN 1504EDTR-42 15.88 4.76 1.40 11.50 • • 3.00-8.00 0.08-0.15
• For cutting speed recommendations, see pages 542-547
For tools, see pages: F75-M (216)
IC=L
SPKR EDTR-HS
Square Positive Inserts with Chip
Splitting Serrated Cutting Edges
APMX
0.5
S BS
Dimensions Tough 1 Hard Recommended Machining Data
IC520M
ap fz
IC328
Designation L S BS APMX IC928 (mm) (mm/t)
SPKR 1203EDTR-HS 12.70 3.18 1.60 9.50 • • • 3.00-9.00 0.10-0.20
SPKR 1504EDTR-HS 15.82 4.80 2.00 12.24 • • 3.00-9.00 0.10-0.20
• For cutting speed recommendations, see pages 542-547
For tools, see pages: F75-M (216)
L
SPKR ED..-76
Square Milling Inserts with Ribs
Along Edges for 45° Roughing
APMX
BS
S
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC328
IC950
Designation L S BS APMX (mm) (mm/t)
SPKR 1203EDL-76 12.70 3.18 1.80 9.50 • 3.00-9.00 0.08-0.15
SPKR 1203EDR-76 12.70 3.18 1.80 9.50 • • 3.00-9.00 0.08-0.15
SPKR 1504EDTR-76 15.88 4.76 1.73 12.65 • • 3.00-9.00 0.08-0.15
• For cutting speed recommendations, see pages 542-547
For tools, see pages: F75-M (216)
SDMT-AD-N L/IC
Inserts for General Use
on 45° Endmills
45° APMX
BS
S
Dimensions Tough 1 Hard Recommended Machining Data
IC520M
IC50M
ap fz
IC20
Designation L S APMX BS (mm) (mm/t)
SDMT 0903AD-N 9.52 3.18 5.60 0.90 • • • 2.00-4.00 0.12-0.15
• For cutting speed recommendations, see pages 542-547
For tools, see pages: E45 / T245 (38)
513