Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 196
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
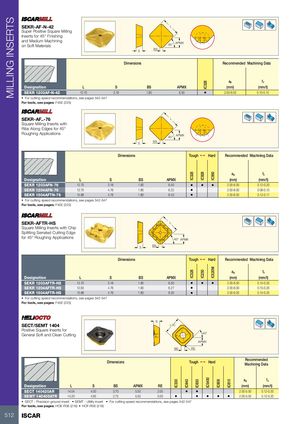
SEKR-AF-N-42 L
Super Positive Square Milling
Inserts for 45° Finishing
and Medium Machining APMX
45°
on Soft Materials
BS
S
Dimensions Recommended Machining Data
ap fz
IC328
Designation L S BS APMX (mm) (mm/t)
SEKR 1203AF-N-42 12.70 3.18 1.80 6.50 • 2.00-6.00 0.10-0.15
• For cutting speed recommendations, see pages 542-547
For tools, see pages: F45E (225)
SEKR-AF..-76 L
Square Milling Inserts with
Ribs Along Edges for 45°
Roughing Applications APMX
45°
BS
S
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC328
IC928
IC950
Designation L S BS APMX (mm) (mm/t)
SEKR 1203AFN-76 12.70 3.18 1.80 6.50 • • • 2.00-6.00 0.12-0.20
SEKR 1204AFN-76 12.70 4.76 1.80 6.22 • 2.00-6.00 0.08-0.15
SEKR 1504AFTN-76 15.88 4.76 1.80 8.43 • 2.00-6.00 0.12-0.17
• For cutting speed recommendations, see pages 542-547
For tools, see pages: F45E (225)
SEKR-AFTR-HS L
Square Milling Inserts with Chip
Splitting Serrated Cutting Edge
for 45° Roughing Applications 45° APMX
BS
S
Dimensions Tough 1 Hard Recommended Machining Data
IC520M
ap fz
IC328
IC250
Designation L S BS APMX (mm) (mm/t)
SEKR 1203AFTR-HS 12.70 3.18 1.80 6.50 • • • 2.00-6.00 0.15-0.25
SEKR 1204AFTR-HS 12.63 4.76 1.80 6.27 • 2.00-6.00 0.15-0.25
SEKR 1504AFTR-HS 15.88 4.76 1.80 8.30 • 2.00-6.00 0.15-0.25
• For cutting speed recommendations, see pages 542-547
For tools, see pages: F45E (225)
S
SECT/SEMT 1404 L/IC
Positive Square Inserts for
45°
General Soft and Clean Cutting
APMX
BS RE
Recommended
Dimensions Tough 1 Hard
Machining Data
ap fz
IC5400
IC330
IC840
IC830
IC808
IC810
Designation L S BS APMX RE (mm) (mm/t)
SECT 140420AR 14.04 4.50 3.70 5.50 2.00 • • 2.00-5.50 0.12-0.20
SEMT 140405ATR 14.20 4.95 2.75 5.50 0.50 • • • • • 2.00-5.50 0.12-0.20
• SECT - Precision ground insert • SEMT - Utility insert • For cutting speed recommendations, see pages 542-547
For tools, see pages: HOE-R06 (218) • HOF-R06 (218)
512 ISCAR