Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 187
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
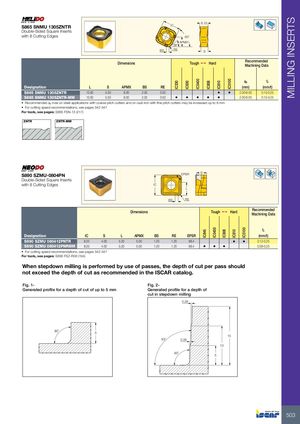
S865 SNMU 1305ZNTR IC
Double-Sided Square Inserts
with 8 Cutting Edges 65° APMX 38° BS RE S
Recommended
Dimensions Tough 1 Hard Machining Data
a f
p z
| Designation | L | S | APMX | BS | RE | (mm) | (mm/t) | ||||||
| S865 SNMU 1305ZNTR | 13.00 | 5.50 | 8.00 | 2.00 | 0.50 | • | • | 2.00-6.00 | 0.15-0.25 | ||||
| S865 SNMU 1305ZNTR-MM | 13.00 | 5.50 | 8.00 | 2.00 | 0.50 | • | • | • | • | • | 2.00-6.00 | 0.15-0.25 |
- Recommended a max on steel applications with coarse pitch cutters and on cast iron with fine pitch cutters may be increased up to 8 mm
p
- For cutting speed recommendations, see pages 542-547
For tools, see pages: S865 FSN-13 (217) ZNTR ZNTR-MM
S890 SZMU-0804PN EPSR S
Double-Sided Square Inserts with 8 Cutting Edges IC L BS RE
Recommended
Dimensions Tough 1 Hard Machining Data
f
z
| Designation | IC | S | L | APMX | BS | RE | EPSR | (mm/t) | |||||
| S890 SZMU 080412PNTR | 8.20 | 4.00 | 5.20 | 5.00 | 1.20 | 1.20 | 88.4 | • | • | 0.12-0.25 | |||
| S890 SZMU 080412PNRMM | 8.20 | 4.00 | 5.20 | 5.00 | 1.20 | 1.20 | 88.4 | • | • | • | 0.08-0.25 |
- For cutting speed recommendations, see pages 542-547
For tools, see pages: S890 FSZ-R08 (194)
When stepdown milling is performed by use of passes, the depth of cut per pass should
not exceed the depth of cut as recommended in the ISCAR catalog.
Fig. 1- Fig. 2-
Generated profile for a depth of cut of up to 5 mm Generated profile for a depth of
cut in stepdown milling
0.28
90˚ 5
93˚
0.28
90˚
15 10 5